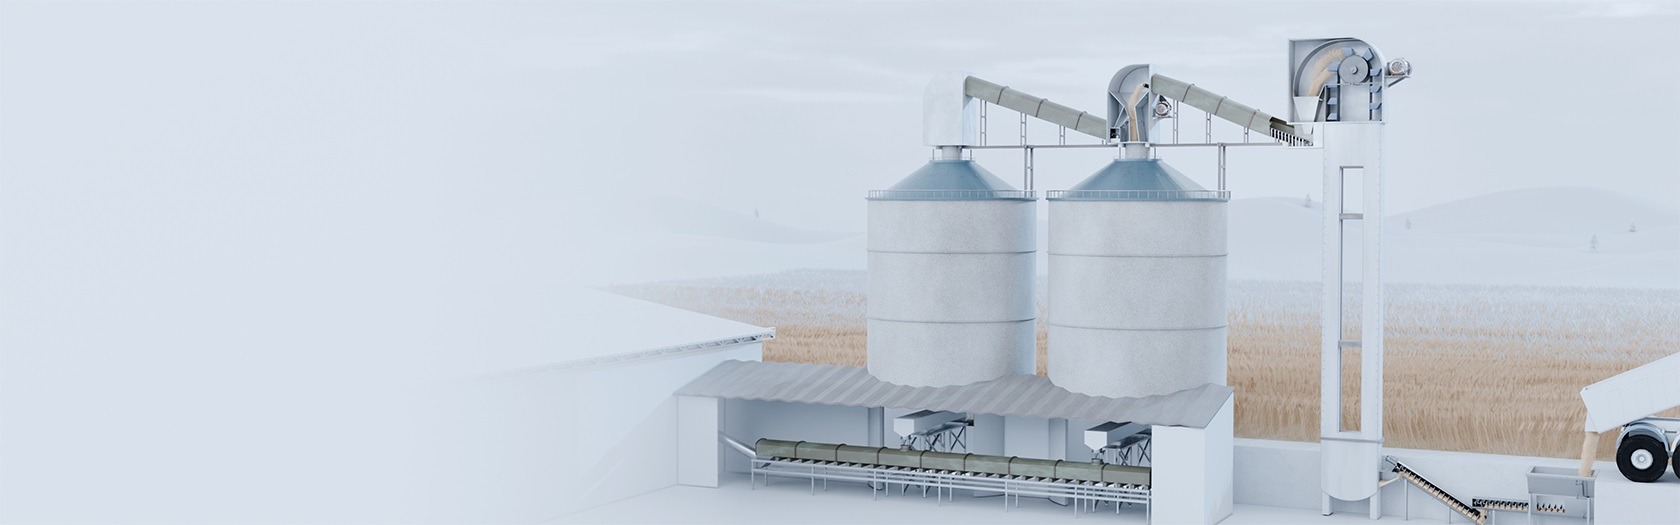
Solid Material Inventory Management with Mechanical Conveying
Precision for reliability, efficiency and complete traceability
From material unloading to transfer and storage, modern mechanical conveyor systems rely on smart sensor technologies. These technologies guarantee that every gram is measured, monitored and dosed with precision. Designed for the robustness needed to cope with dust, vibration and explosive atmospheres, the sensors enable uninterrupted, safe operation. At the same time, precision and speed guarantee efficiency across the value chain through minimum product loss, improved inventory control and complete traceability.
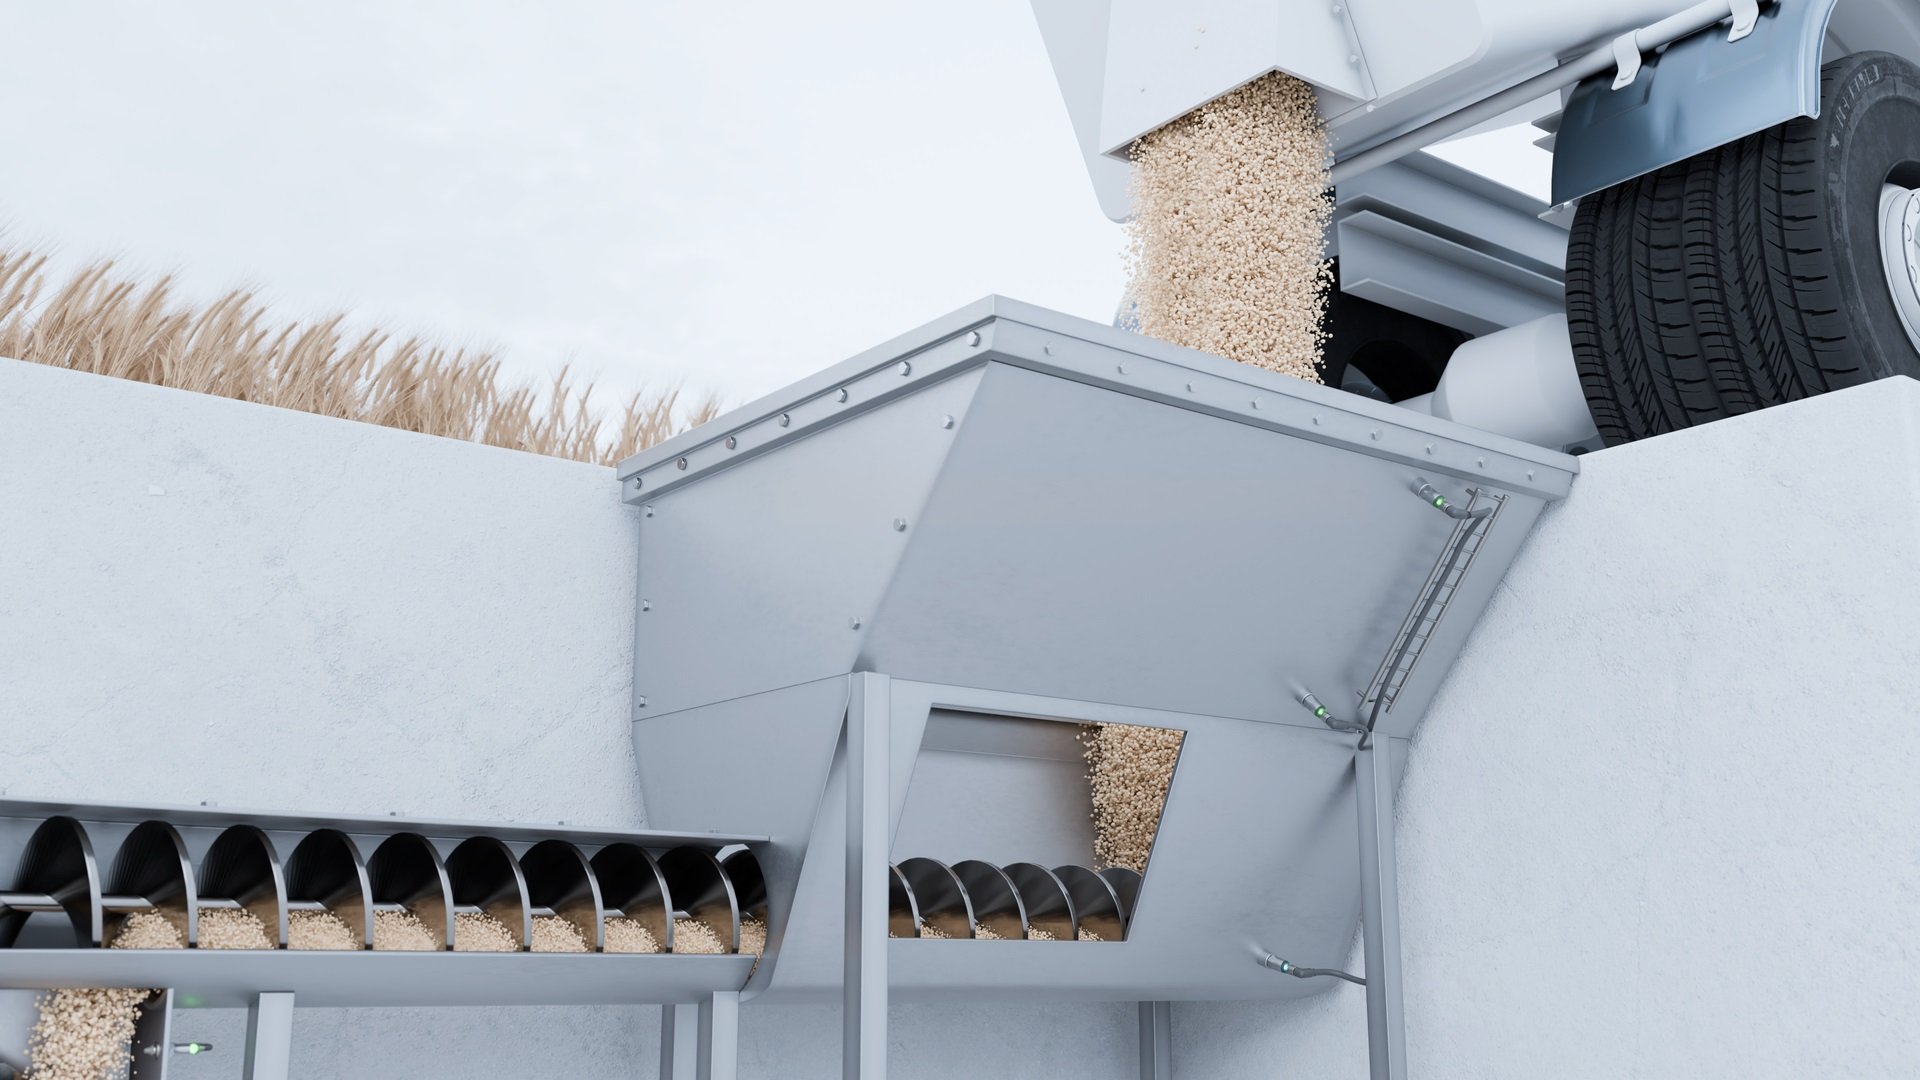
Receival chute monitoring
Ensure reliable fill monitoring and transfer from the receival chute.
- Detection of different fill levels in the receival chute with point level or distance measurement sensors, to start material transfer when the hopper is empty and to prevent no-load running
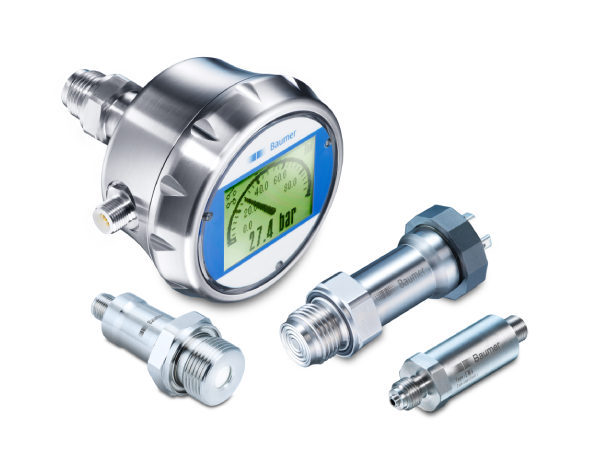
- If delivery trucks lack a bed-lifting function, discharge can be performed with a tipping truck unloader whose hydraulics are monitored by pressure sensors
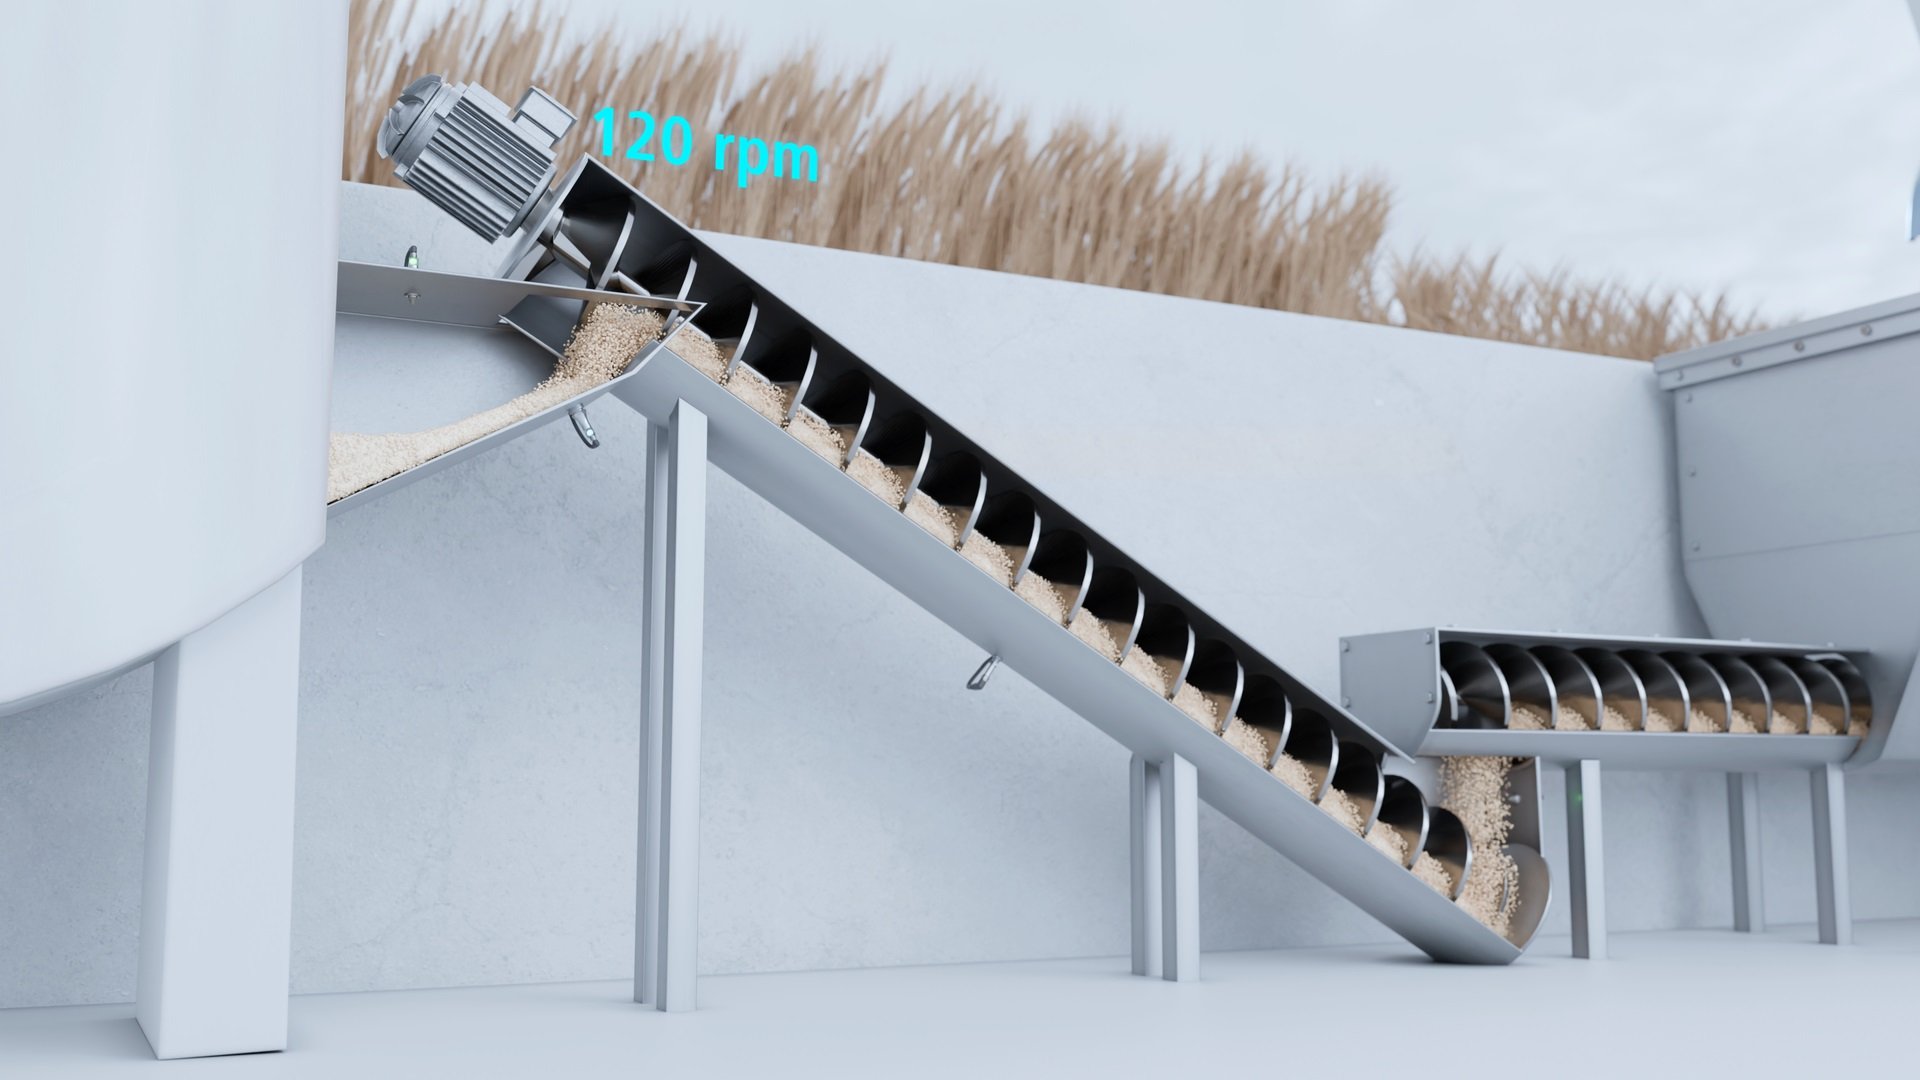
Screw conveyor monitoring
Guarantee reliable, loss-free transport using a rotating helical screw inside a tube.
- Control of screw speed with encoders to ensure consistent and accurate conveying rates suited to upstream and downstream processes
- Detection of blockages in product feeding and discharge, and complete emptying of the screw conveyor, with point level sensors
- Measurement of product temperature with temperature sensors to control heat input or removal in heated or cooled screw conveyors
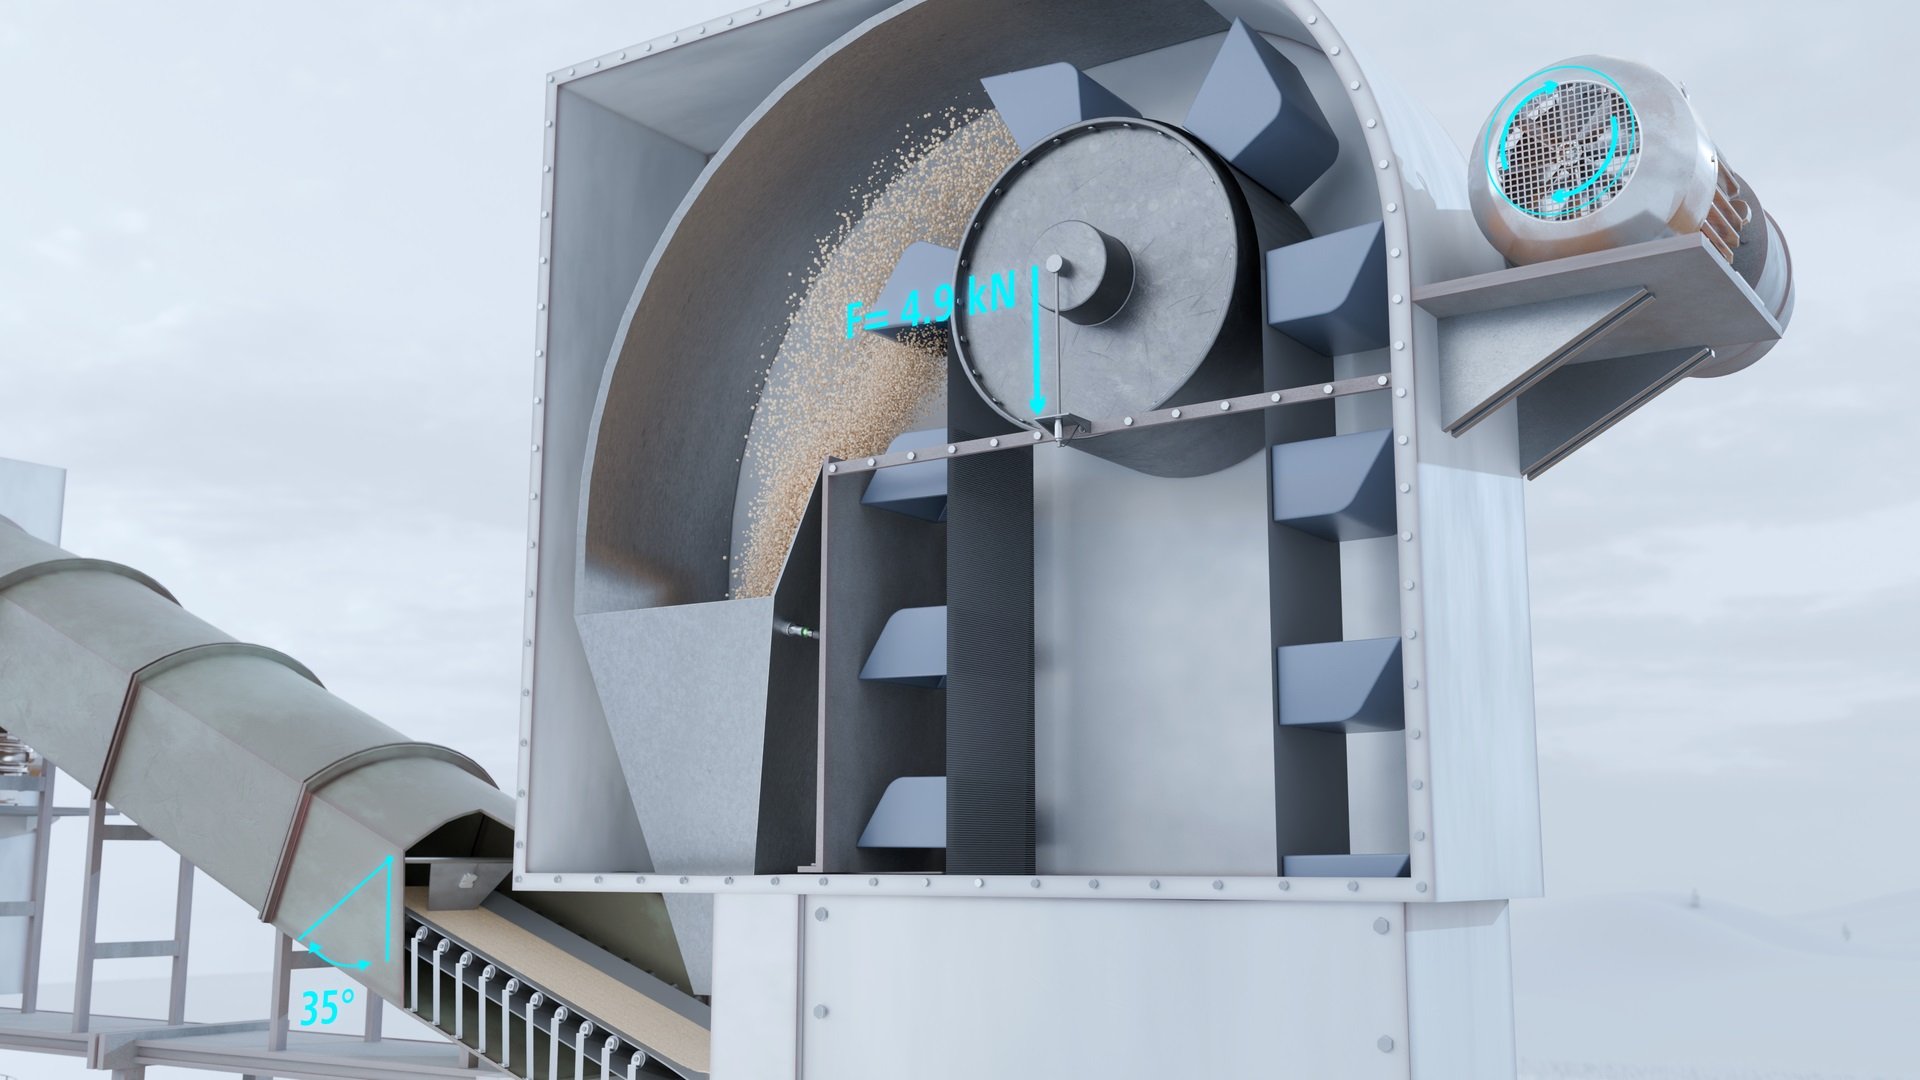
Bucket conveyor monitoring
Guarantee reliable, loss-free vertical transfer of materials in buckets fixed to a belt.
- Control of belt speed with encoders or inductive sensors to ensure consistent and accurate conveying rates suited to upstream and downstream processes; belt slip can also be detected at these measurement points
- Detection of blockages in feeding and product discharge with point level sensors
- Monitoring of belt tension and alignment with force and distance measurement sensors to prevent belt slip or excessive wear
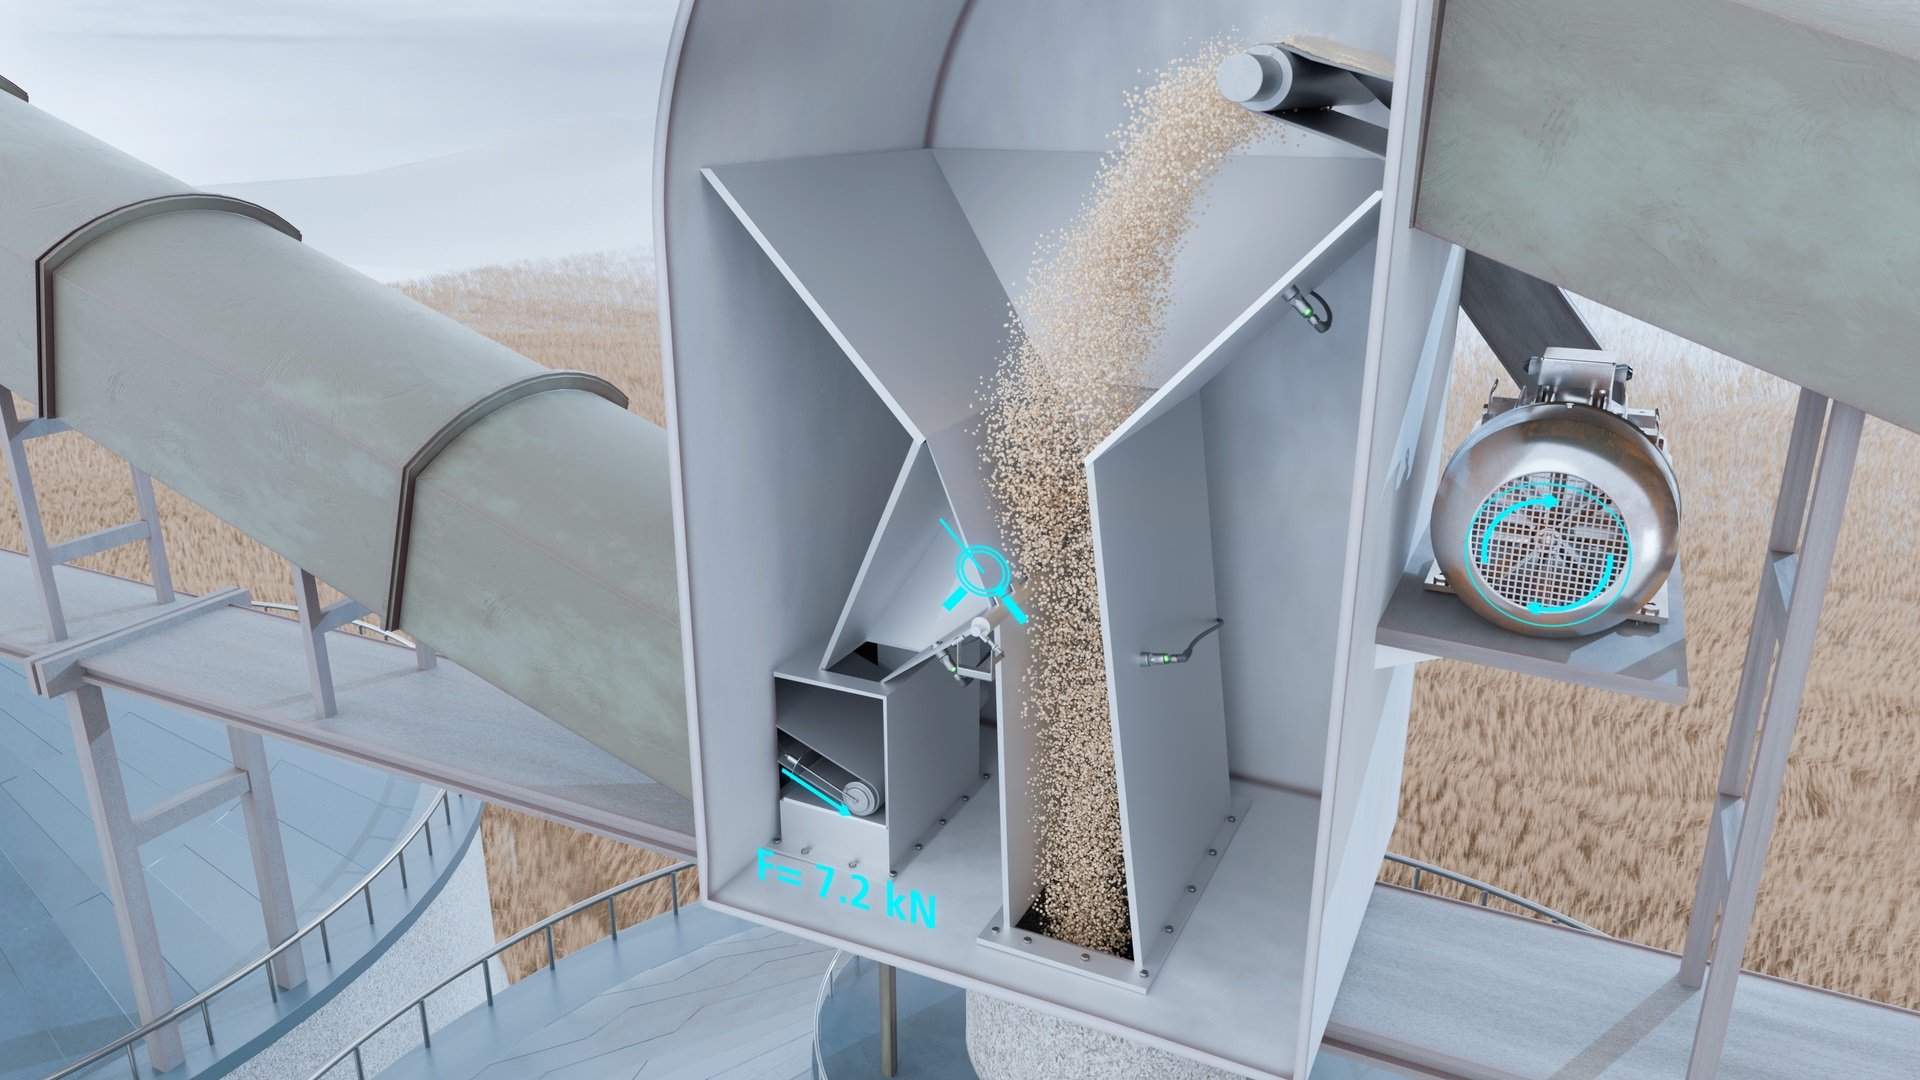
Belt and chain conveyor monitoring
Guarantee reliable, loss-free transport of material on a moving belt running around two or more pulleys, or via flights fixed to a chain.
- Control of speed with encoders or inductive sensors to ensure consistent and accurate conveying rates suited to upstream and downstream processes; belt slip can also be detected at these measurement points
- Detection of blockages in feeding and product discharge with point level sensors
- Monitoring of belt or chain tension and alignment with force and distance measurement sensors to prevent belt slip or wear
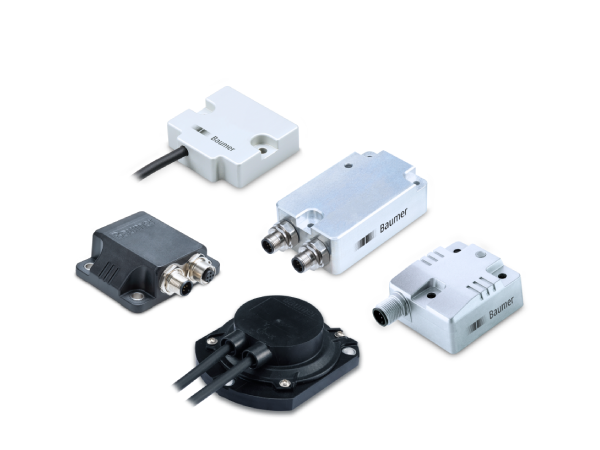
- Measurement of belt load with inclination sensors mounted on a plate placed on top of the product
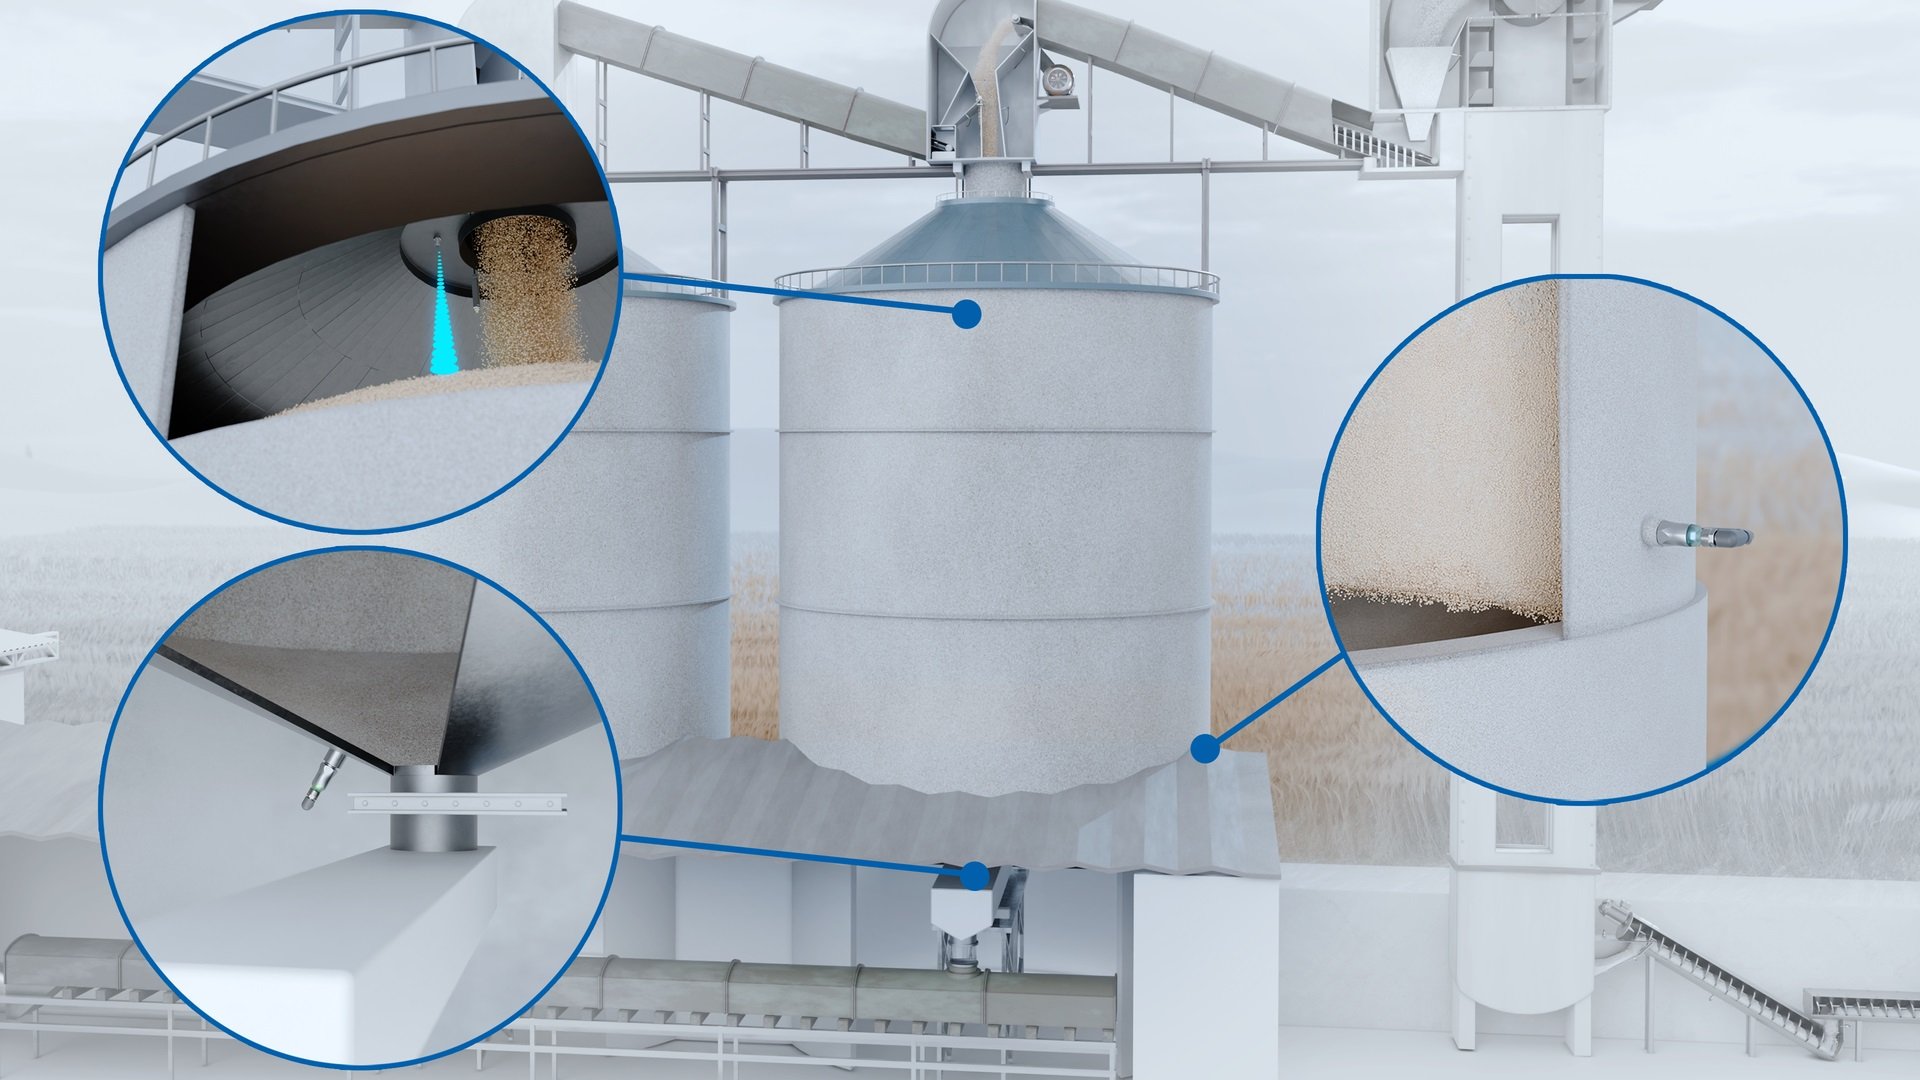
Buffer and storage silo monitoring
Ensure the safe filling and complete emptying of silos, obtain reliable information on fill status, and detect dust explosions instantly.
Certifications and Approvals
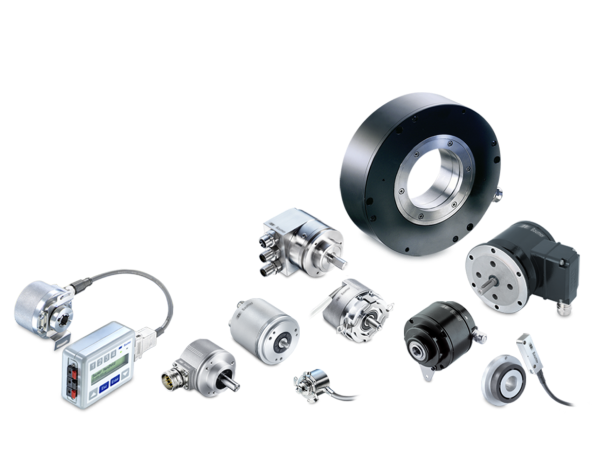
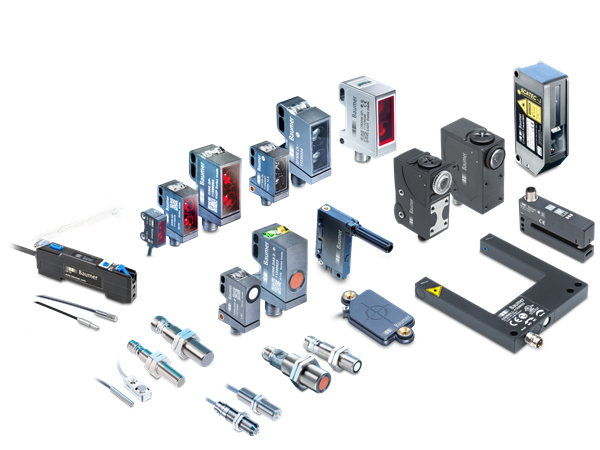
Baumer sensors are certified in accordance with all international design and material standards relevant to the food and beverage industry. Baumer's internal processes are certified according to DIN ISO 9000 requirements. Hygienic sensors are designed, developed and manufactured in compliance with 3-A and EHEDG guidelines to guarantee the highest standards in food production.
An end-to-end development process, from the initial concept stage through to series production, is continuously validated by our customers' use. Our sensors comply with IP69 protection and undergo additional testing under our corporate proTect+ standard for maximum reliability and durability.
Have a Sector-Specific Question?
Our expert engineers are ready to help you identify the most suitable solution for your industry.