Solid Material Inventory Management with Pneumatic Conveying
Precision for reliability, efficiency and complete traceability
From receival to transfer and storage, modern pneumatic conveying systems rely on smart sensor technologies. These technologies guarantee that every gram is measured, monitored and dosed with precision. Designed for the robustness needed to cope with dust, vibration, fast-moving materials and explosive atmospheres, the sensors enable uninterrupted, safe operation. At the same time, precision and speed guarantee efficiency across the value chain through minimum product loss, improved inventory control and complete traceability.
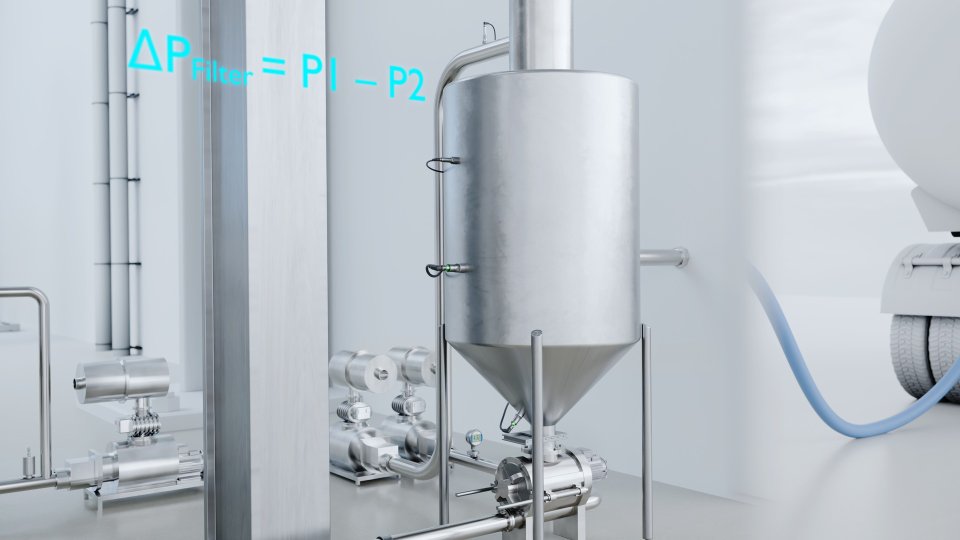
Vacuum conveying systems
Ensure stable material transfer via suction and prevent dust formation by monitoring vacuum conditions and level at the receiving end.
- Control of negative pressure in the collection vessel with pressure sensors to facilitate effective suction of the material
- Monitoring of the differential pressure between the collection vessel and the vacuum pump to detect filter blockages
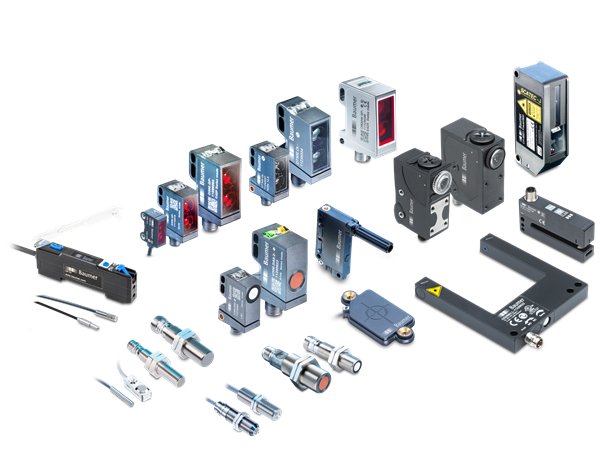
- Detection of high and low fill levels in the collection vessel with point level sensors to prevent overfilling or no-load running
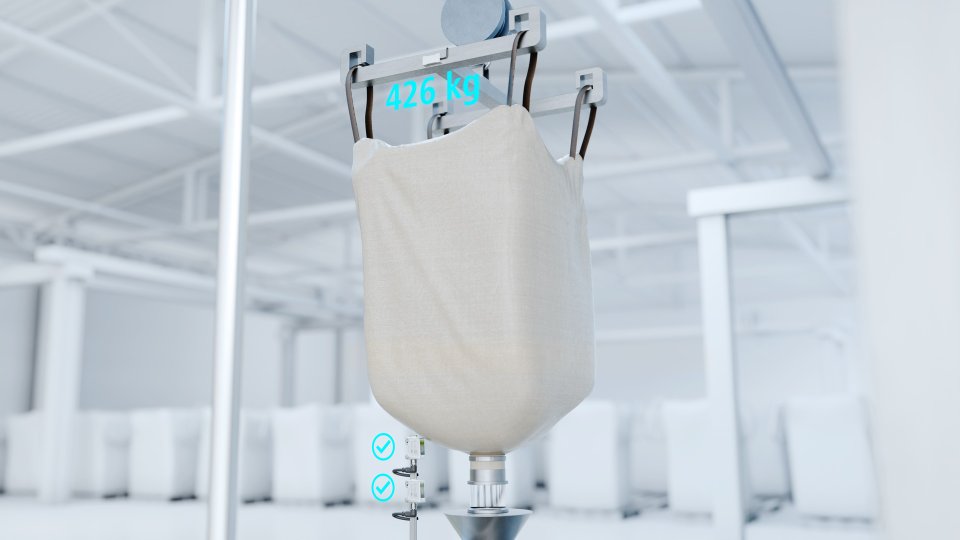
Big bag tipping
Guarantee uninterrupted material continuity and complete traceability.
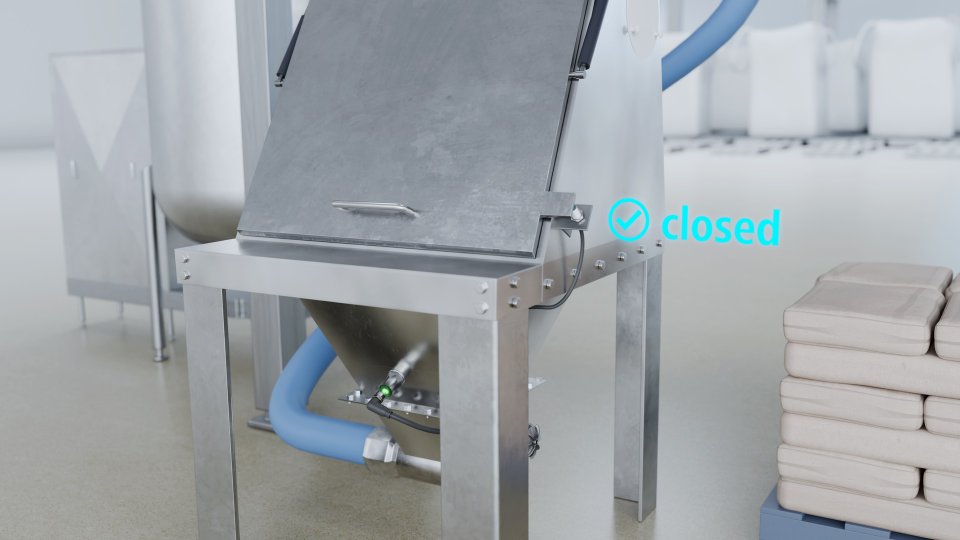
Bag dump station
Enable lump breaking and material transfer while also guaranteeing operator health and safety.
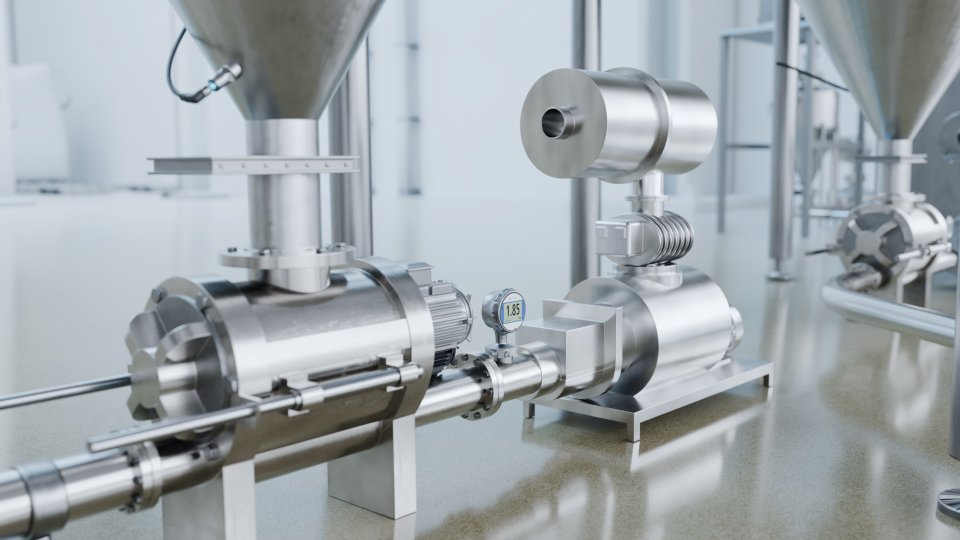
Positive pressure dilute phase conveying systems
Guarantee uninterrupted material transfer using compressed air at sufficient positive pressure as the conveying medium.
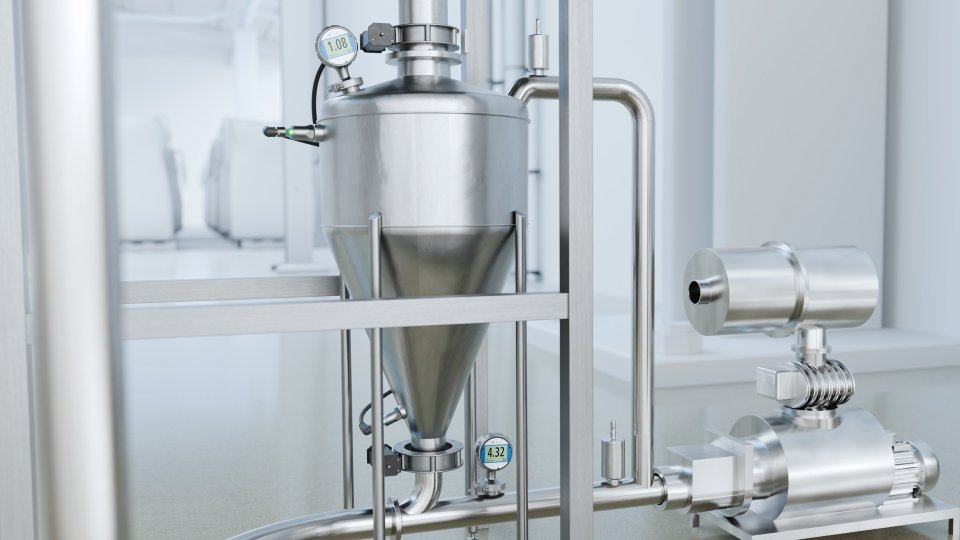
Positive pressure dense phase conveying with pressure vessels
Guarantee gentle, high-capacity material transfer over long distances using high positive pressures.
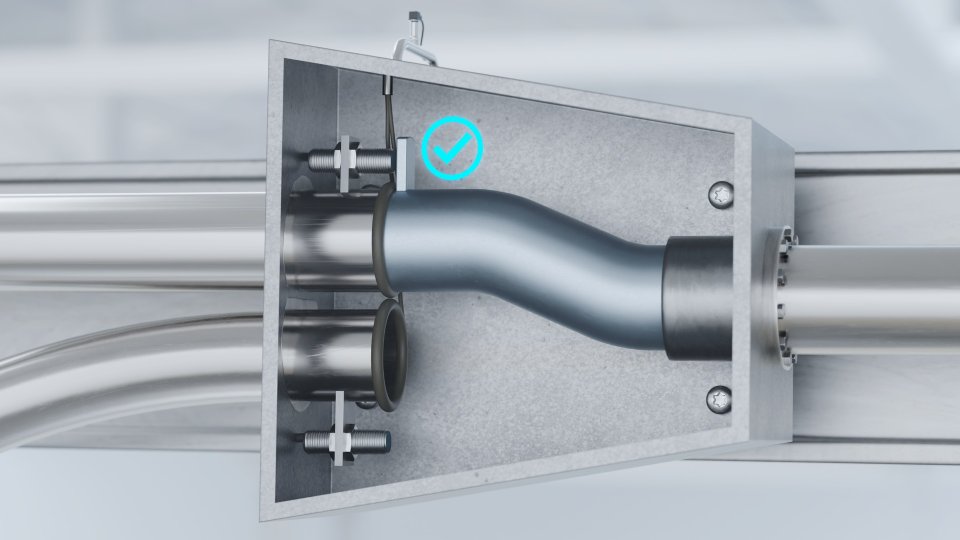
Diverter valve monitoring
Guarantee flexible routing and accurate distribution of conveyed materials with minimum pipeline and product loss.
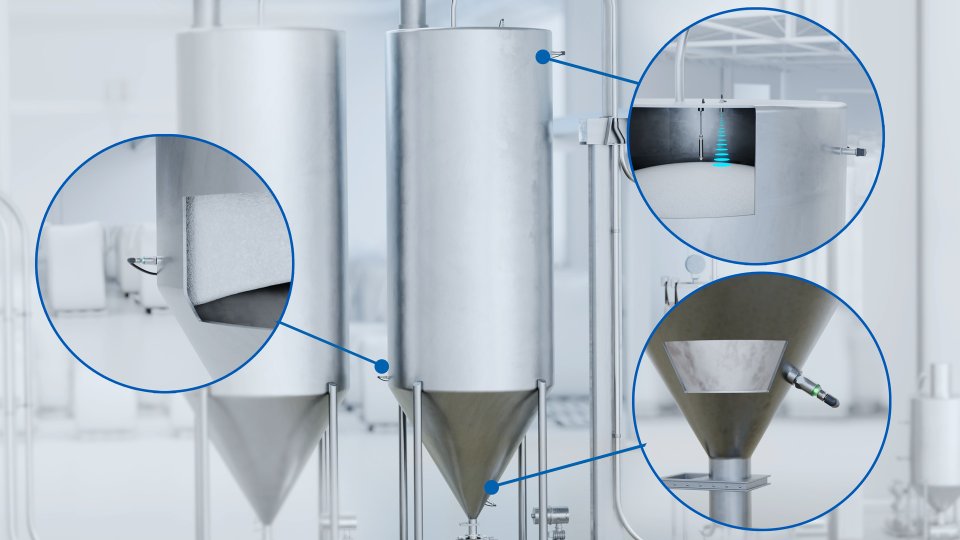
Buffer and storage silo monitoring
Ensure the safe filling and complete emptying of silos, obtain reliable information on fill status, and detect dust explosions instantly.
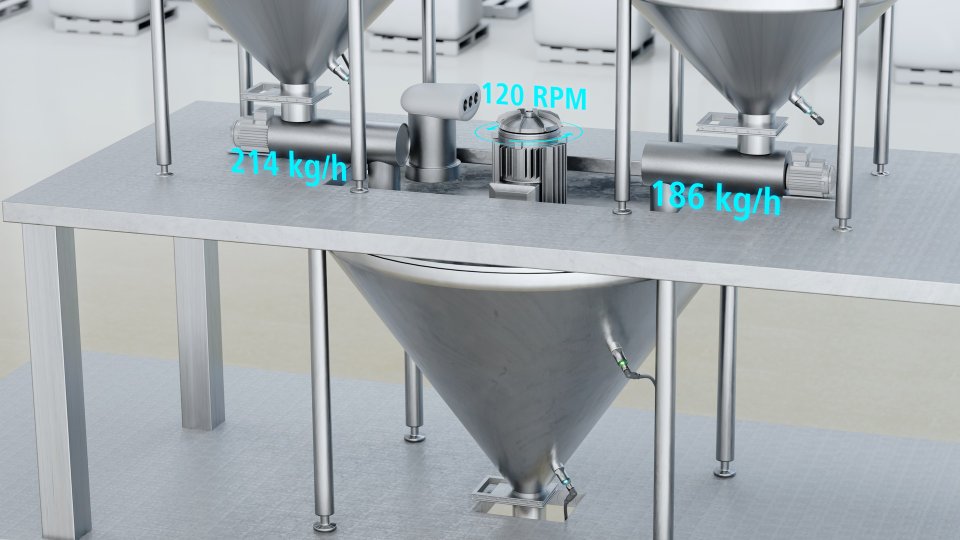
Dosing and mixing monitoring
Guarantee consistent, accurate dosing of dry ingredients and a homogeneous mix.
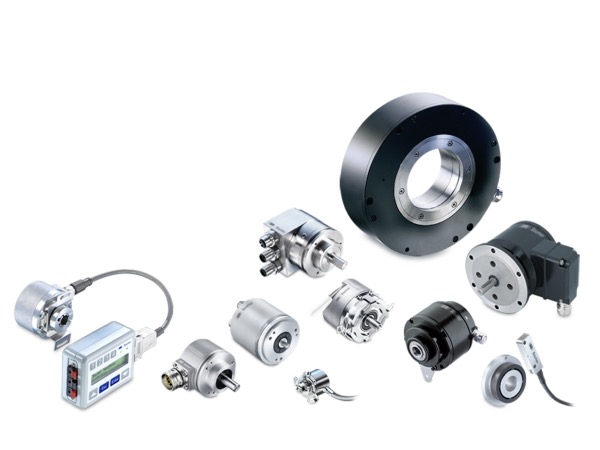
- Control of screw speed with encoders to ensure the required volumetric performance
- Control of screw speed with encoders to achieve a homogeneous mix
- Detection of high and low fill levels in the mixing vessel with point level and continuous fill sensors to control dosing, mixing and material discharge
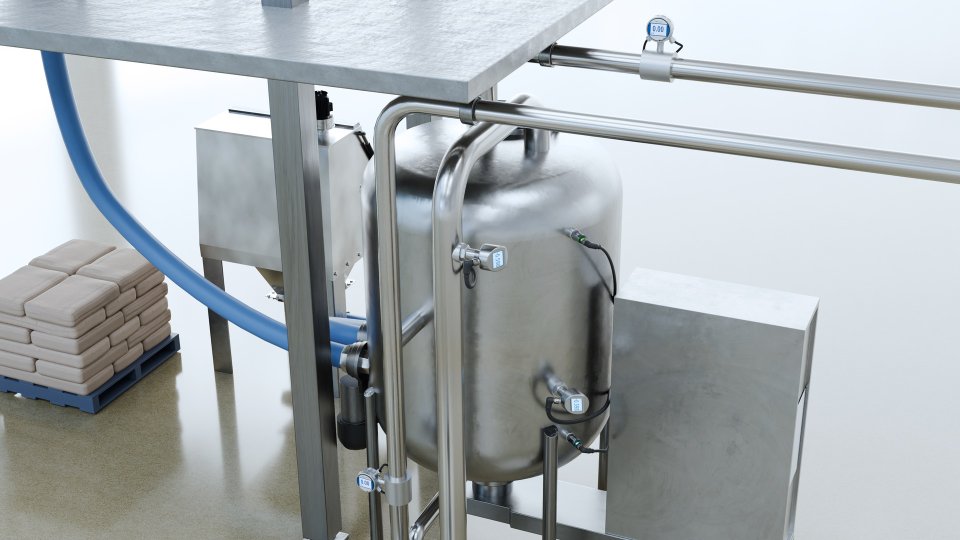
Dissolution monitoring
Guarantee controlled addition, efficient dissolution and mixing of ingredients in a liquid using a high-shear mixer under partial vacuum.
- Control of negative pressure with pressure sensors to effectively draw ingredients into the mixer
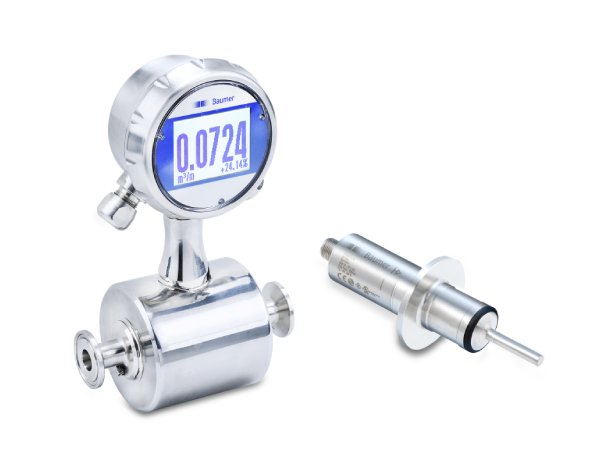
- Measurement of water addition for dissolution and use of flow meters to total the amount during transfer
- Monitoring of mixer speed with encoders to ensure efficient dissolution and mixing
- Detection of high and low fill levels with point level sensors to prevent overfilling and ensure complete emptying of the mixer
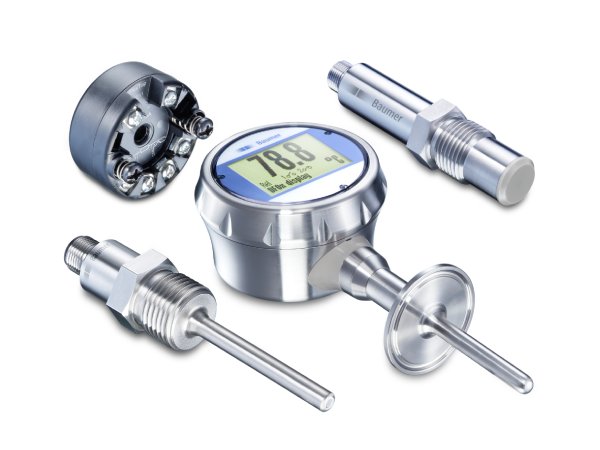
- Monitoring of ambient temperature inside the mixer with temperature sensors to prevent thermal damage to the product
Certifications and Approvals
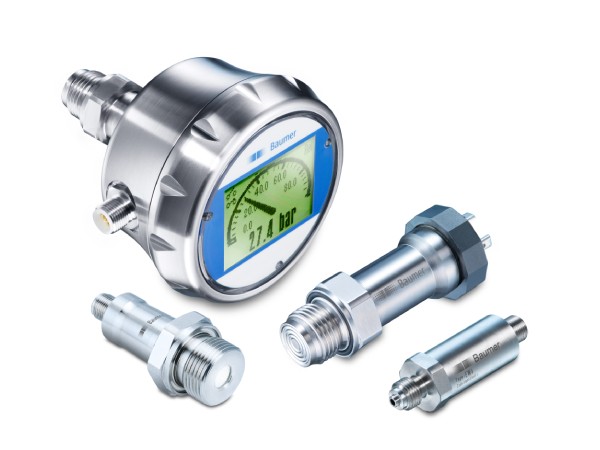
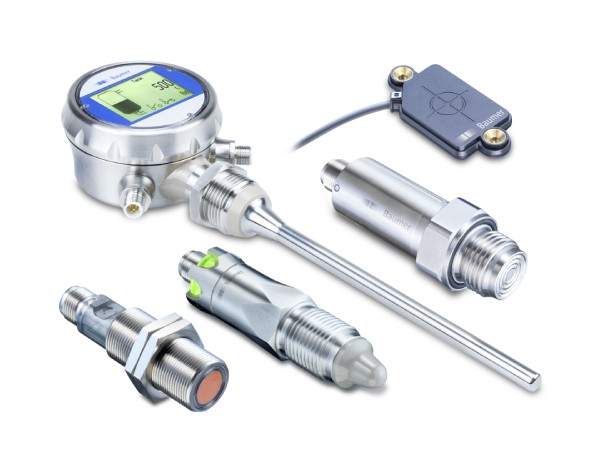
Baumer sensors are certified in accordance with all international design and material standards relevant to the food and beverage industry. Baumer's internal processes are certified according to DIN ISO 9000 requirements. Hygienic sensors are designed, developed and manufactured in compliance with 3-A and EHEDG guidelines to guarantee the highest standards in food production.
An end-to-end development process, from the initial concept stage through to series production, is continuously validated by our customers' use. Our sensors comply with IP69 protection and undergo additional testing under our corporate proTect+ standard for maximum reliability and durability.
Have a Sector-Specific Question?
Our expert engineers are ready to help you identify the most suitable solution for your industry.