Sensor Solutions for CIP Applications — Food Safety and Maximum Efficiency
Precision for superior cleaning efficiency and reduced operating costs.
Precision for superior cleaning efficiency and reduced operating costs
Our state-of-the-art sensor solutions address every dimension of the Sinner circle, delivering precise, fast and repeatable measurement values that reduce cleaning times as well as detergent and water use.
Decades of industry experience for food safety and uninterrupted operation
Our hygienically designed, robustly built sensors operate reliably in the demanding environment and harsh ambient conditions of your CIP system, ensuring minimum downtime with no compromise on food safety.
Tailored one-stop solutions for flexible, simple integration
We offer the full package of high-performance technologies for CIP systems of every type and complexity, as a sensor solution designed to your needs from a single supplier.
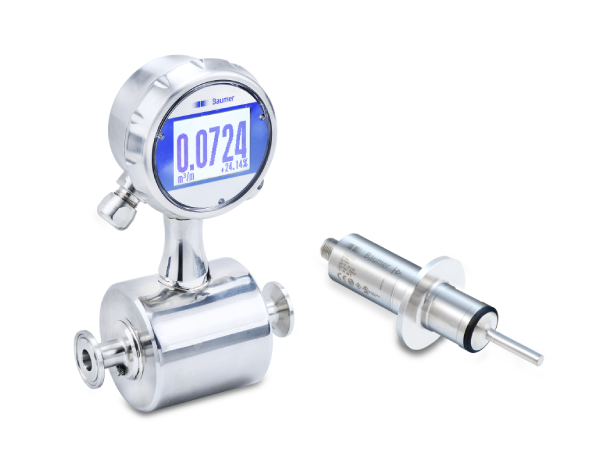
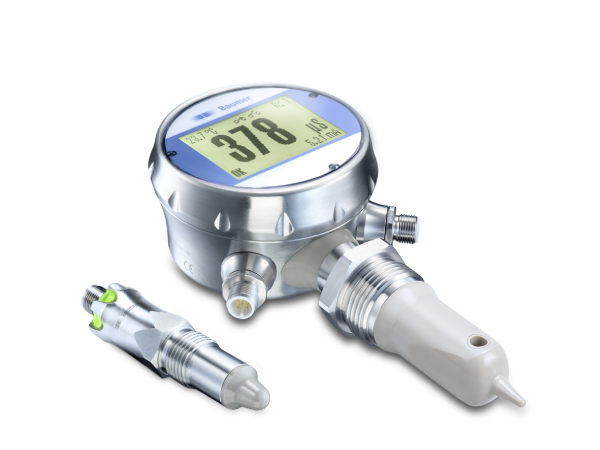
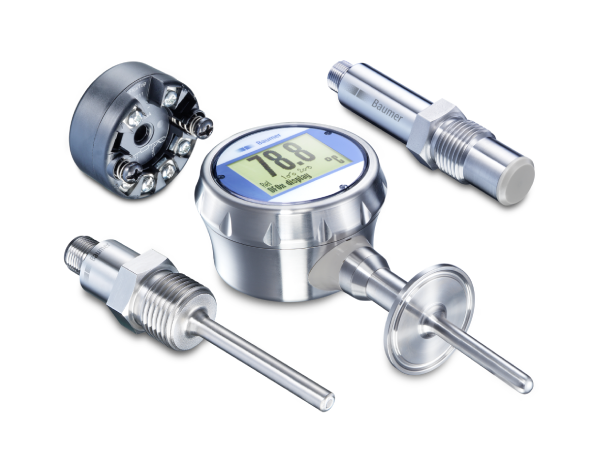
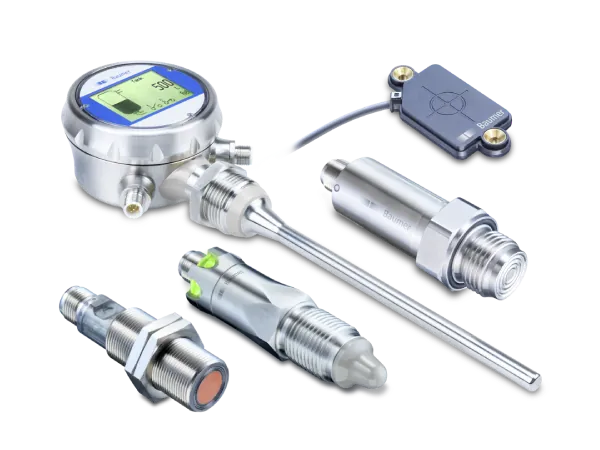
Efficient and reliable CIP processes rely on highly precise, fast and robust sensors that monitor conductivity, temperature, flow and level in real time. These sensors ensure cleaning agents are always ready for use and that cleaning parameters are continuously met. Smart sensor technology thereby enables shorter cleaning cycles with reduced water and chemical use — increasing production line availability while preserving cleanliness and food safety, and lowering costs.
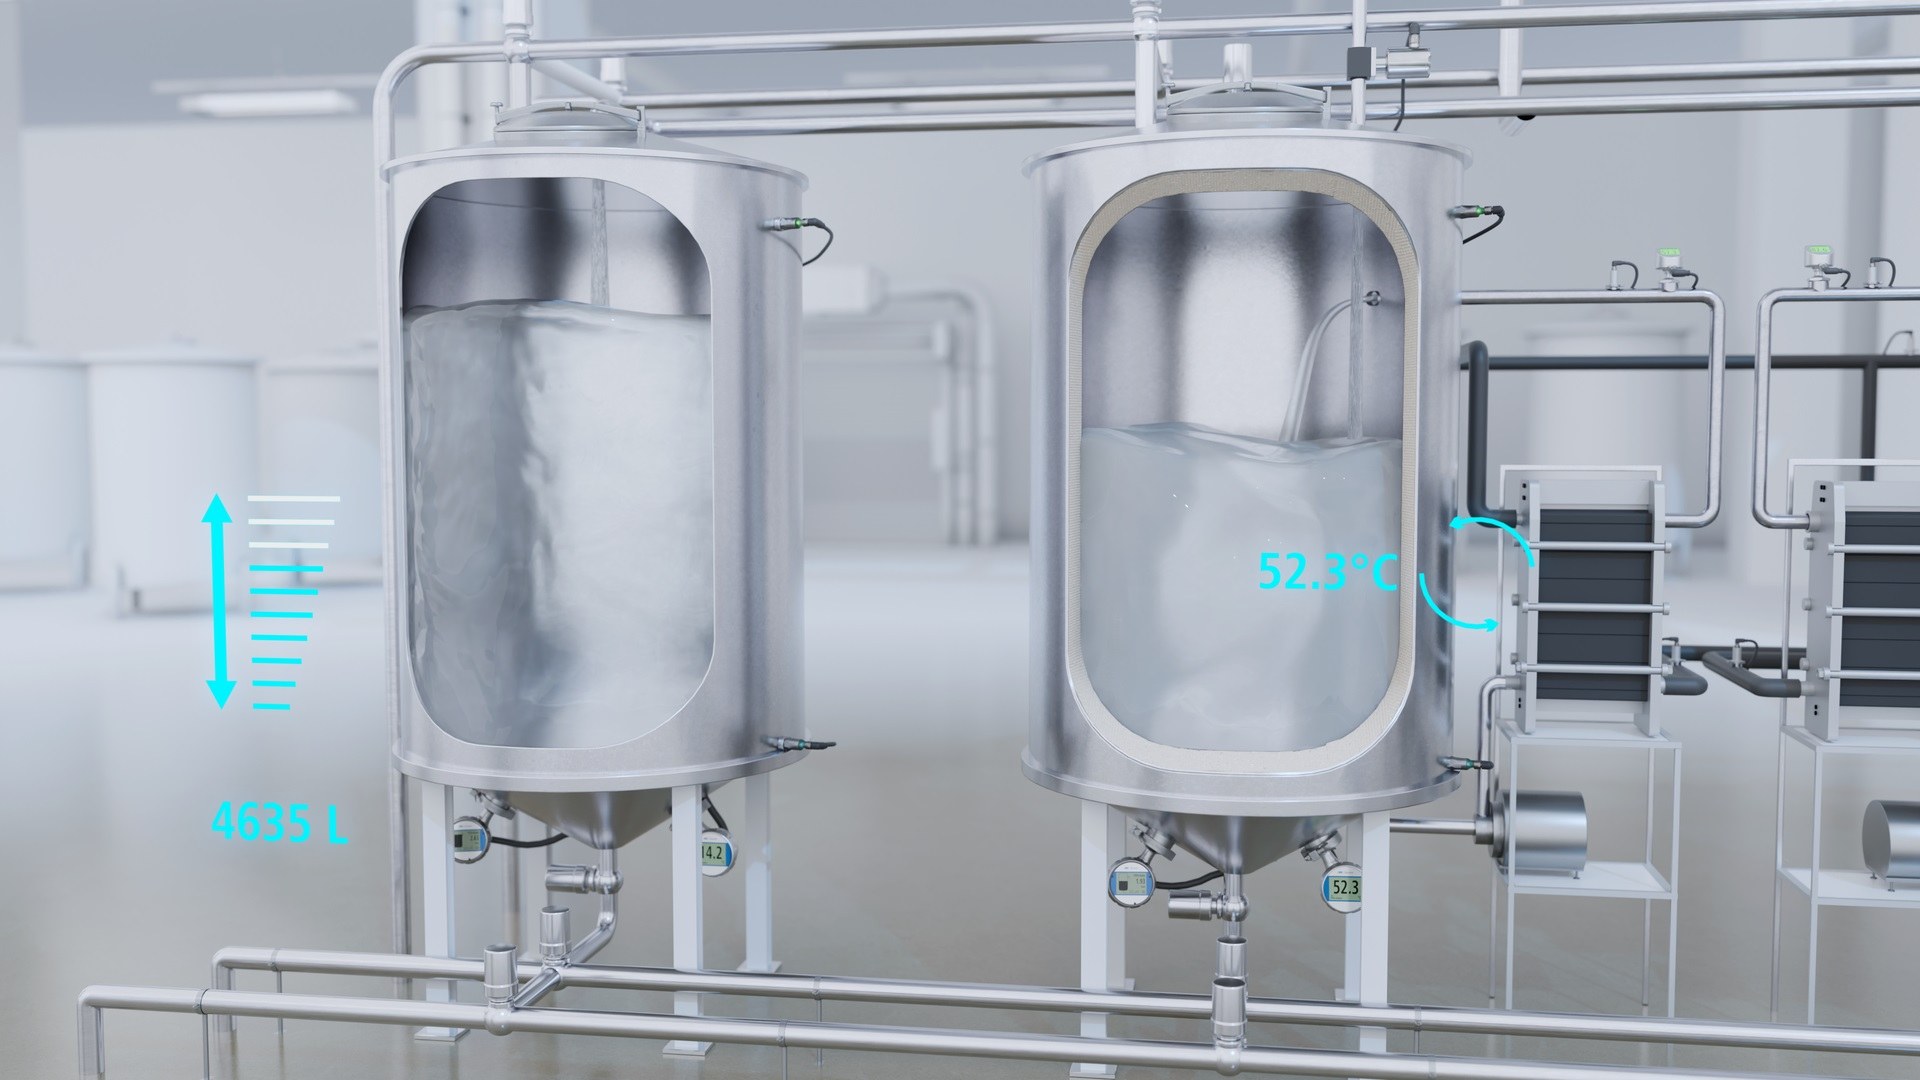
CIP tank monitoring
Ensure a continuous and sufficient supply of water and cleaning solutions for cleaning cycles.
- check_circle Detection of high and low limit levels to prevent overflow or dry running
- check_circle Continuous fill-level measurement to ensure sufficient water and media are available
- check_circle Monitoring of lye and acid temperatures and activation of the heating bypass line to ensure constant readiness to start the cleaning cycle
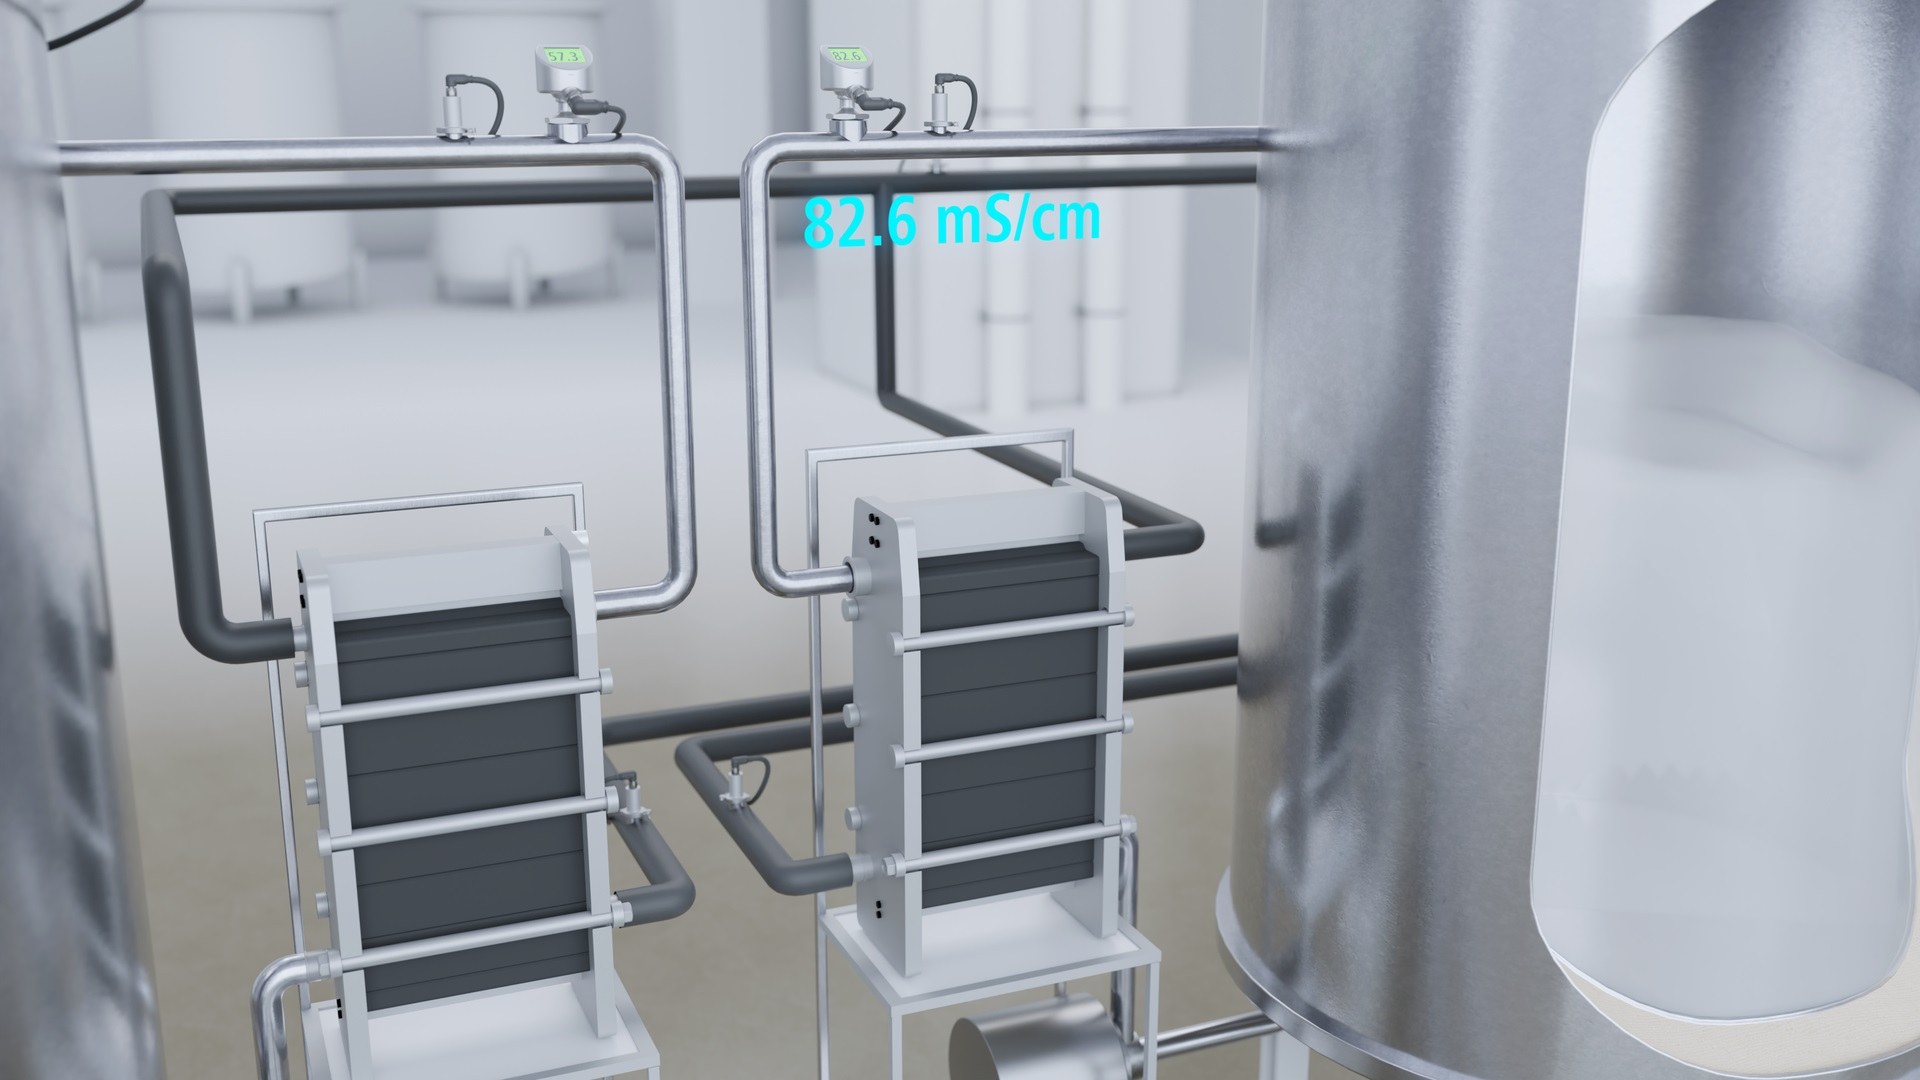
Media concentration and heating monitoring
Ensure the correct cleaning-media concentration and control the heating process in the recirculation line for continuous system readiness.
- check_circle Continuous media availability ensured by measuring lye and acid concentration with conductivity sensors, enabling water and concentrate dosing
- check_circle Monitoring of bypass temperature and flow rate to control the heating process
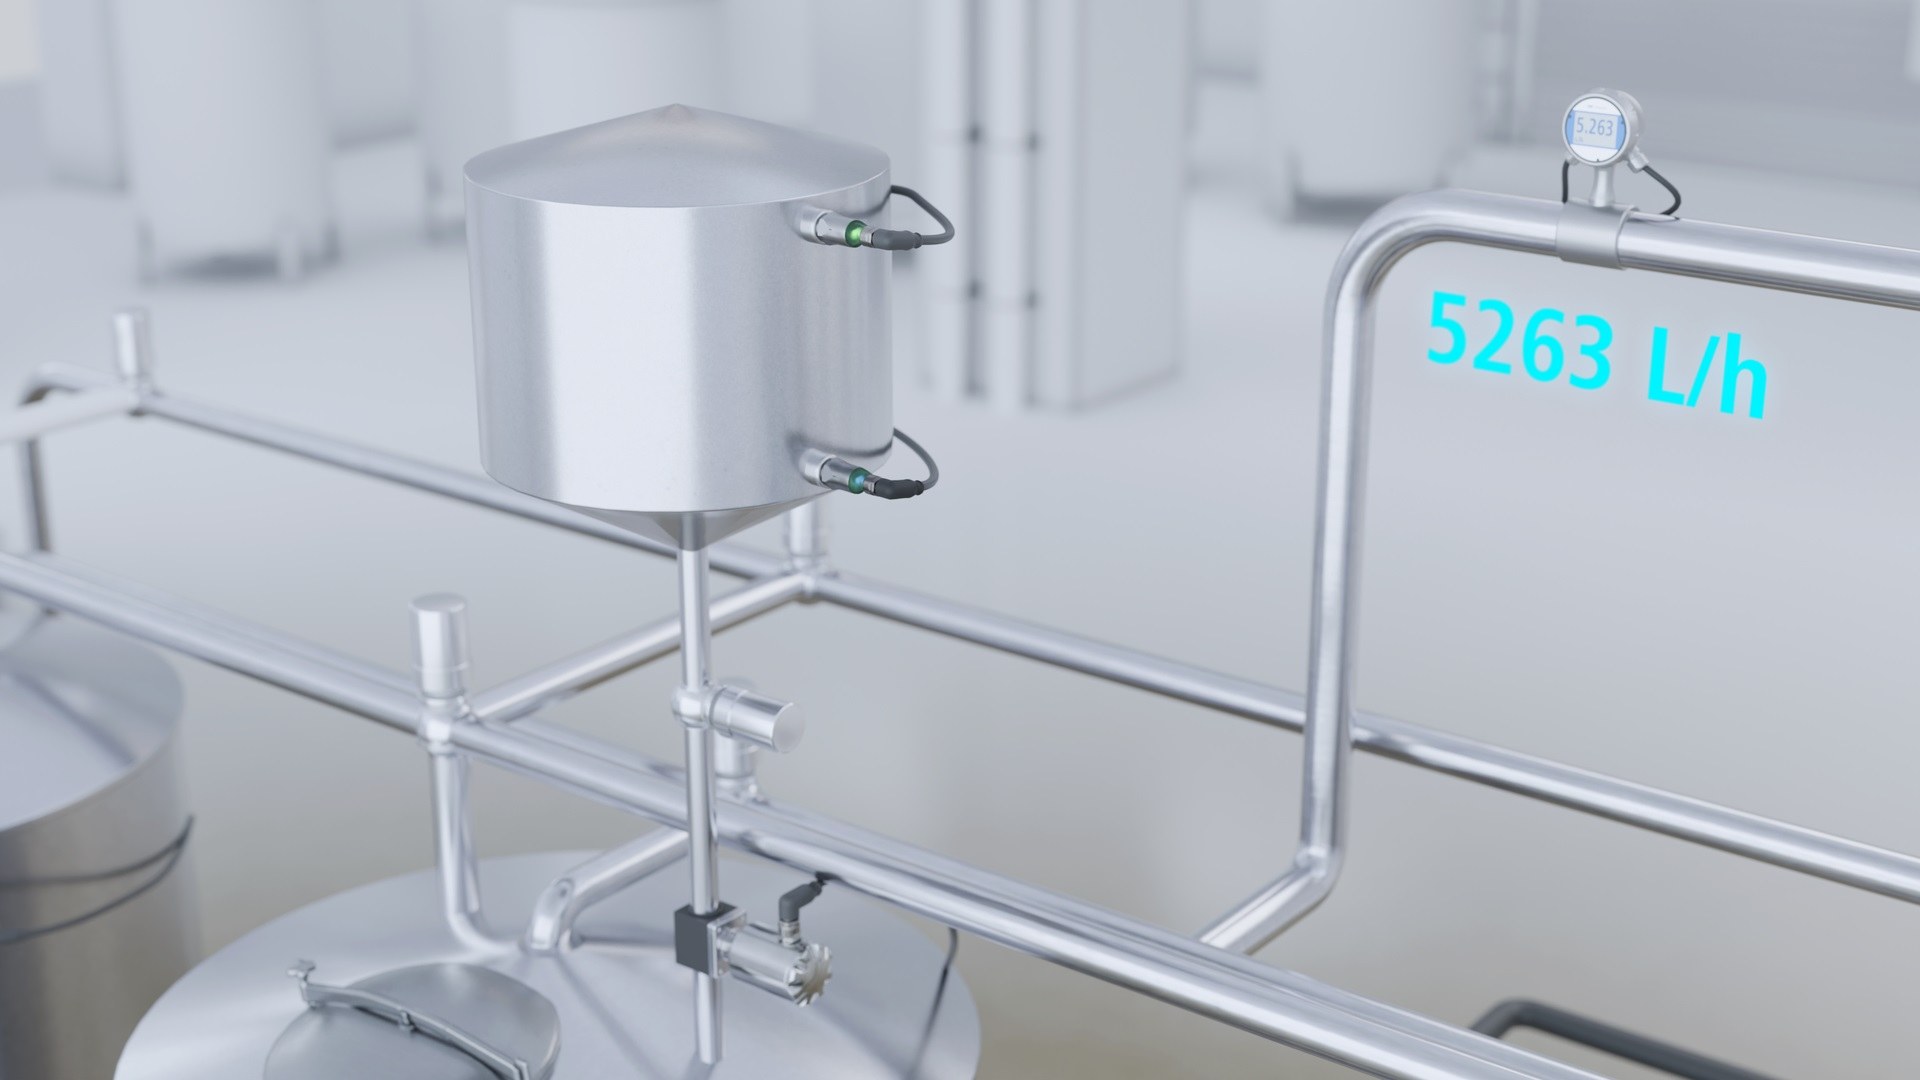
Concentrate and water dosing
Ensure precise and safe addition of concentrated lye, acid and water.
- check_circle Monitoring of water, lye and acid dosing with flow sensors to reach the desired concentrations in CIP tanks
- check_circle Monitoring of concentrate tank fill levels to ensure sufficient supply, preventing dry running and uninterrupted cleaning-media readiness
- check_circle Where concentrates must be pumped into CIP tanks, pressure sensors ensure unobstructed flow for safety, preventing leaks caused by overpressure
Dry-running protection
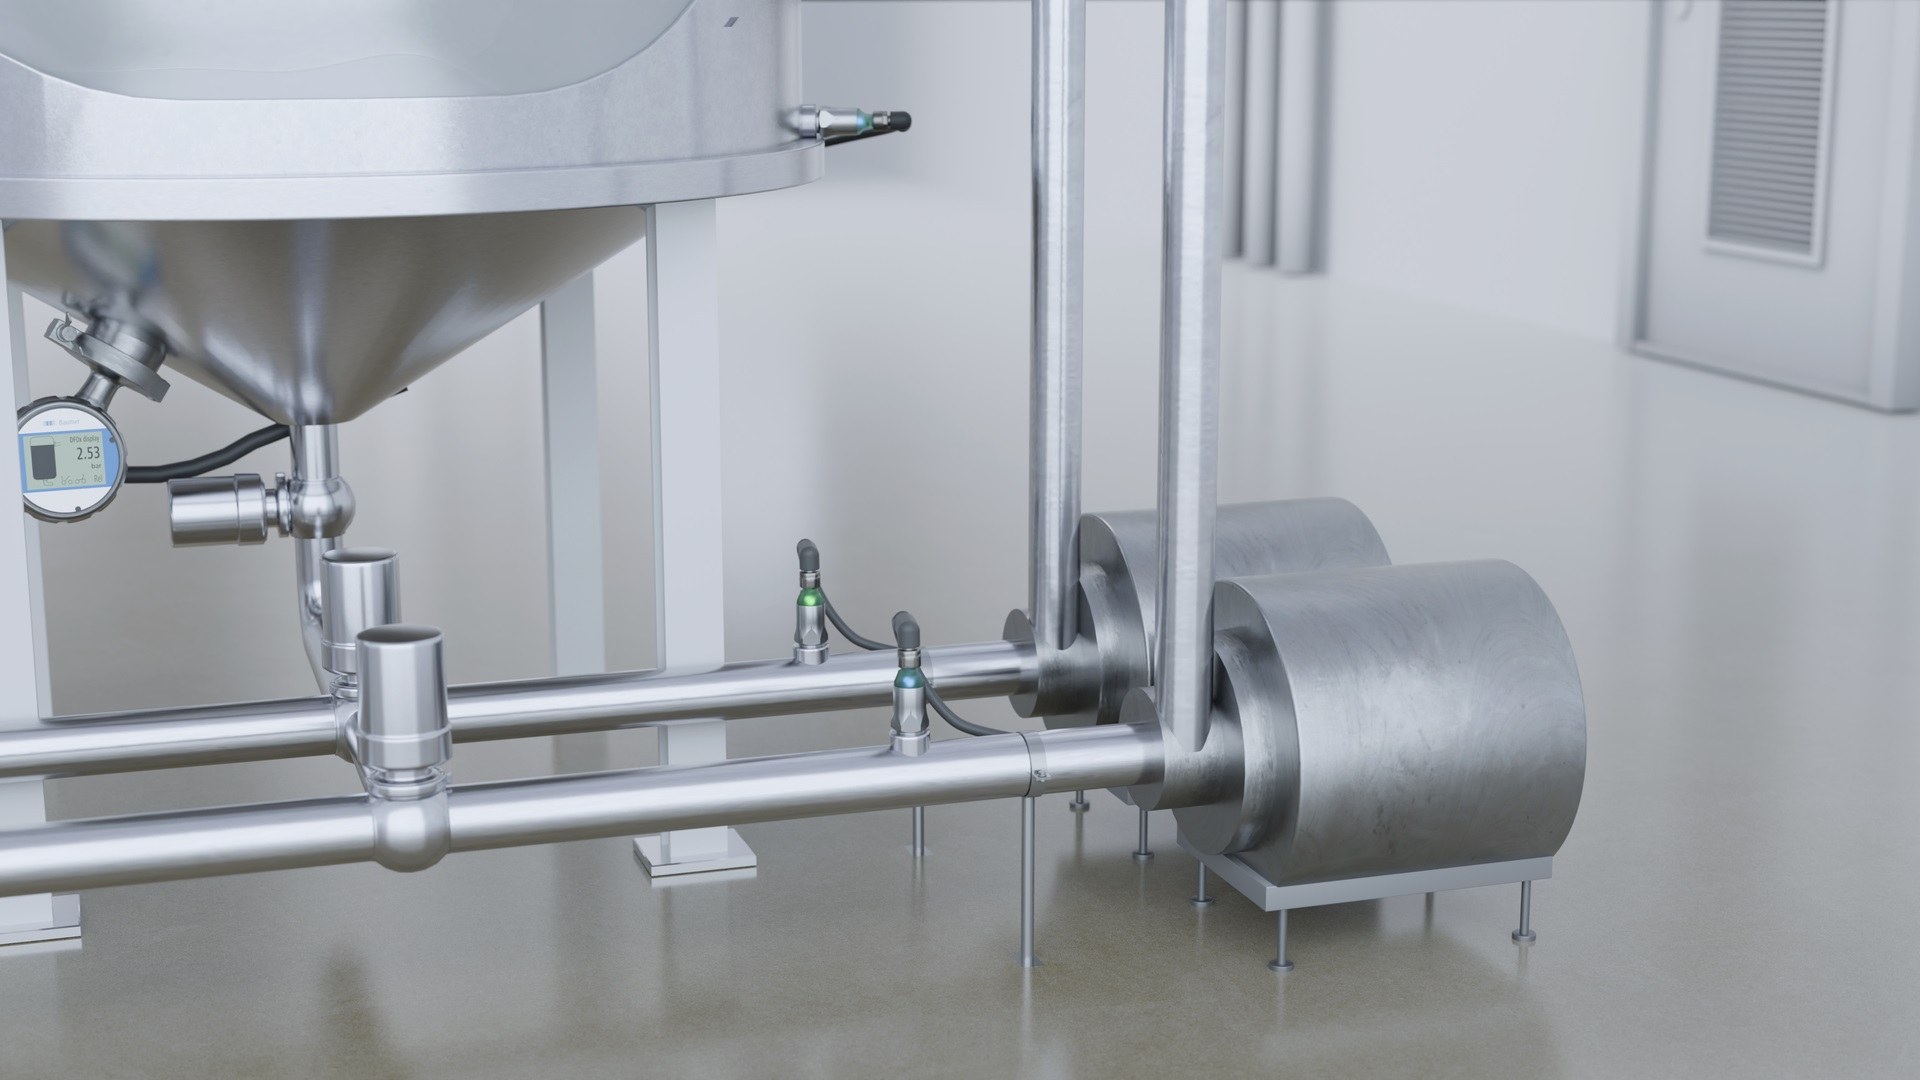
Protect pumps from damage by preventing prolonged dry running.
- check_circle CleverLevel level switches or bubble-detection sensors reliably identify empty pipes by distinguishing between liquid, foam, gas or gas bubbles
CIP supply monitoring
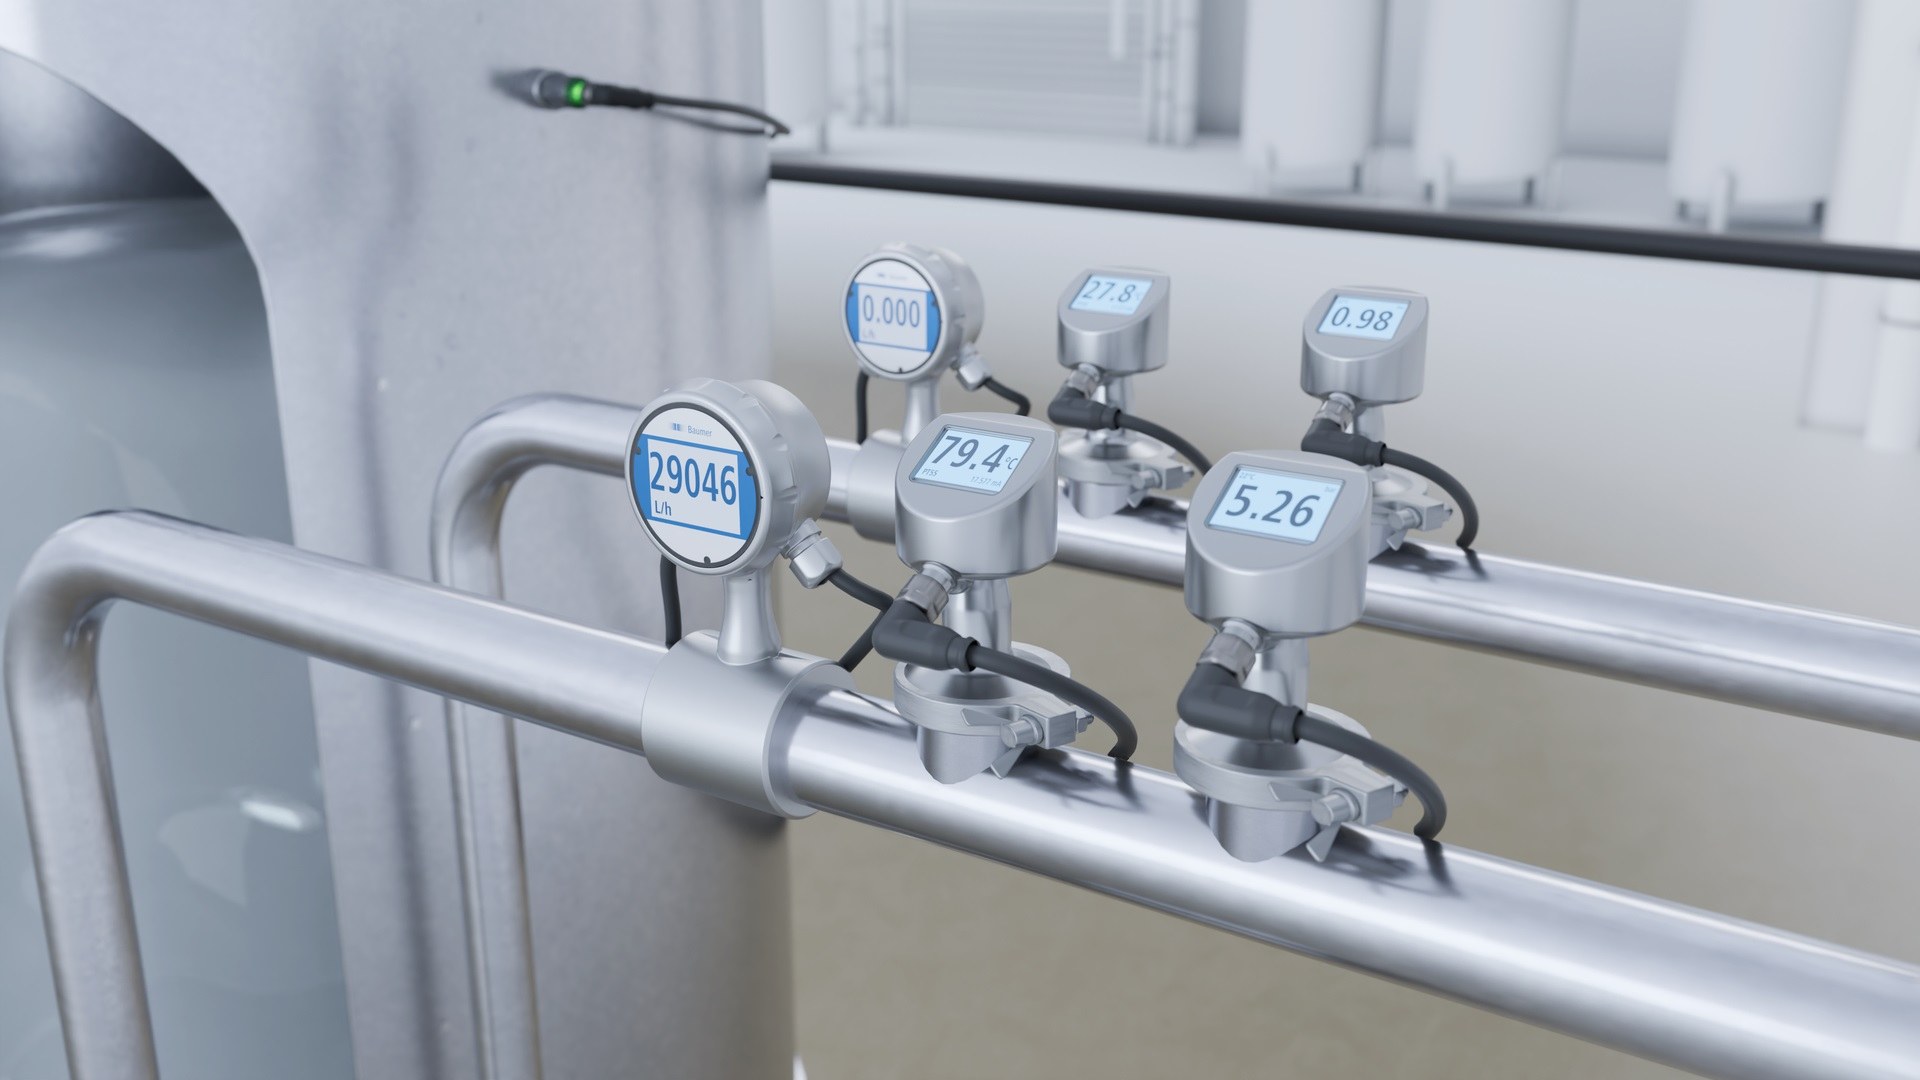
Ensure the correct media and process parameters as a precondition for efficient cleaning that saves time and resources.
- check_circle Monitoring of flow rate to ensure sufficient flow velocity for the turbulence required for optimal cleaning effectiveness
- check_circle Measurement of the temperature of water and cleaning media entering the CIP circuit
- check_circle Monitoring of inlet-line pressure to ensure proper operation of spray balls and detect blockages in the CIP circuit
Quality monitoring on CIP return
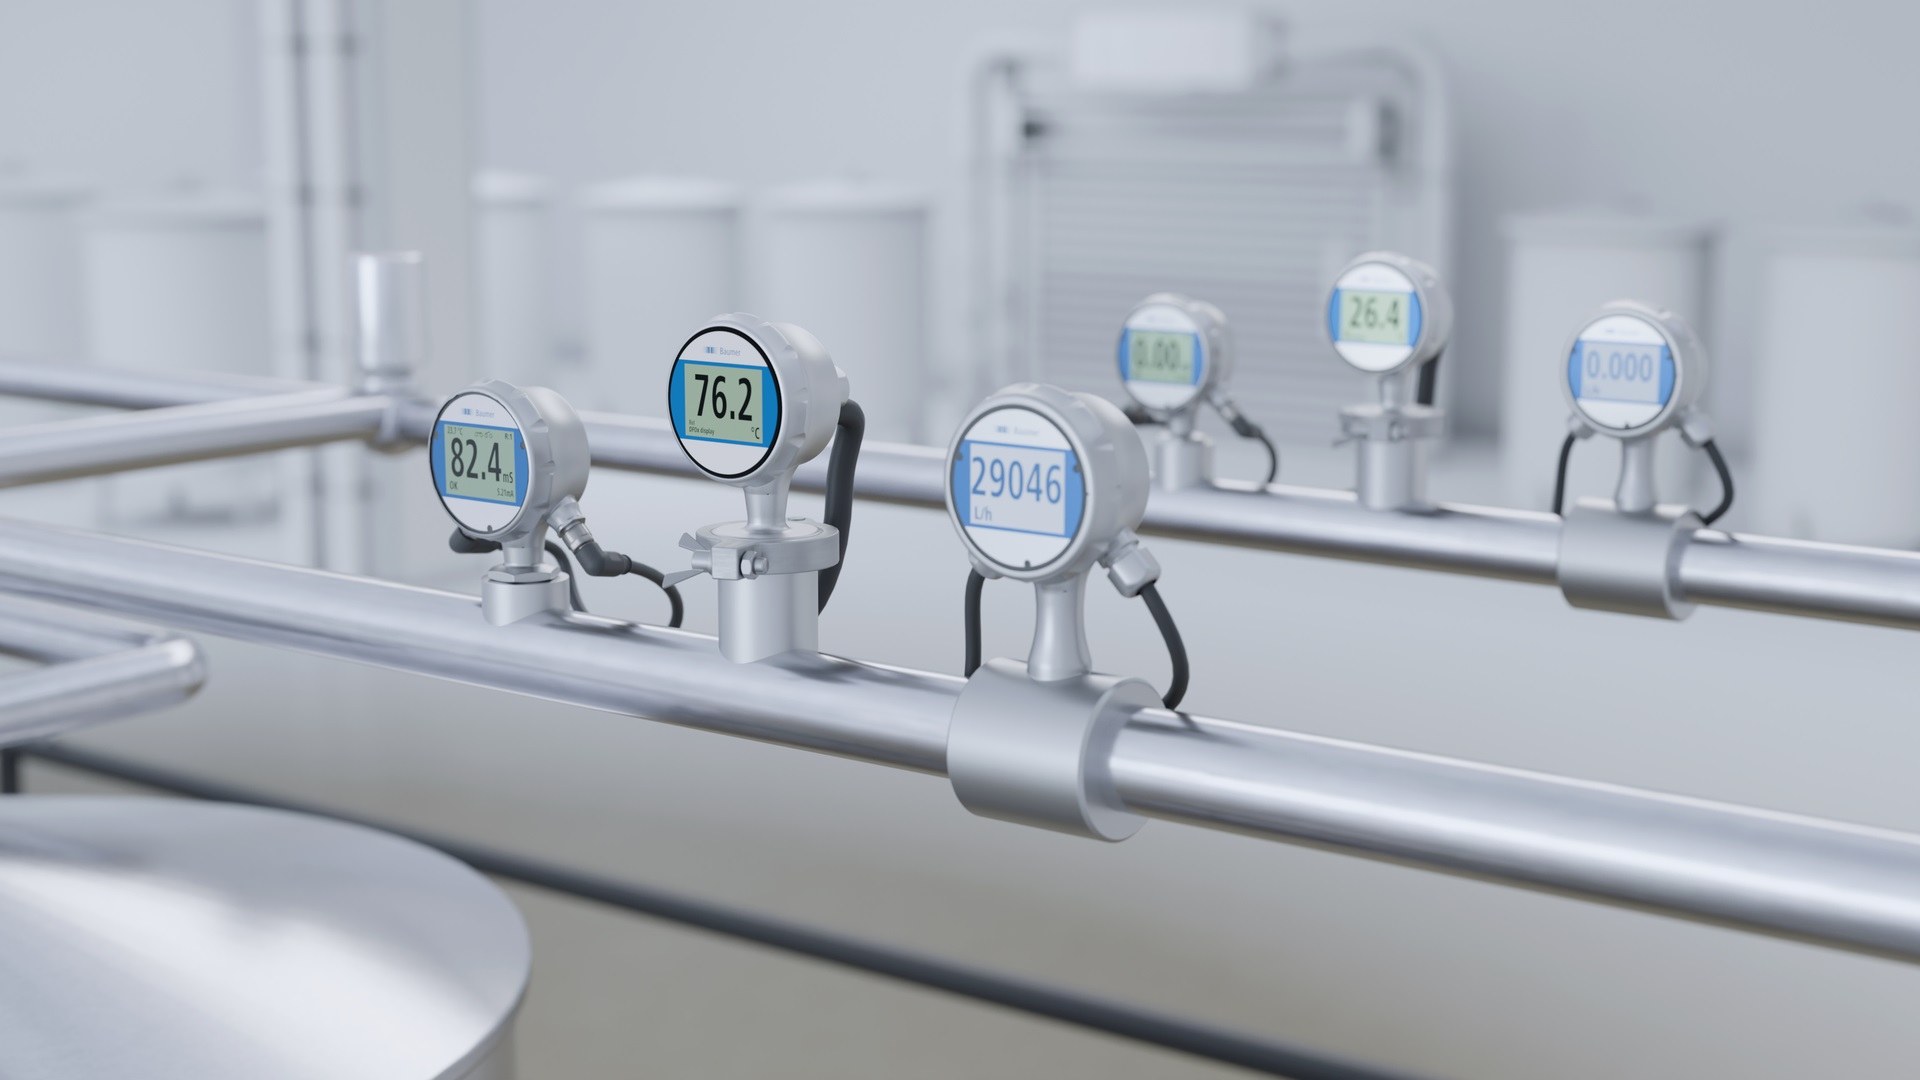
Ensure compliance with cleaning parameters and durations throughout the CIP circuit for effective and safe cleaning according to the Sinner circle.
- check_circle Conductivity measurement to verify correct lye and acid concentrations throughout the CIP circuit and to precisely detect phase transitions with fast temperature compensation
- check_circle Monitoring of flow rate to ensure sufficient velocity — and therefore turbulence — throughout the CIP circuit
- check_circle Monitoring of lye and acid solution temperature to ensure cleaning effectiveness
Specialized mechanical instrumentation for the process industry
Since 1849, Bourdon has offered dedicated solutions for reliable pressure and temperature measurement. All products are manufactured to the highest quality and safety requirements, drawing on our expertise in the railway market and its applications. Bourdon also has a worldwide presence for better service.
Browse Bourdon products arrow_forwardBaumer sensors are certified in compliance with all international design and material standards relevant to the food and beverage industry. Internal processes at Baumer comply with DIN ISO 9000 requirements and are certified accordingly. Hygienic sensors are designed, developed and manufactured in compliance with 3-A and EHEDG guidelines to ensure the highest standards in food production.
An end-to-end development process, from the initial concept phase through to series production, is continuously validated by our customers' actual use. Sensors comply with IP68/IP69K protection class and are additionally tested according to our own internal proTect+ standard to ensure maximum reliability and durability.
Learn more about Baumer's other food and beverage solutions
Discover our sensor solutions for filtration, heat exchange, centrifugation, extrusion, evaporation, dairy, brewing and beverage production.
Back to Food & Beverage SolutionsHave questions?
Our experts are happy to answer all your questions and provide further information. Just send us an email.