Sensor solutions for enhanced reliability and efficiency in filtration
Our technologically advanced sensor solutions deliver precise, repeatable measurement values for your filtration processes, boosting your competitiveness with peak process performance and consistently high product quality.
Precision for superior efficiency and reduced operating costs
Our technologically advanced sensor solutions deliver precise, repeatable measurement values for your filtration applications, boosting your competitiveness with peak process performance and consistently high product quality.
Long-standing industry experience for uninterrupted operation
Our hygienically designed, robustly built sensors operate reliably in the demanding filtration environment and harsh ambient conditions, enabling uninterrupted production with minimum downtime and no compromise on food safety.
Real-time monitoring for optimized production, cleaning and maintenance cycles
Fast, repeatable measurement results enable proactive detection of fouling, blockages and membrane wear, guaranteeing uninterrupted filtration operation and minimum product loss.
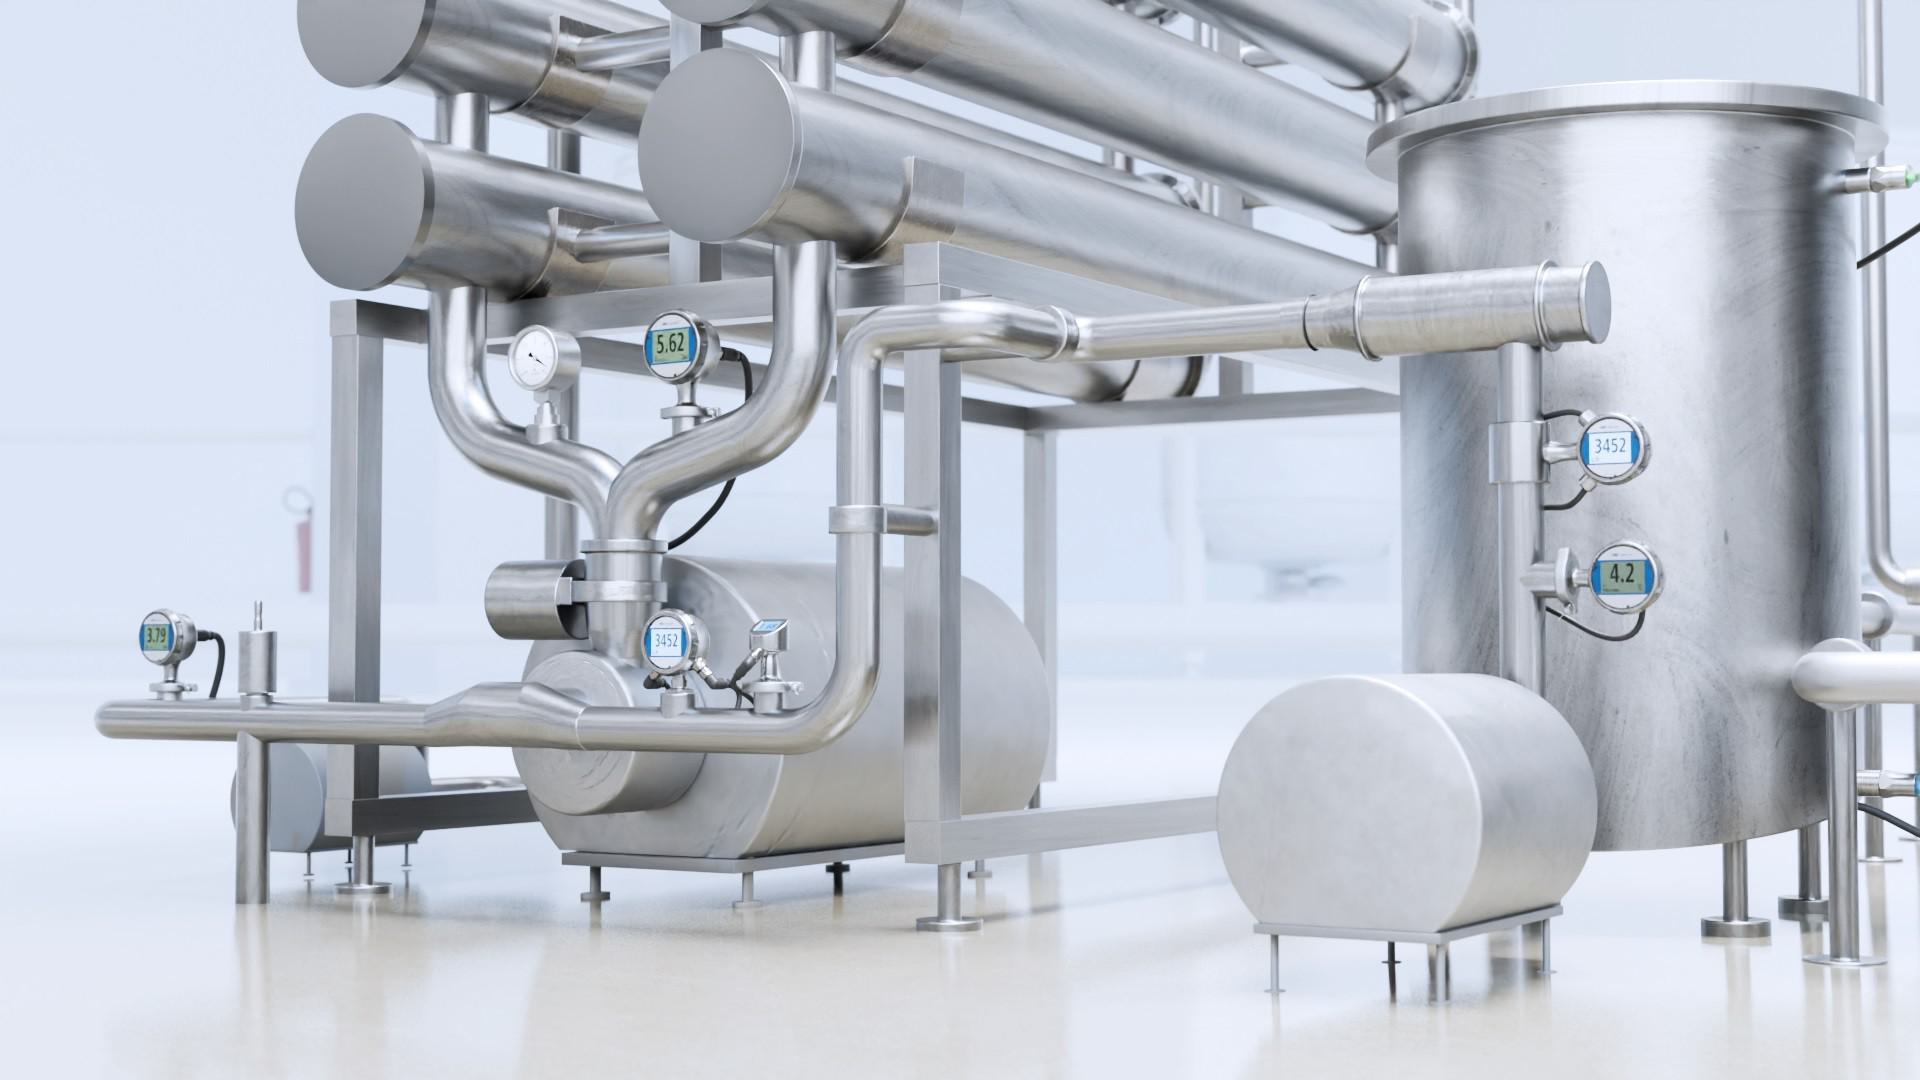
Product feed monitoring
Guarantee stable operating conditions through continuous monitoring of feed parameters, preventing premature membrane fouling or damage.
- Continuous pressure and flow-rate measurement for a constant throughput, preventing overloading or underfeeding of membranes and stress-sensitive products
- Monitor feed composition with conductivity sensors to detect changes in product concentration and prevent scaling/fouling
- Temperature monitoring to control viscosity and prevent damage to heat-sensitive components
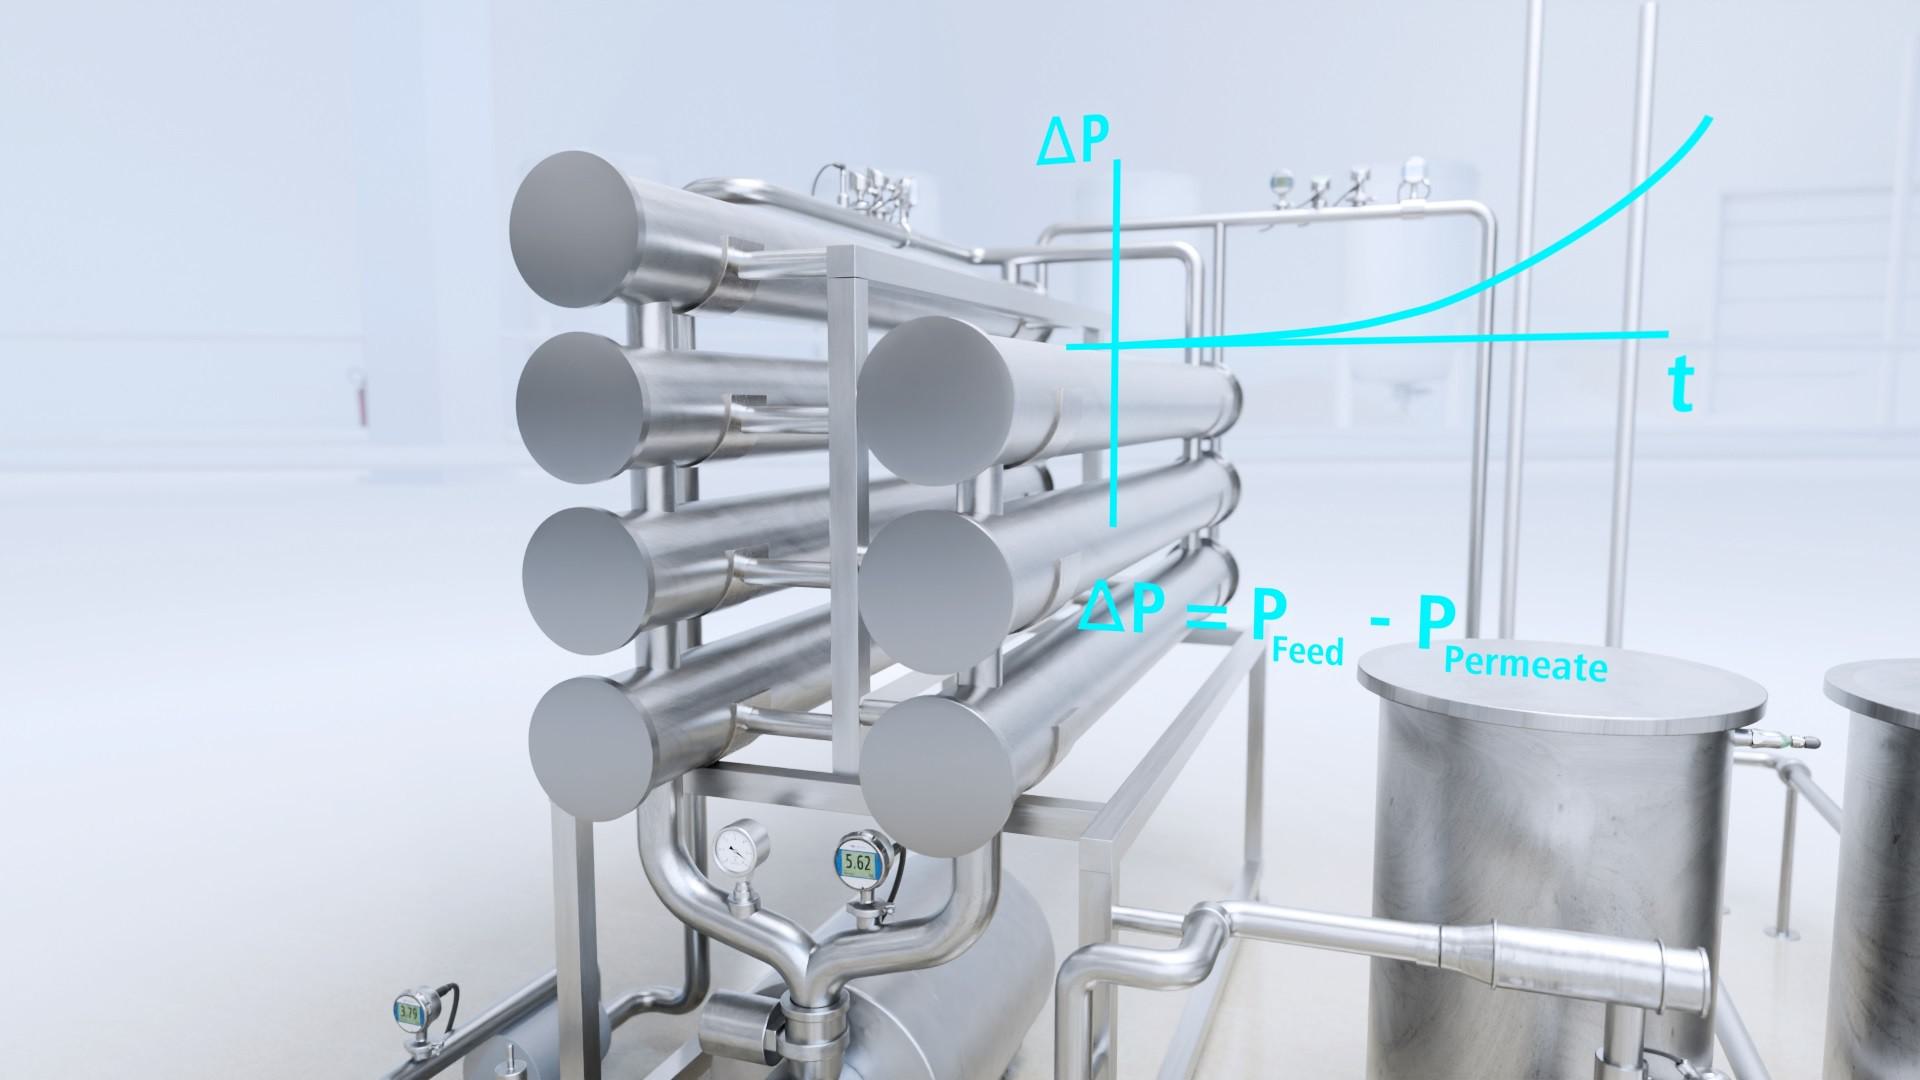
Transmembrane pressure (TMP) monitoring
Reliable detection of fouling or blockage for optimal cleaning-cycle timing and detection of membrane damage.
- Monitor gradual TMP changes with precise pressure measurement to detect product buildup trends and membrane wear/aging
- Detection of sudden TMP spikes as an indicator of membrane damage
- Monitor filtration efficiency with optimized cleaning and backwash timing to minimize planned downtime
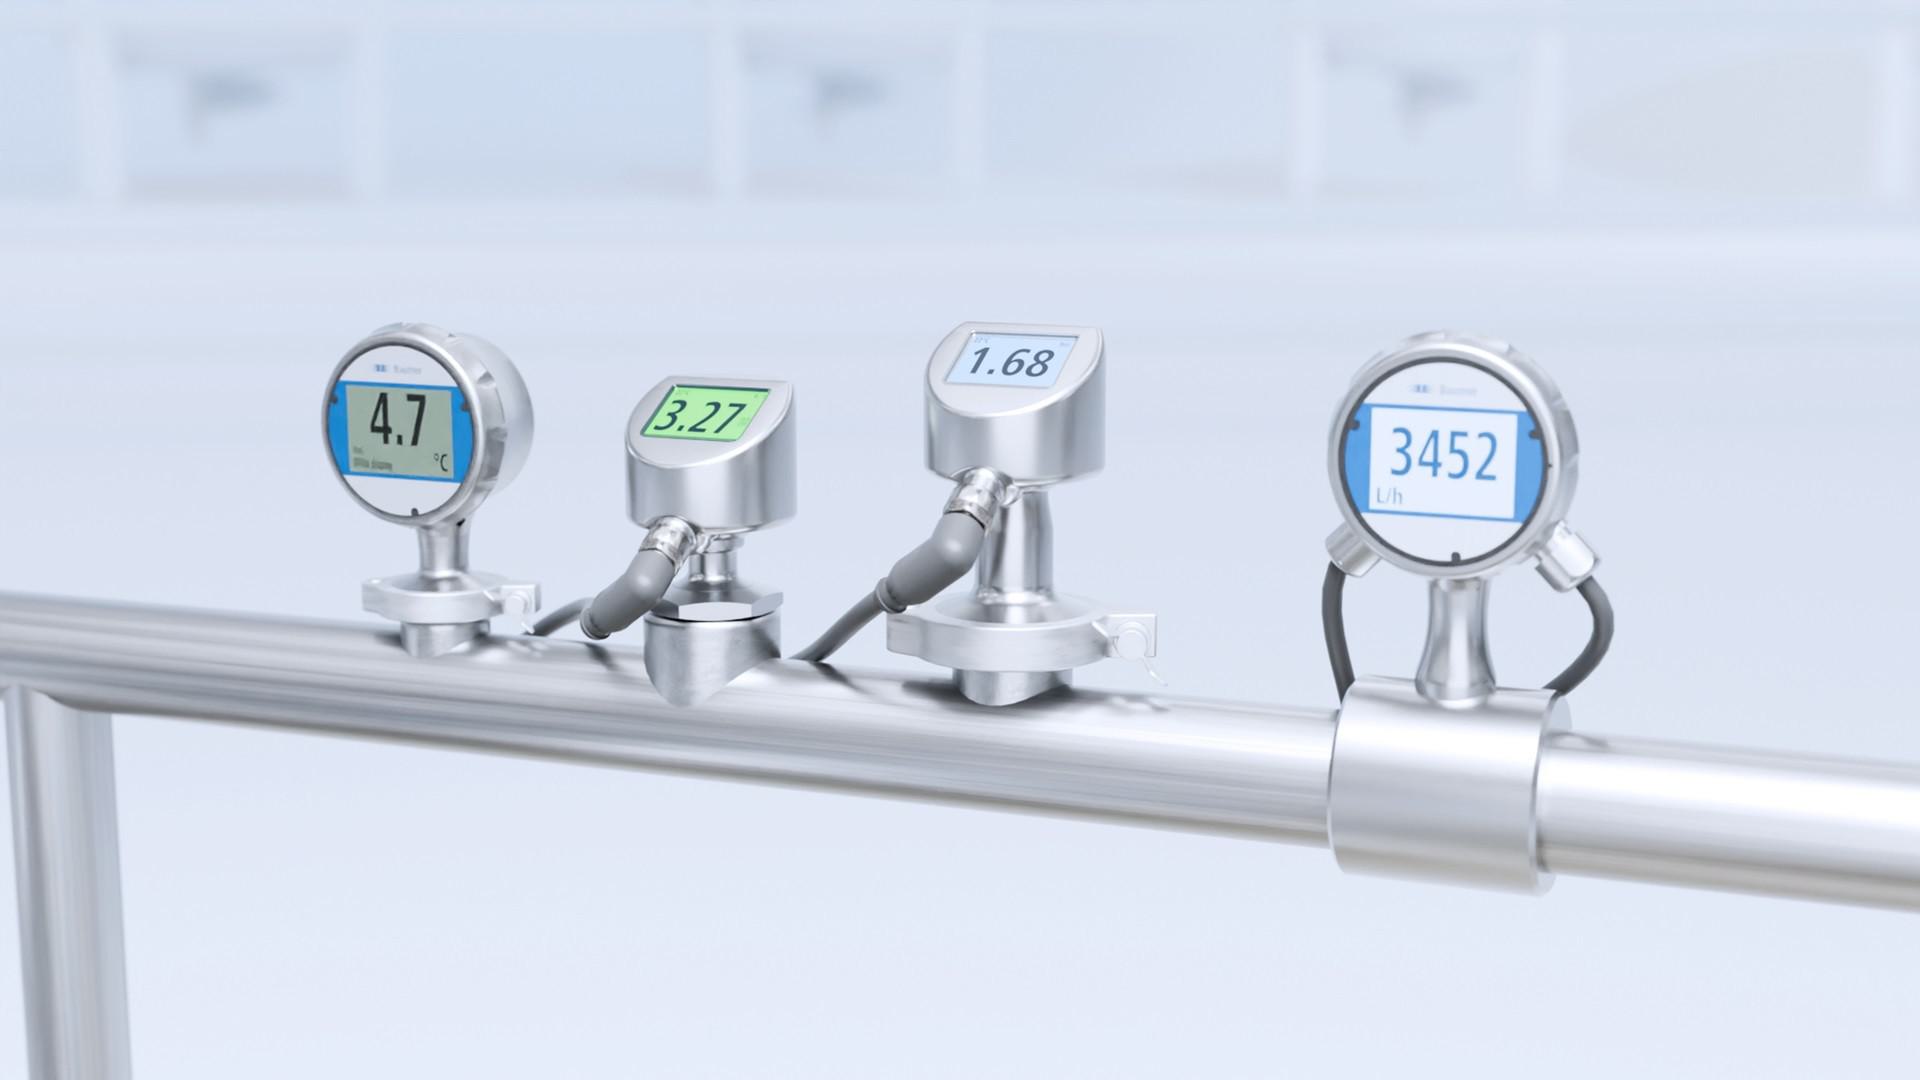
Quality control in the permeate stream
Guarantee compliance with quality standards and prevent contaminated products from entering downstream processes.
- Maintain a stable, efficient filtration operation through precise measurement of pressure and flow rate
- Ensure rapid detection of quality issues and membrane damage by monitoring conductivity
- Temperature monitoring for product quality assurance, especially for heat-sensitive products
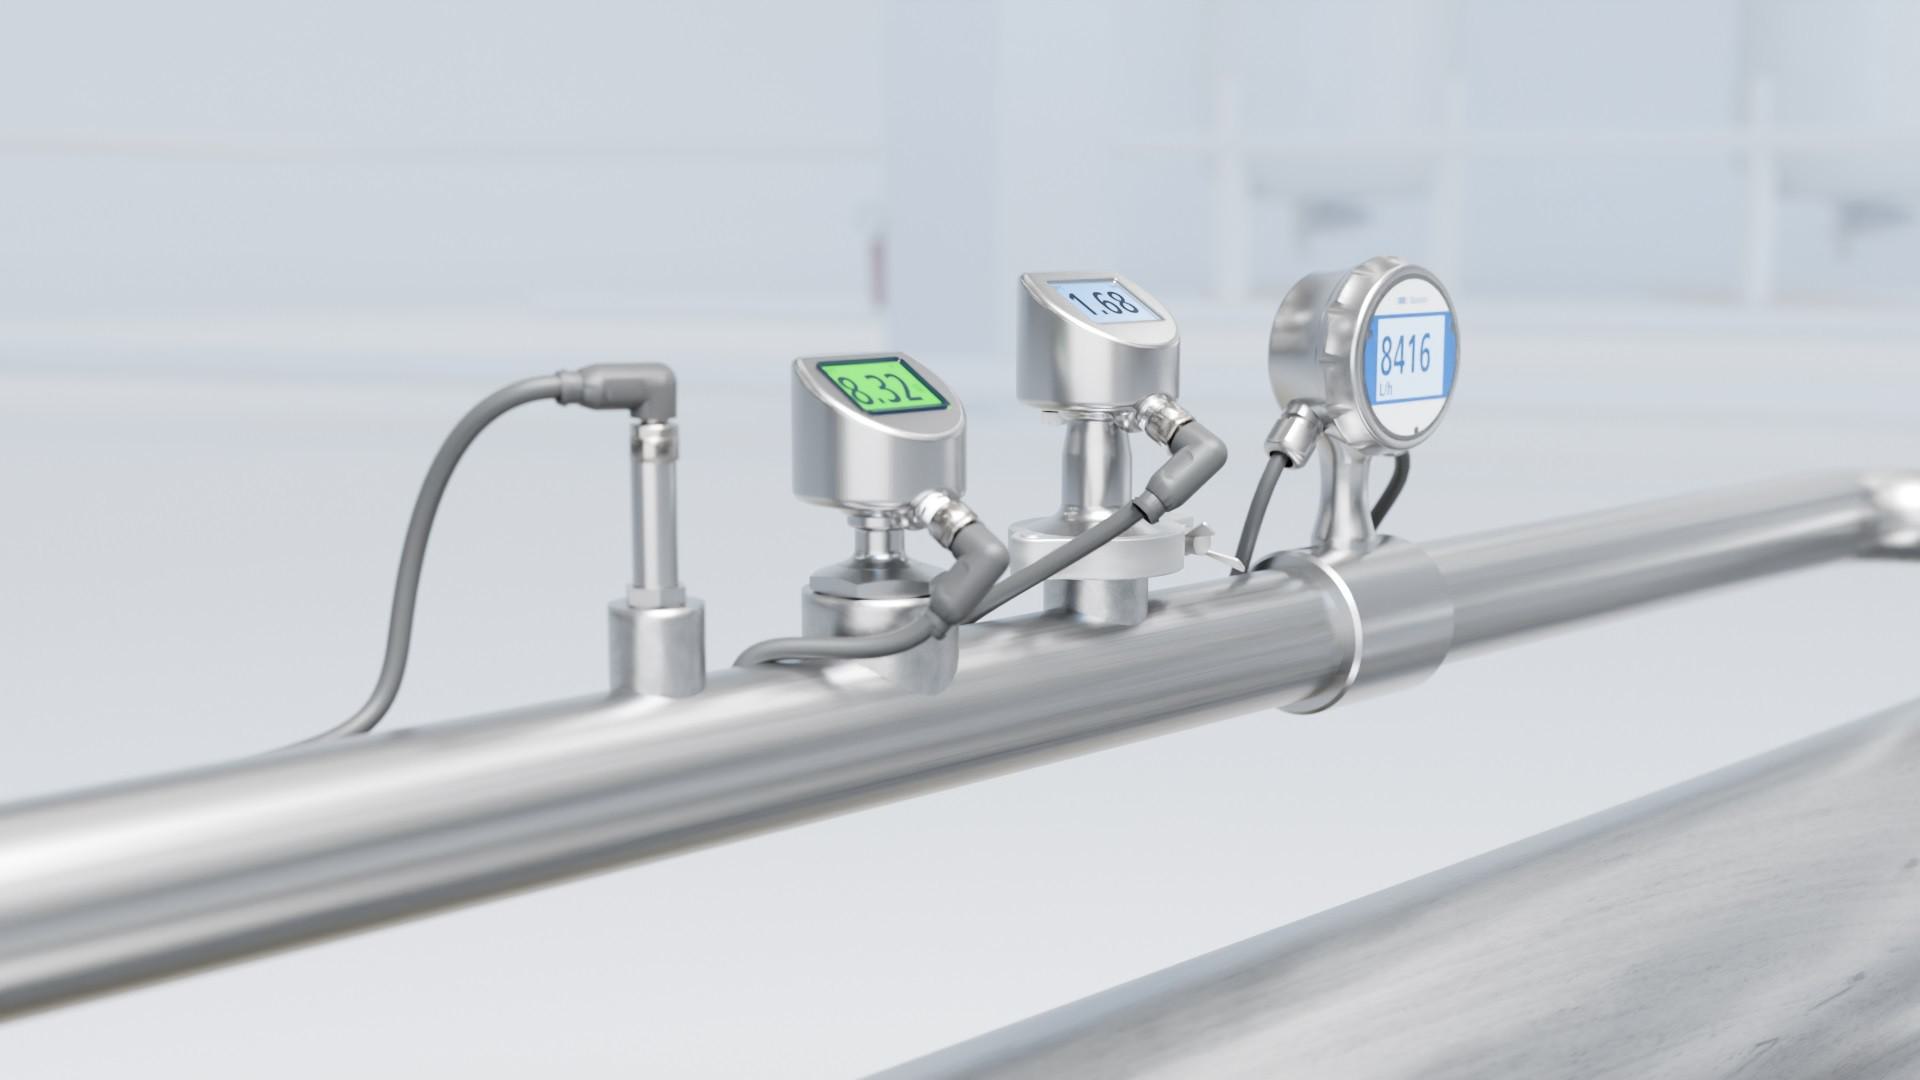
Retentate stream monitoring
Guarantee filtration efficiency by balancing retentate flow parameters and prevent excessive fouling.
- Pressure monitoring to maintain system balance and prevent excessive backpressure for efficient operation without membrane damage
- Cross-flow velocity measurement using flow sensors to ensure the membrane continuously self-cleans
- Monitor retentate concentration with conductivity sensors for optimal retentate discharge timing in recirculating filtration
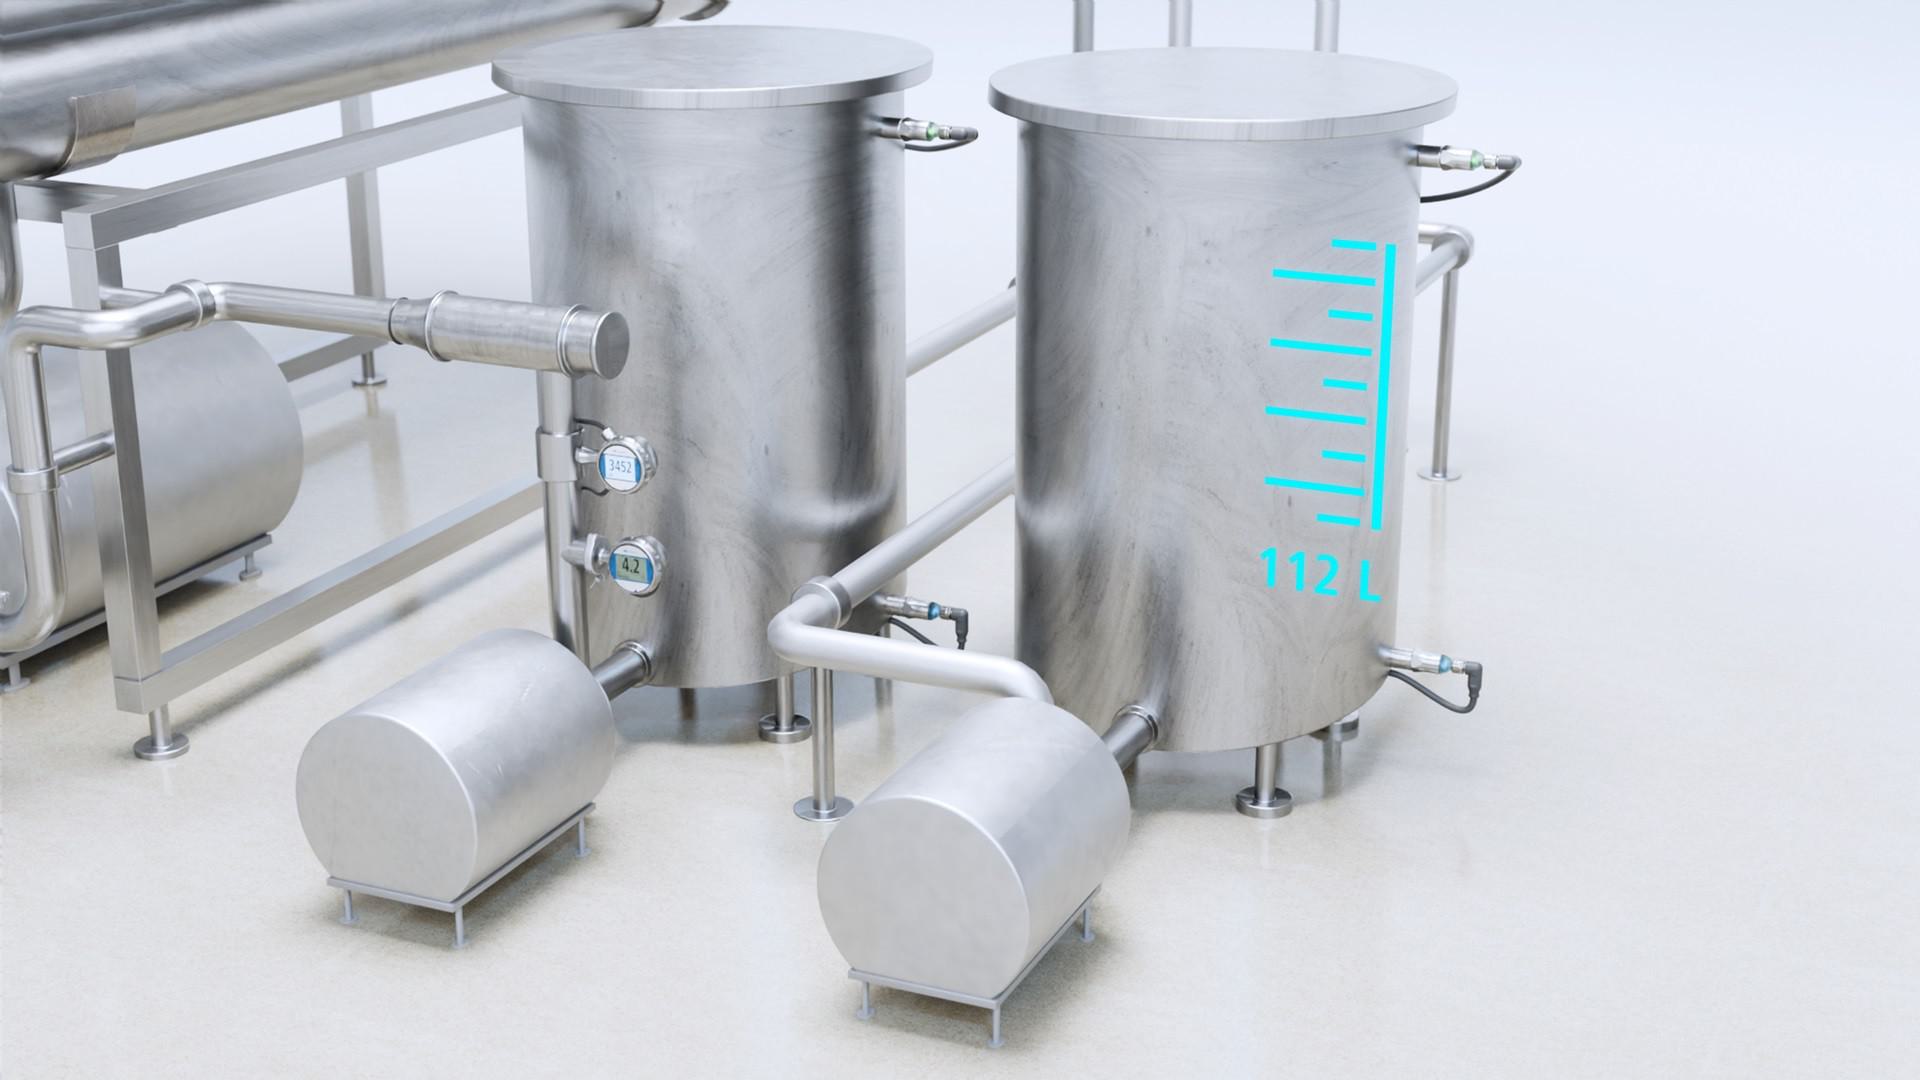
Balance tank level monitoring
Guarantee a continuous product feed for uninterrupted operation of the filtration unit and downstream processes.
- Material-independent detection of high and low limit levels along with continuous fill-level measurement
- Ability to buffer short unplanned stoppages in individual units to keep the entire line running uninterrupted
- Overflow and dry-running protection to minimize product losses and prevent equipment damage
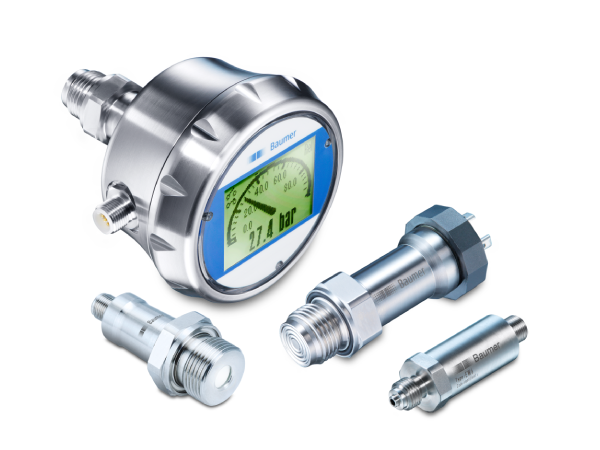
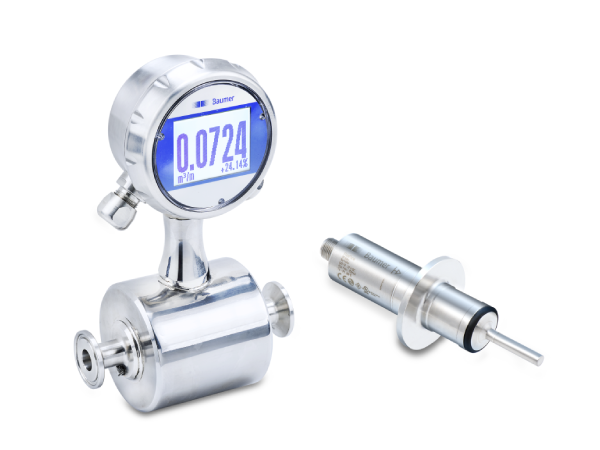
Customized mechanical instrumentation for the process industry
Since 1849, Bourdon has offered custom-built solutions for reliable pressure and temperature measurement. All products are manufactured to the highest quality and safety requirements, drawing on our expertise in the railway market and its applications. Bourdon also has a worldwide presence for better service.
Baumer sensors are certified in compliance with all international design and material standards relevant to the food and beverage industry. Internal processes at Baumer comply with DIN ISO 9000 requirements and are certified accordingly. Hygienic sensors are designed, developed and manufactured in compliance with 3-A and EHEDG guidelines to guarantee the highest standards in food production.
An end-to-end development process, from the initial concept phase through to series production, is continuously validated by our customers' actual use. Sensor protection is key in this context: sensors comply with IP69 protection class and undergo additional testing according to our internal proTect+ standard for maximum reliability and durability.
Learn more east
Learn more about Baumer's other food and beverage solutions
Discover our sensor solutions for heat exchange, centrifugation, extrusion, evaporation, CIP systems, dairy, brewing and beverage production.
Back to Food & Beverage SolutionsHave a Sector-Specific Question?
Our expert engineers are ready to help you identify the most suitable solution for your industry.