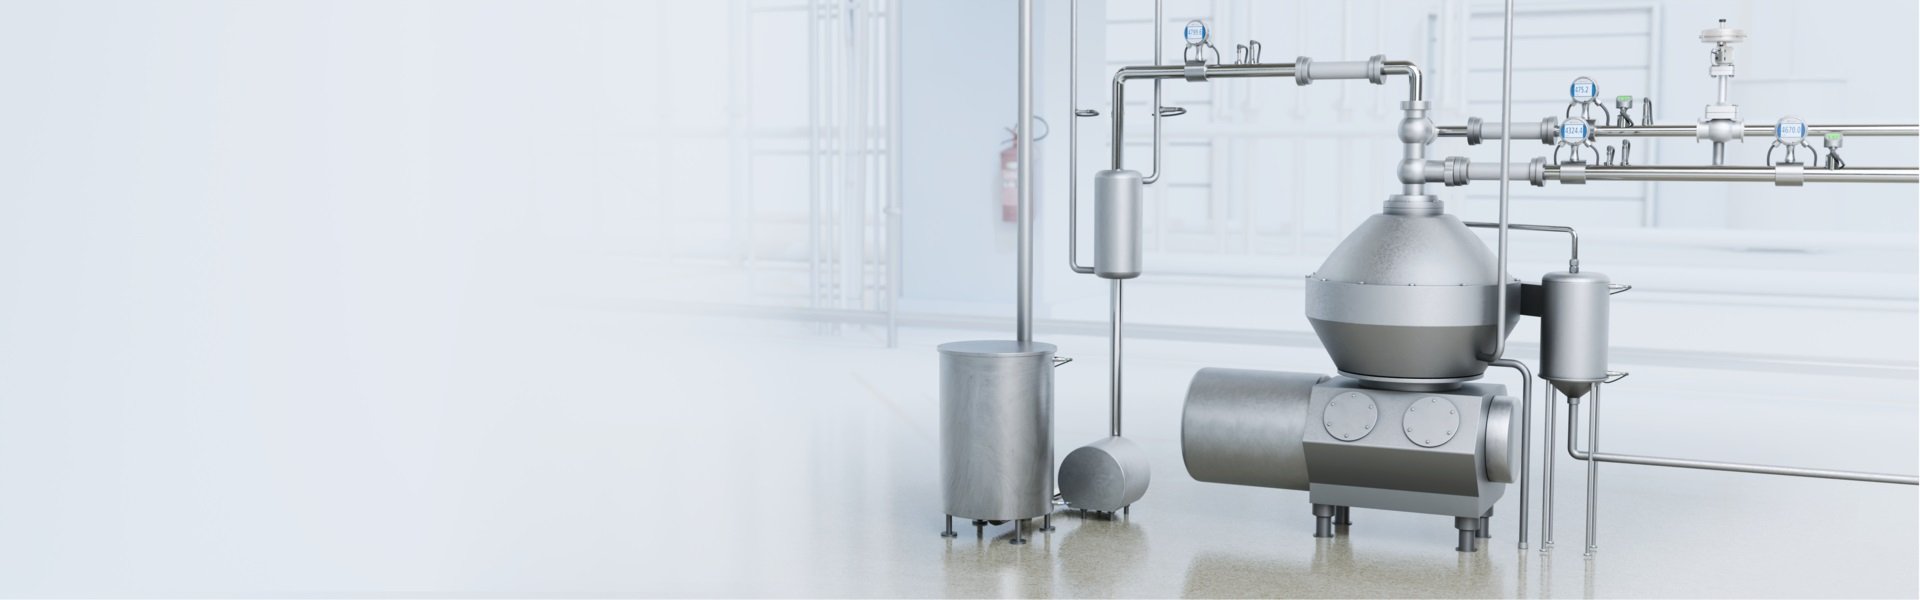
Sensor Solutions Delivering Advanced Reliability and Efficiency for Centrifugation
Precision for superior phase separation at optimum operating costs
Our technologically advanced sensor solutions provide rigorous process control throughout centrifugation, maximizing yield while ensuring the desired purity and product consistency.
Precision for superior phase separation
Our technologically advanced sensor solutions provide rigorous process control in centrifugation, maximizing yield while ensuring the desired purity and product consistency.
Decades of industry experience for safe and uninterrupted operations
Our rugged and durable hygienic sensors operate reliably in the demanding centrifugation environment and in challenging media. They ensure production continuity with minimal downtime, without compromising food safety.
Real-time data for continuous process monitoring
Fast and repeatable measurement values enable quick adjustment of process parameters and reliable detection of equipment wear, ensuring uninterrupted centrifugation, optimal separation and minimal product loss.
From feed monitoring to sludge discharge, every step of the automated centrifugation process relies on precise, reliable sensor technology. Smart sensors provide real-time data on flow, pressure, conductivity, temperature, fill level and RPM to control the centrifugation process for optimal phase separation. The centrifuge is also monitored for wear to ensure uninterrupted, safe operation.
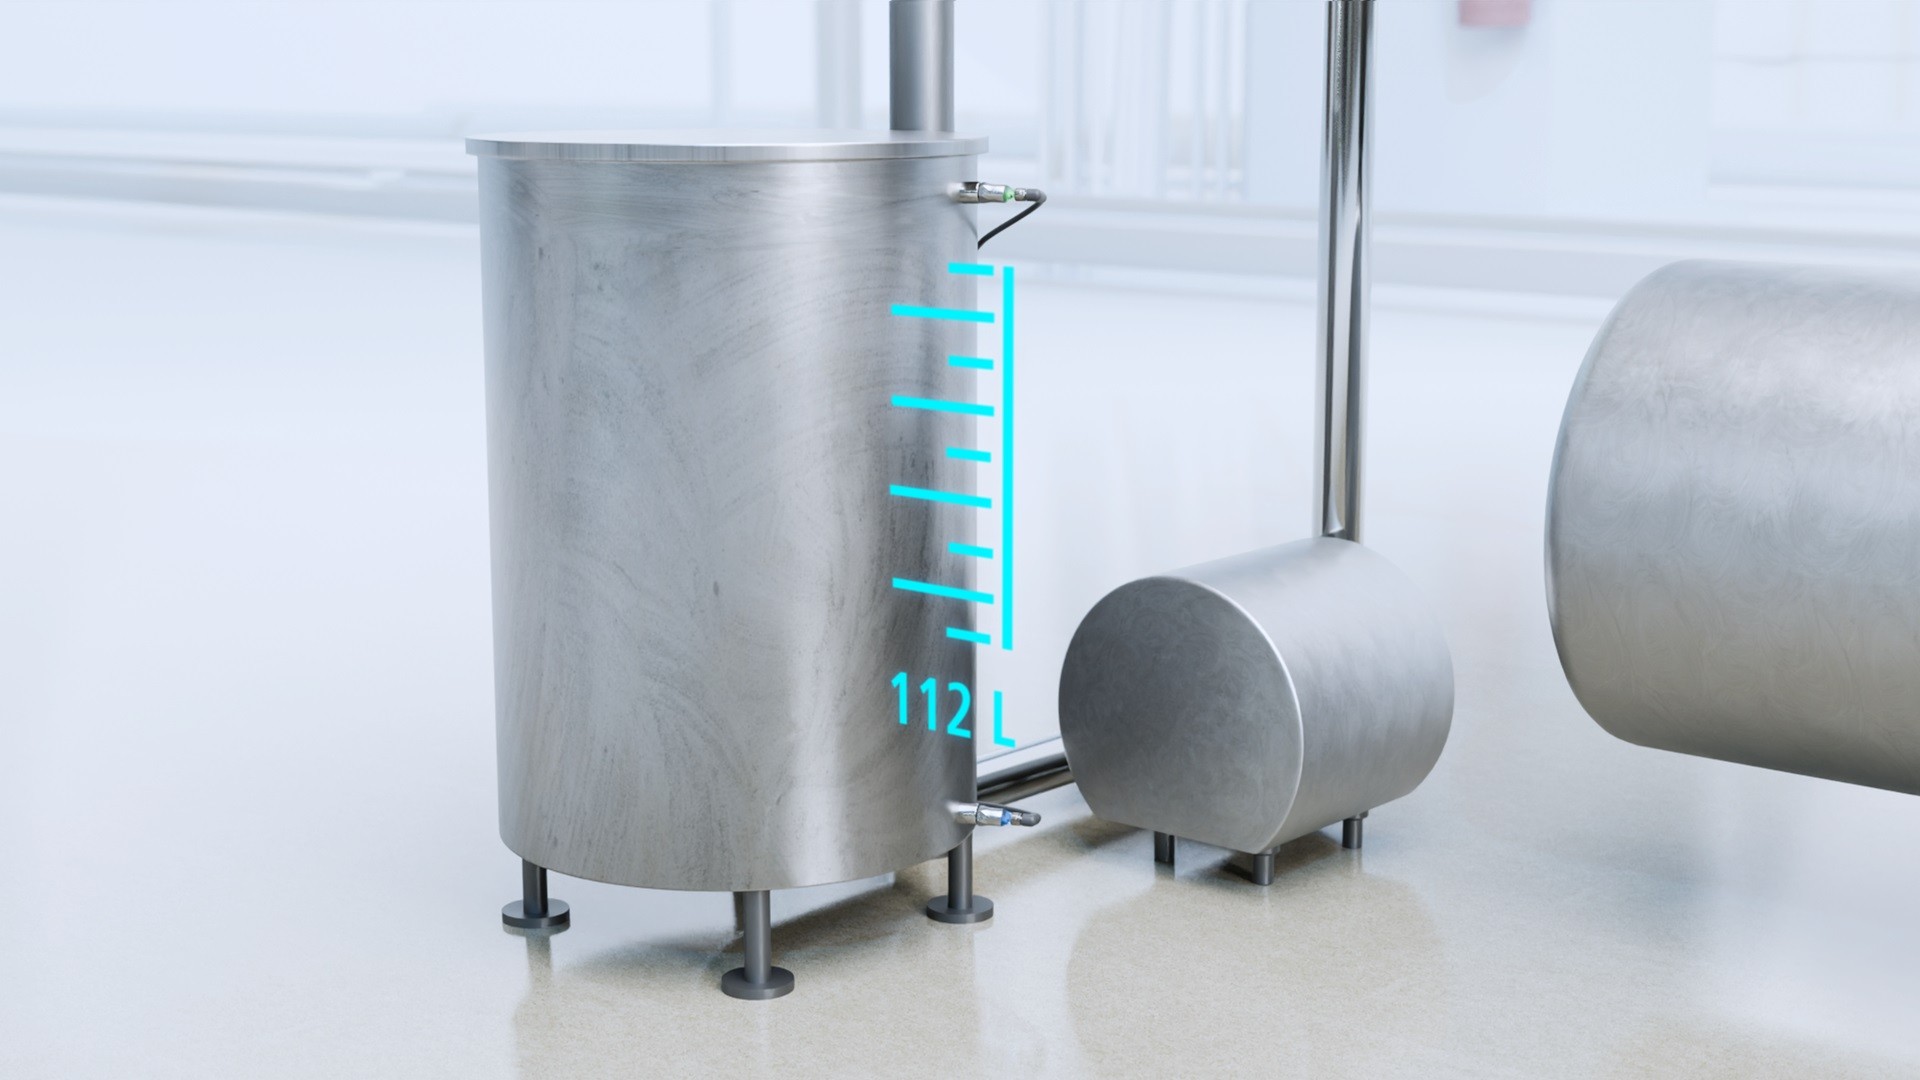
Balance tank level monitoring
Guarantee an uninterrupted product feed to keep the centrifuge running continuously.
- Material-independent detection of high and low limit levels, plus continuous fill-level measurement
- Ability to buffer brief, unplanned stoppages of individual units, guaranteeing that the entire line keeps running without interruption
- Overflow and dry-run protection to minimize product loss and prevent equipment damage
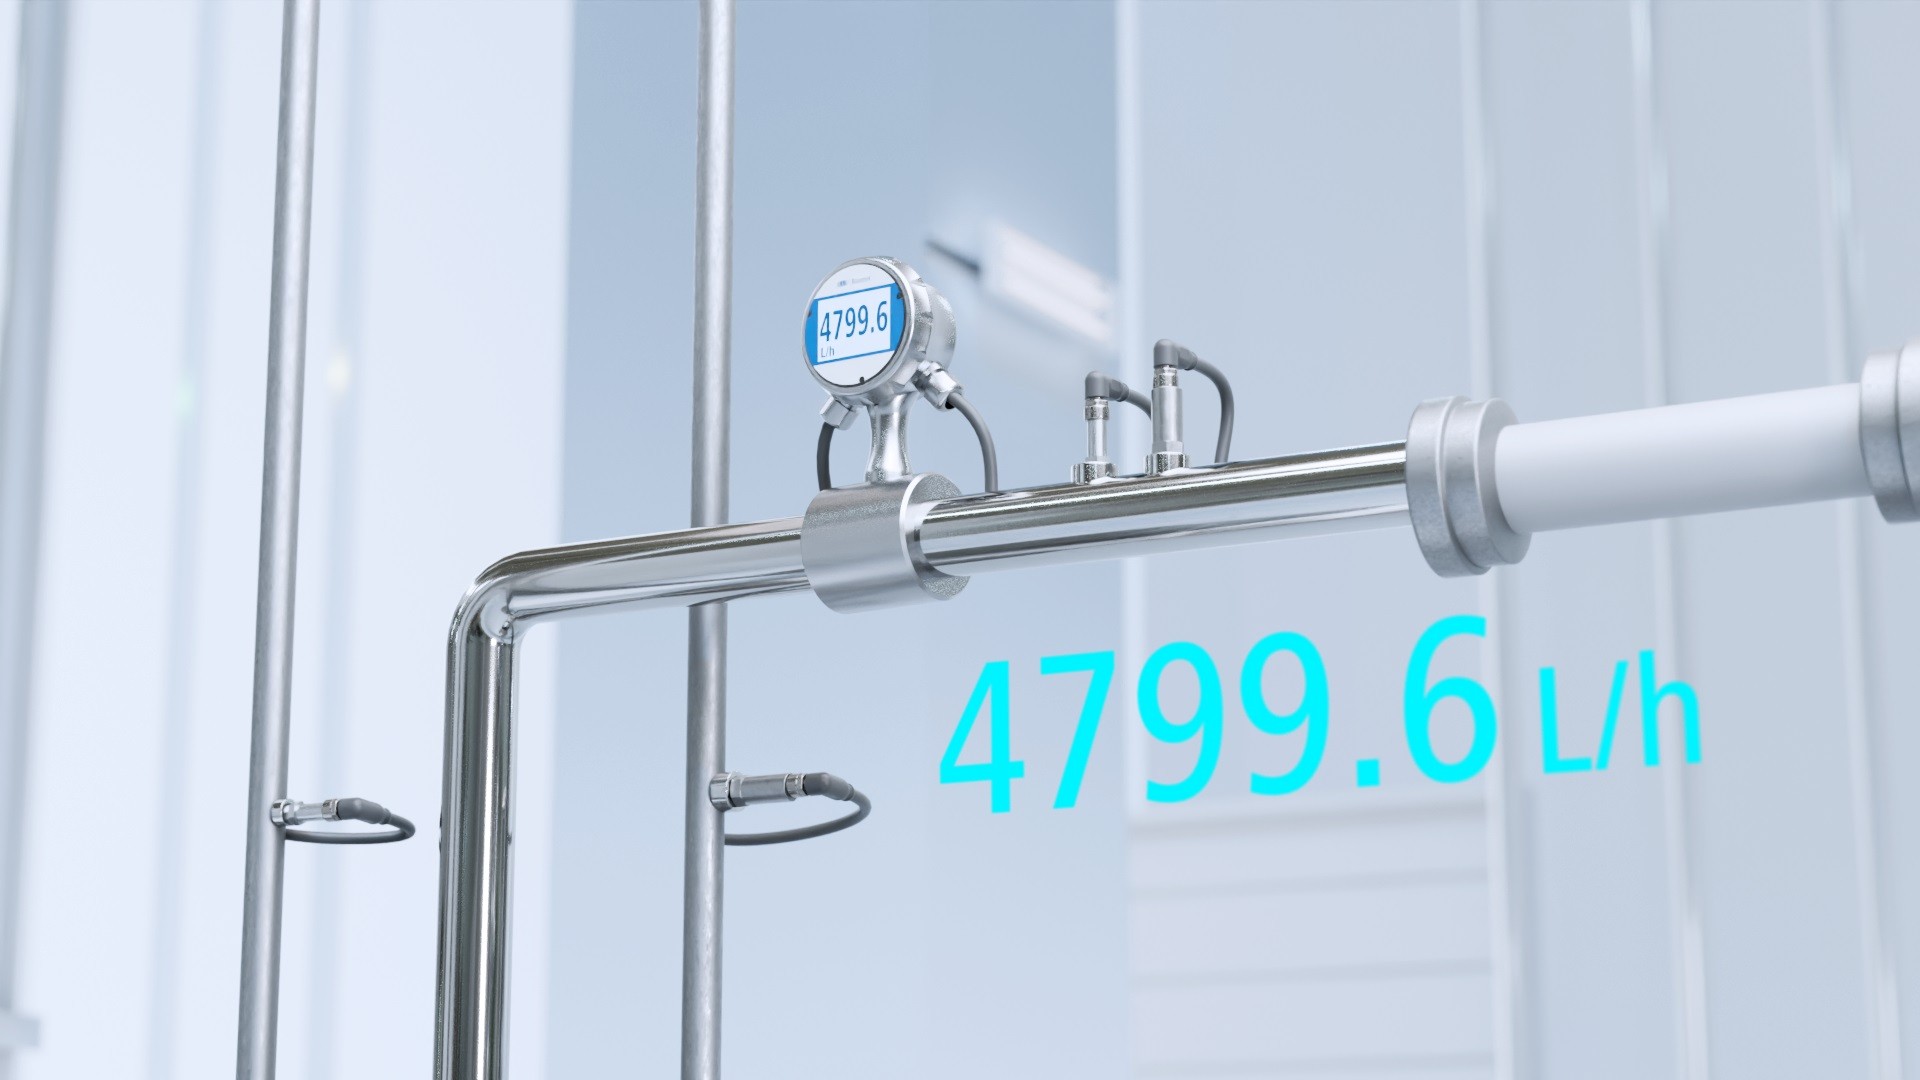
Pre-conditioning and centrifuge feed
Guarantee a consistent centrifuge feed as a prerequisite for stable phase separation.
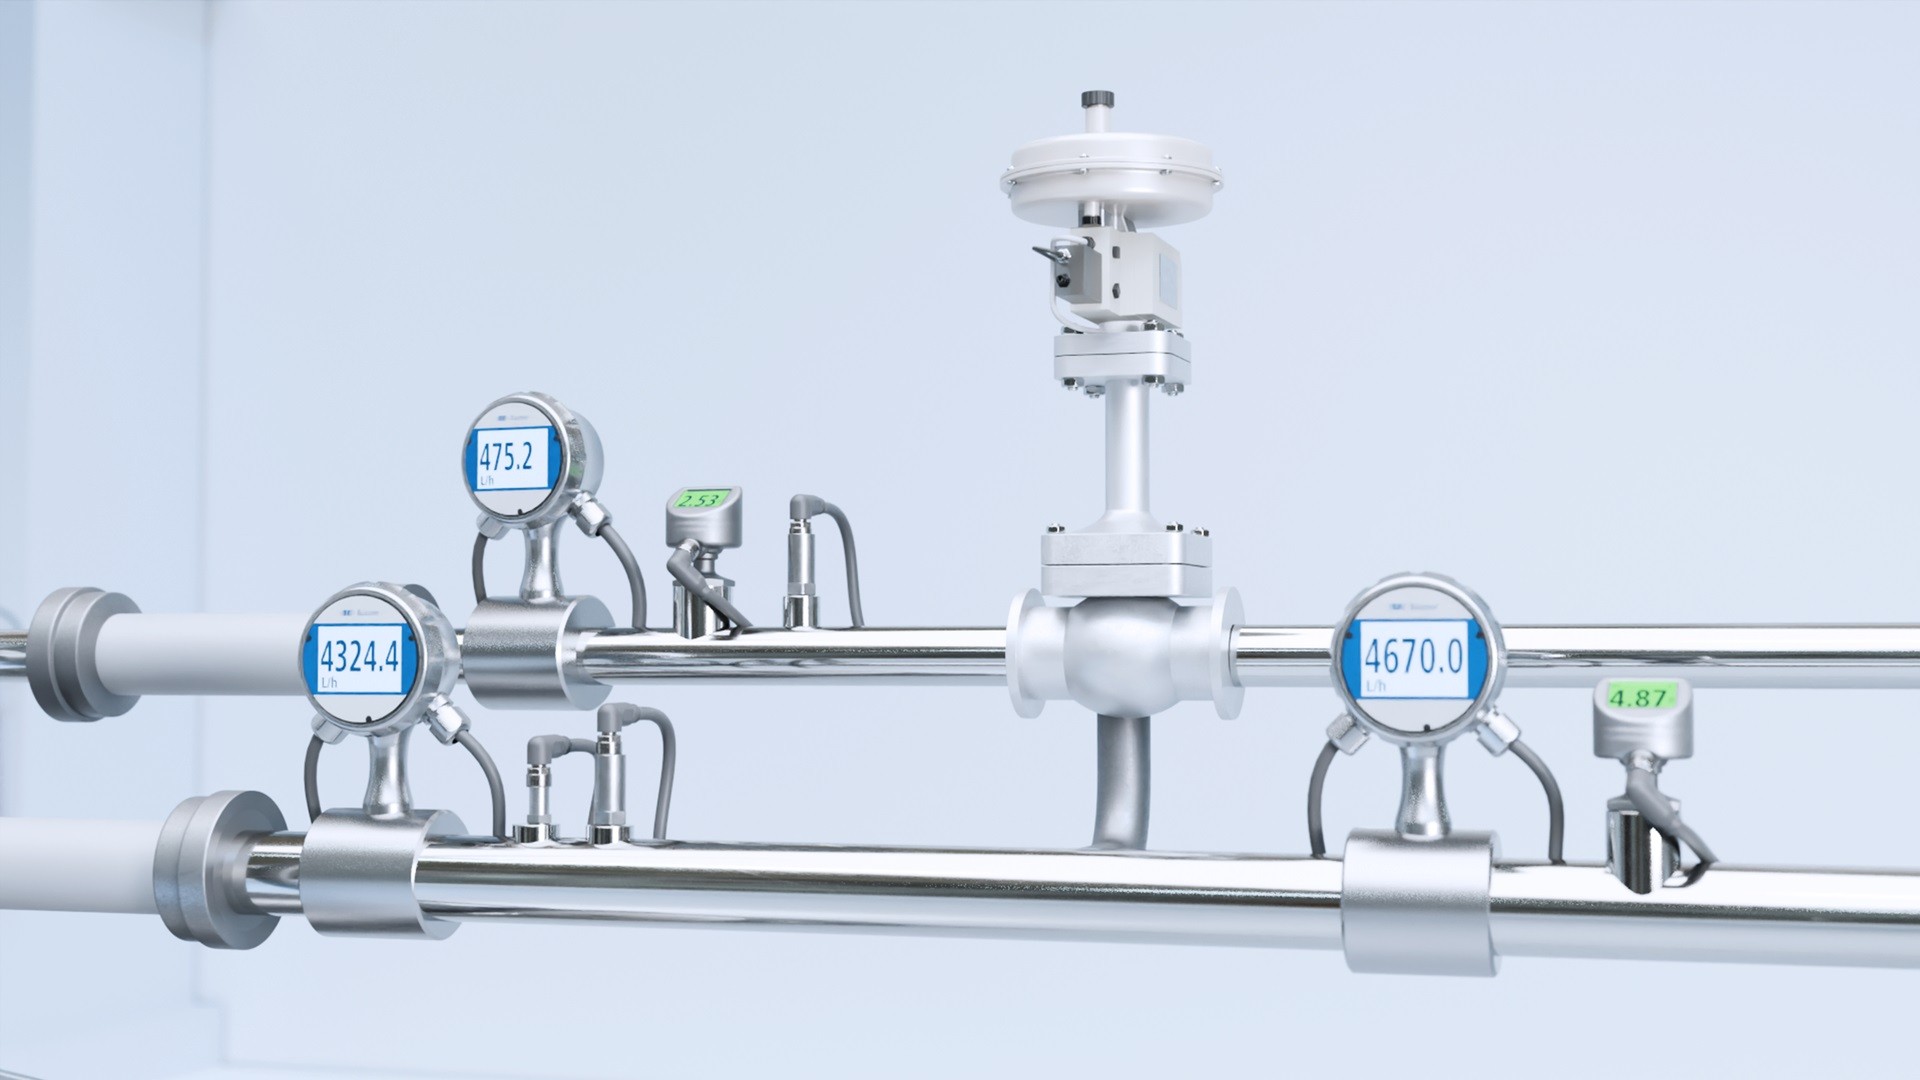
- Control of the regular product feed through flow and pressure measurement, to guarantee a constant flow rate with minimal fluctuation and maintain optimal separation conditions in the centrifuge
- Monitoring temperature to guarantee constant viscosity and other media separation properties for stable separation performance
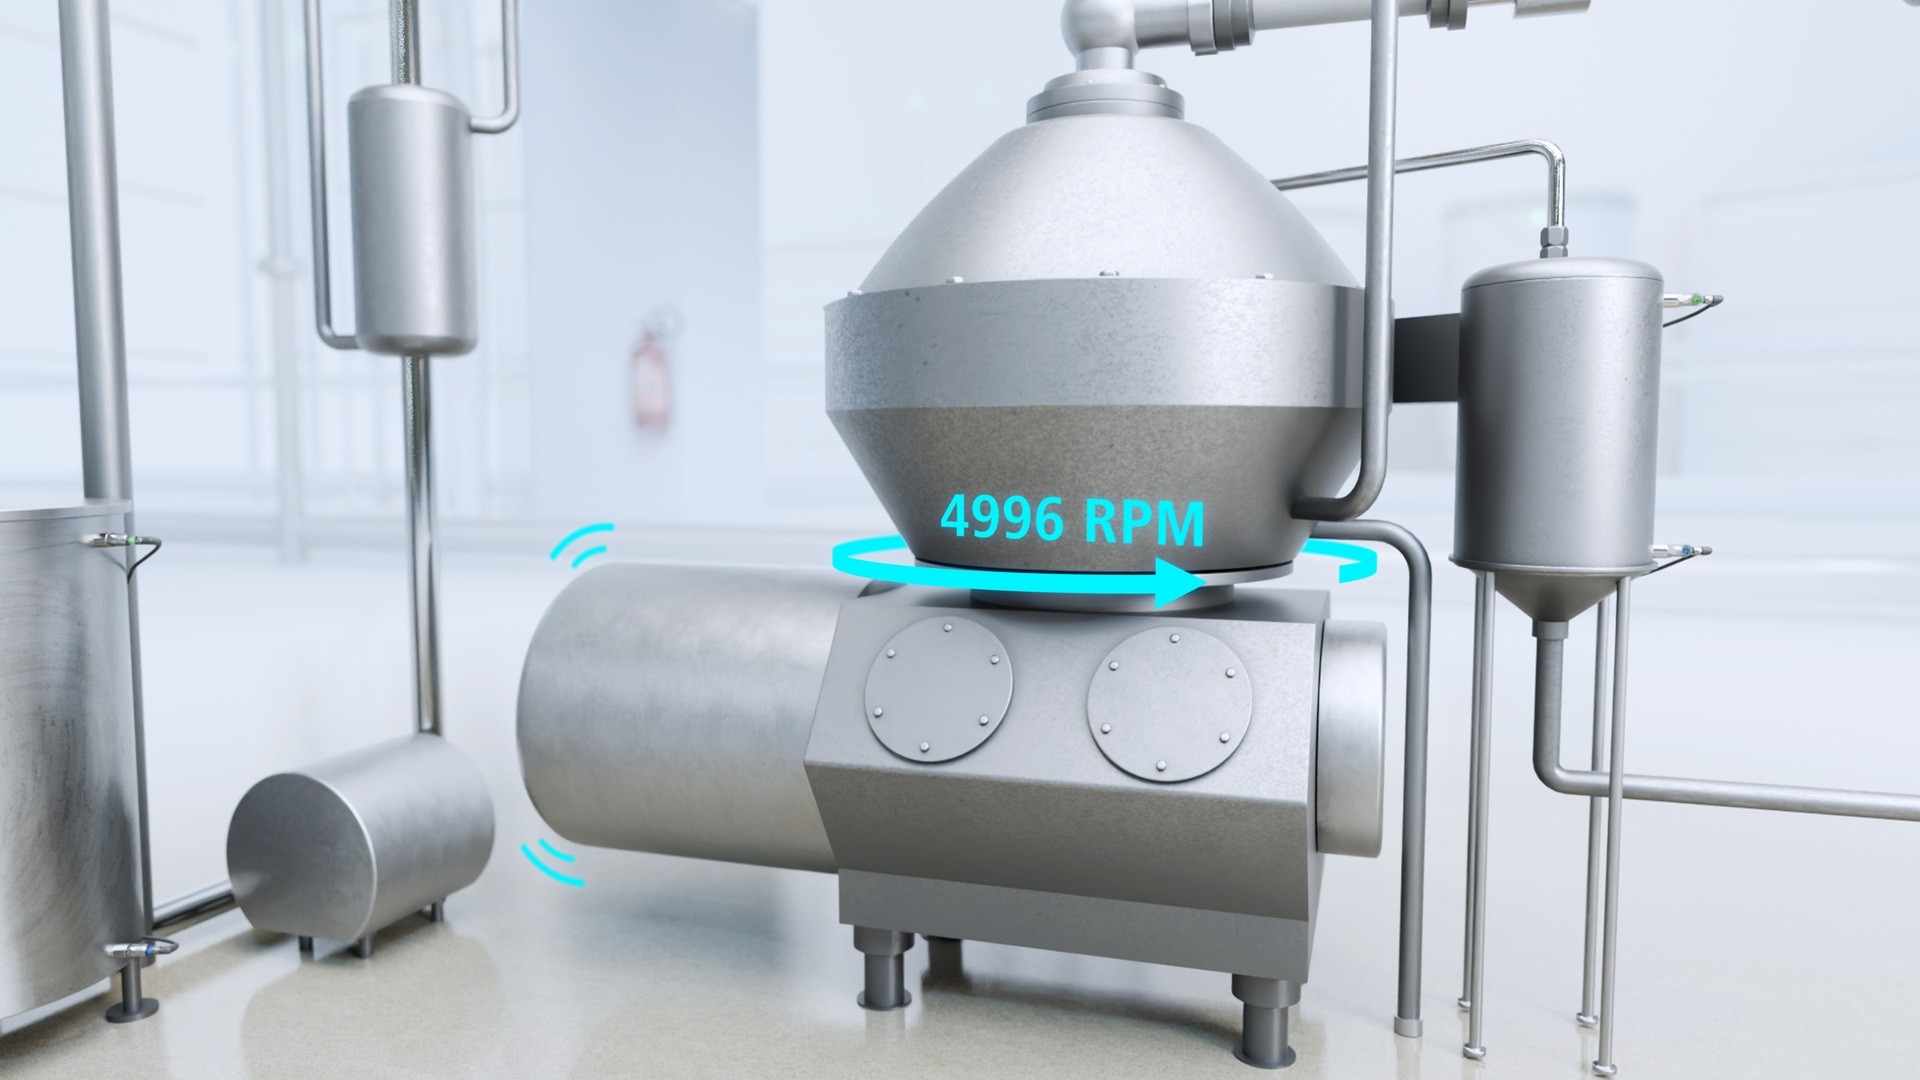
Separator speed and vibration monitoring
Ensure a sufficiently high RPM to generate the forces required for separation, while monitoring drive and separator behavior for efficient and safe operation.
- Monitoring centrifuge bowl speed using encoders on the drive motor is critical for detecting issues such as separation performance and centrifuge overflow
- Detection of vibration and mechanical imbalance with inductive distance sensors and bearingless encoders. This enables preventive maintenance to avoid unplanned downtime, improve system service life, and prevent destructive accidents that these powerful forces could cause
- Monitoring cooling with temperature sensors to prevent overheating of mechanical components
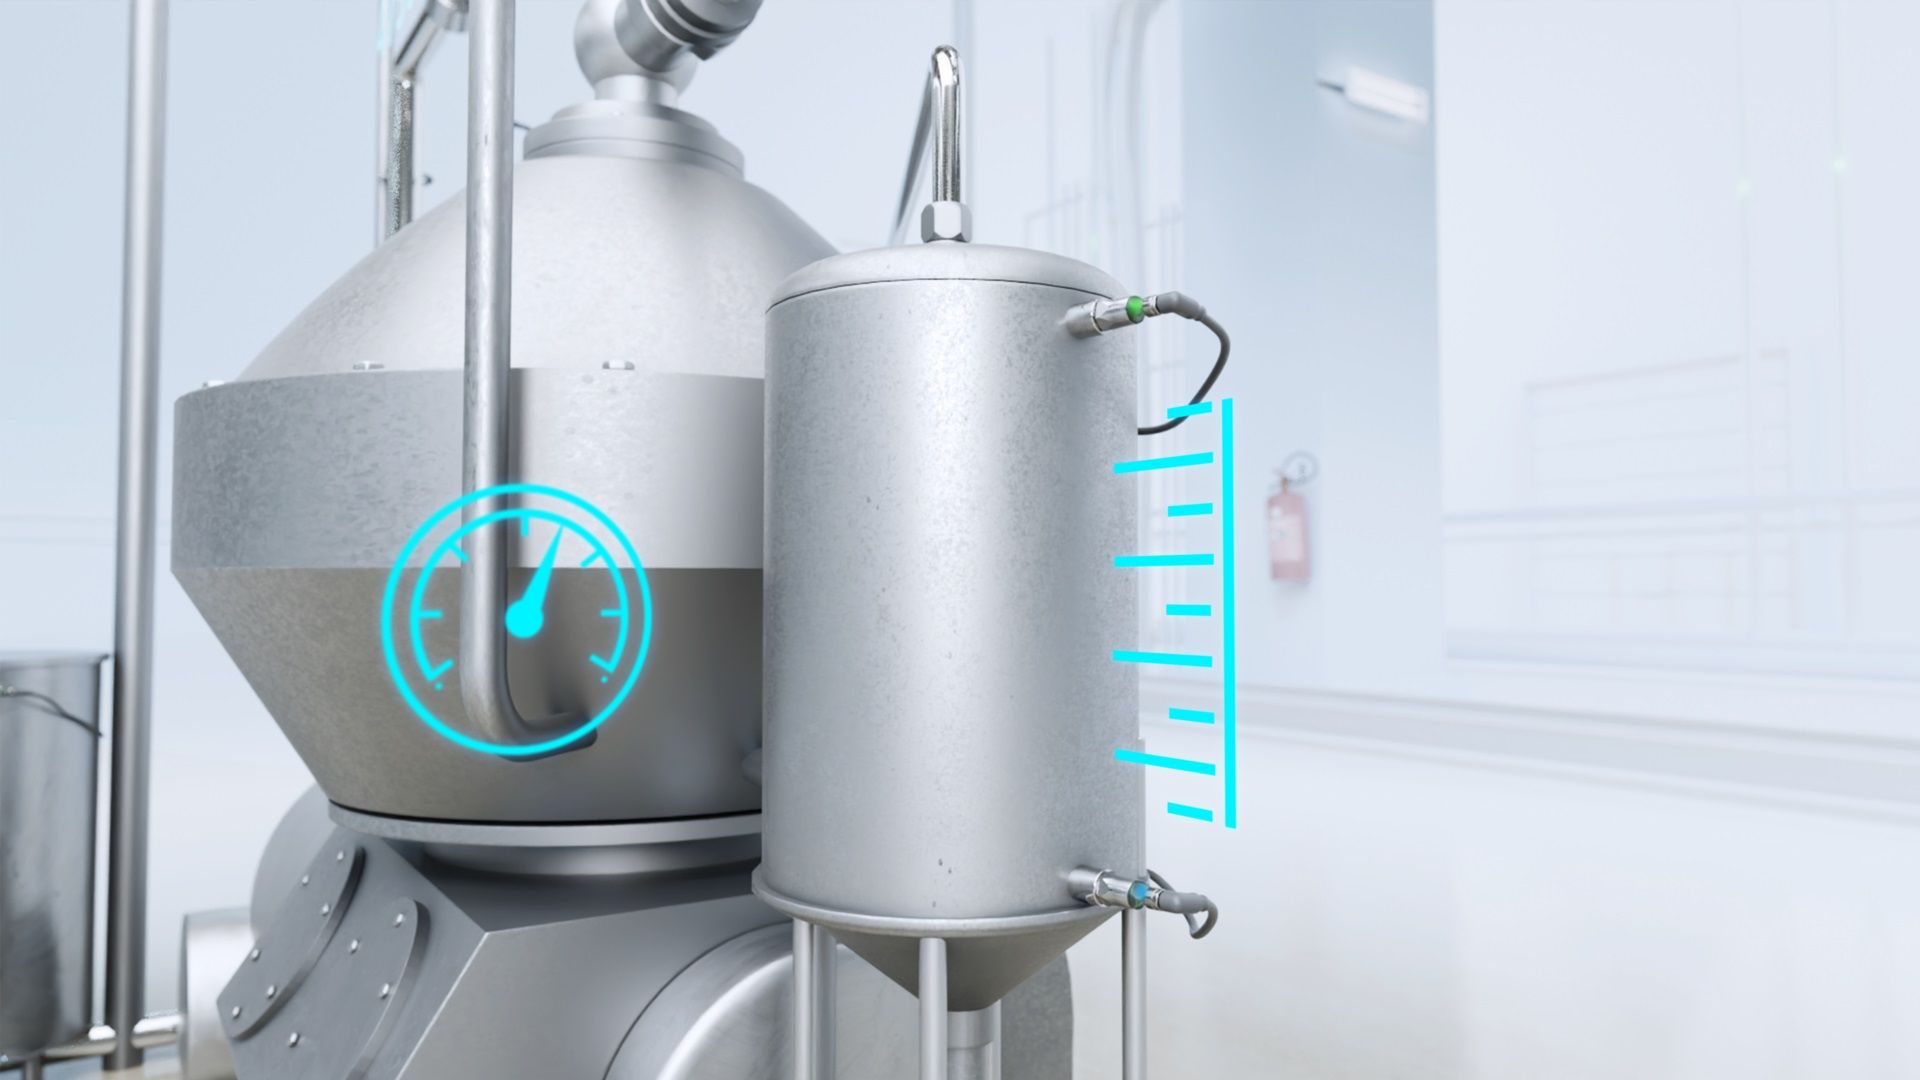
Sludge discharge monitoring
Guarantee regular sludge discharge from the centrifuge bowl to prevent issues such as declining separation performance or centrifuge overflow.
- Monitoring pressure in the process water to ensure proper operation of the hydraulically driven discharge mechanism
- Detection of high and low limit levels independent of sediment and foam, plus continuous fill-level measurement. This ensures proper sludge discharge and prevents overflow of the sludge cyclone
Separation performance monitoring and re-standardization
Guarantee the desired composition of outlet streams and specification-compliant re-standardization for consistent end-product quality.
- Control of back pressures in the light and heavy phases via pressure sensors to regulate the outlet streams and separation quality
- Measurement of outlet streams using flow sensors as a basis for mass balance and downstream re-standardization
- Monitoring composition with conductivity sensors as a factor for ensuring separation performance, controlling product quality, and re-standardization
- Measuring temperature as a correction factor for conductivity measurement, ensuring constant quality of heat-sensitive products
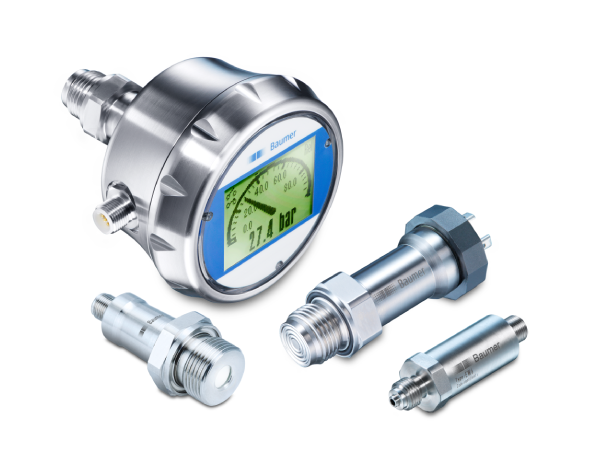
Pressure sensors
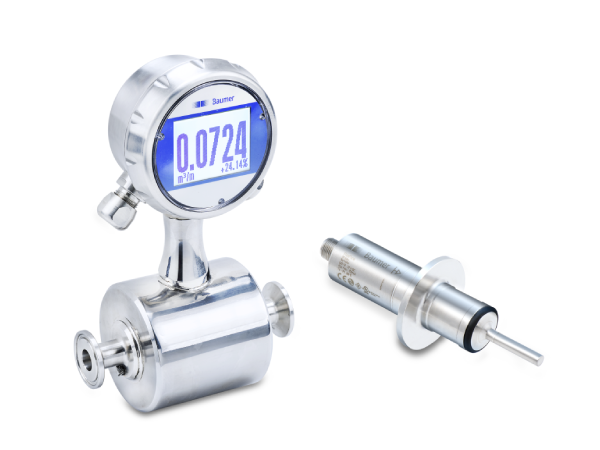
Flow sensors
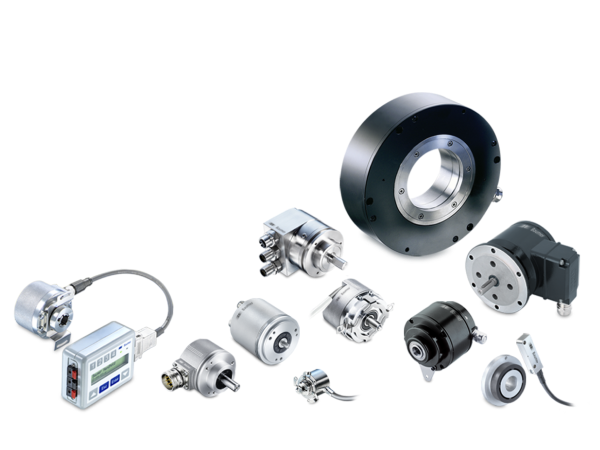
Rotary encoders / angle sensors
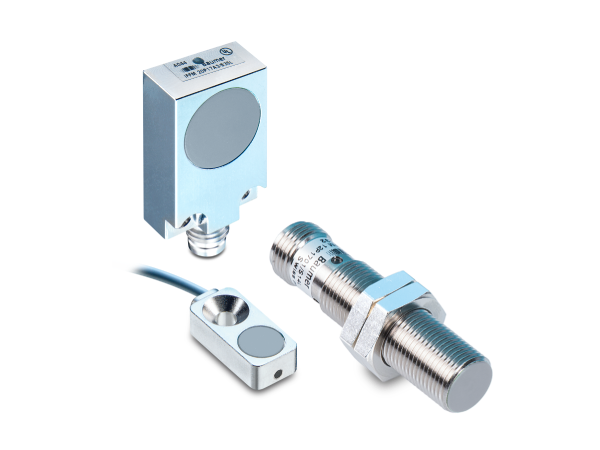
Inductive distance sensors
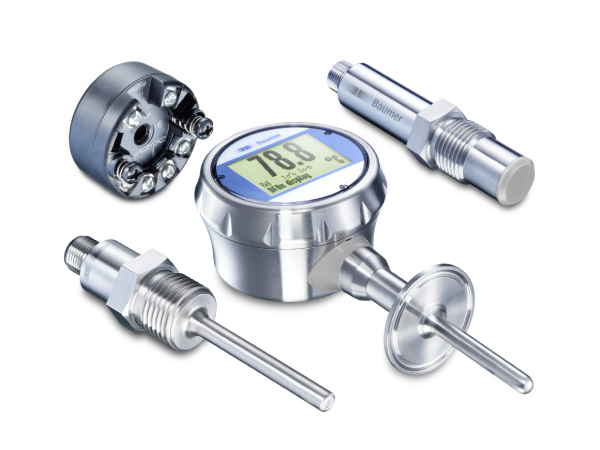
Temperature sensors
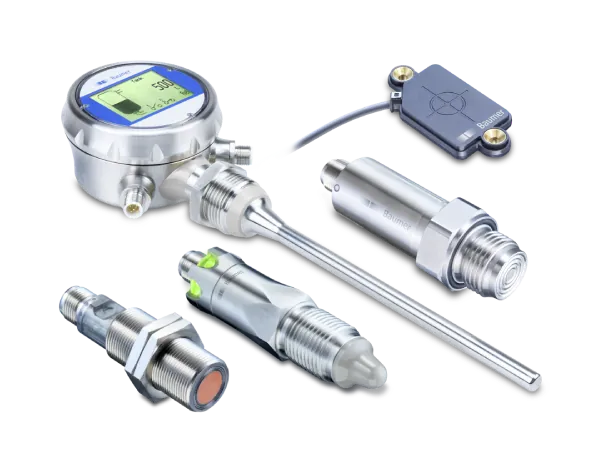
Level sensors
Customized mechanical instrumentation for the process industry
Since 1849, Bourdon has offered dedicated solutions for reliable pressure and temperature measurement. All products are manufactured to meet the highest quality and safety requirements, backed by our expertise in the railway market and its applications. Bourdon also has a worldwide presence for better service.
Discover Bourdon products
Baumer sensors are certified in compliance with all international design and material standards relevant to the food and beverage industry. Internal processes at Baumer comply with DIN ISO 9000 requirements and are certified accordingly. Hygienic sensors are designed, developed and manufactured in compliance with 3-A and EHEDG guidelines to guarantee the highest standards in food production.
End-to-end development, from the initial concept phase through to series production, is continuously validated through our customers' actual use. Sensors comply with IP68/IP69K protection ratings and are additionally tested according to our in-house proTect+ standard to guarantee maximum reliability and durability.
Learn moreHave questions?
Our experts will be happy to answer any questions and provide further information. Just send us an email.