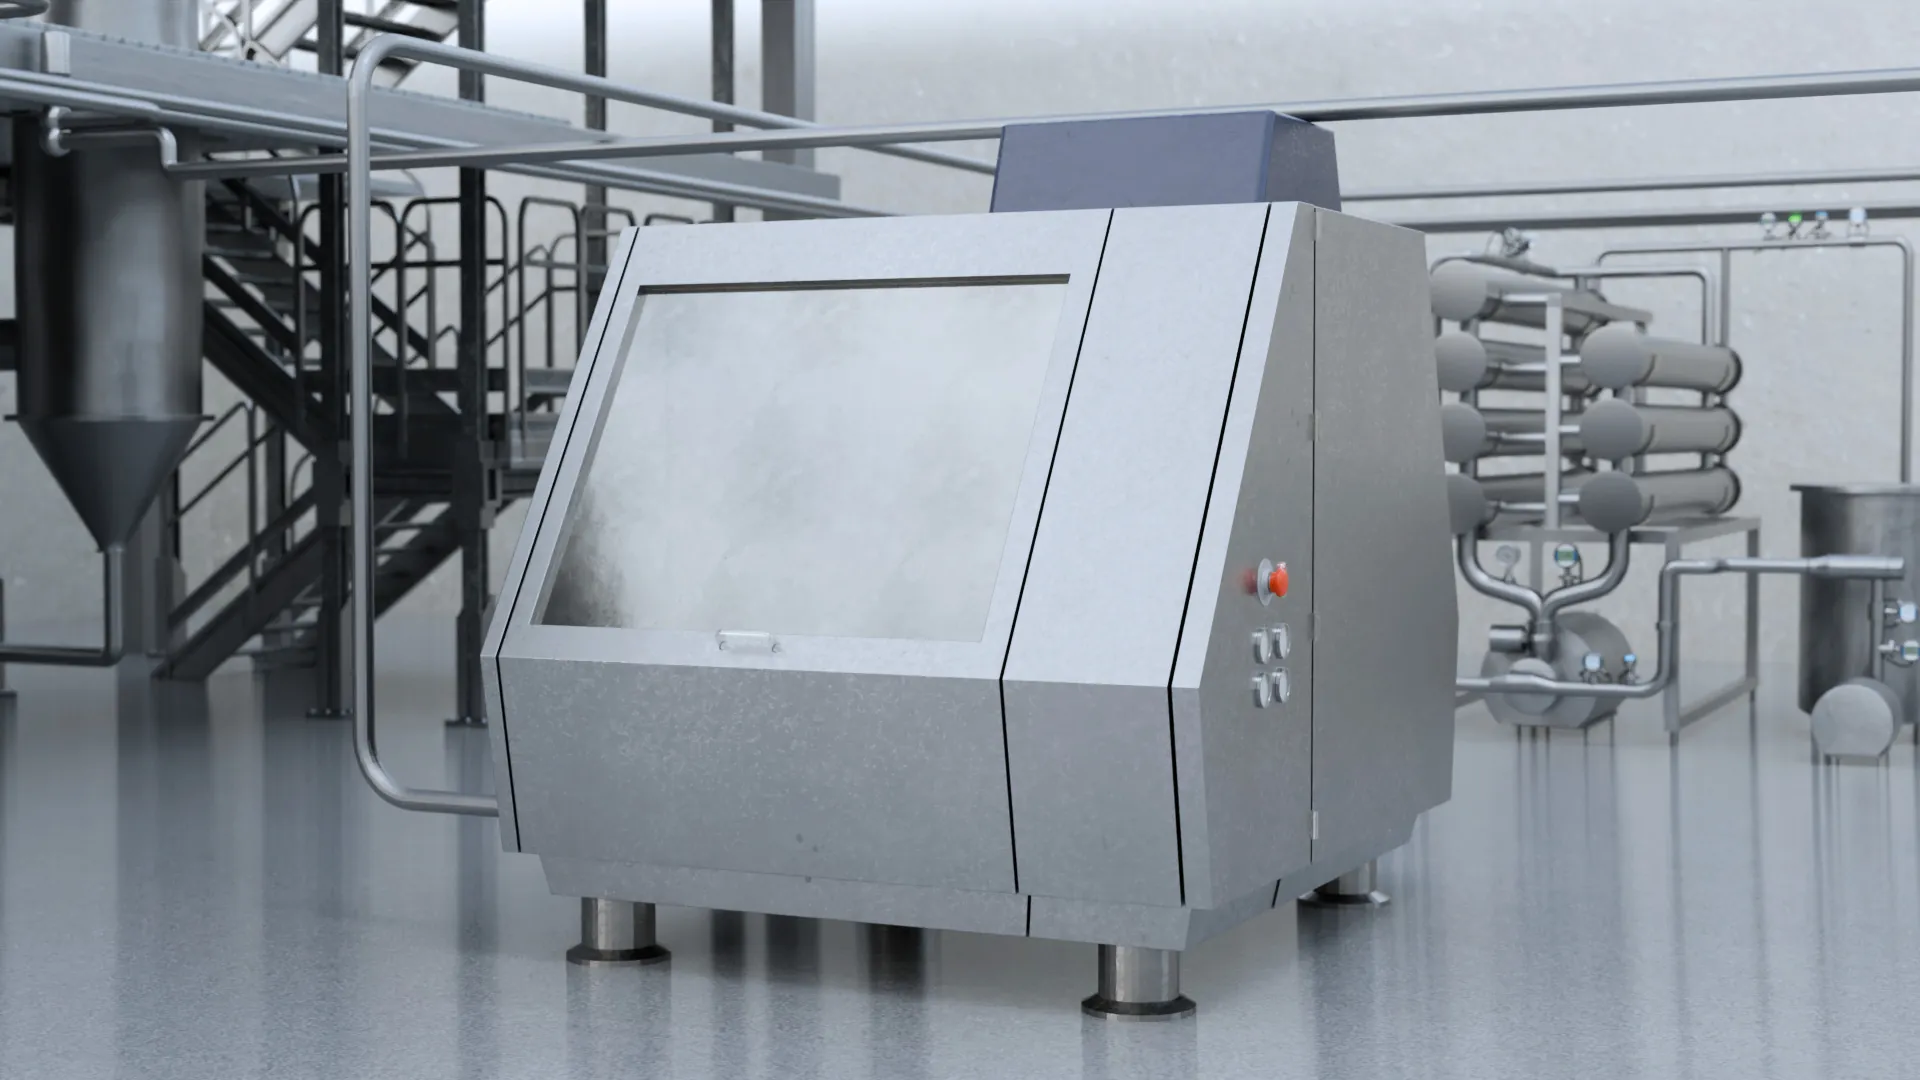
Sensor solutions for stable process control in homogenization
Precise pressure, flow and temperature control for consistent product quality
In dairy products, beverages and other food products, fat stabilization is achieved by breaking down droplets and distributing them evenly throughout the product using a homogenizer. Stable, efficient operation requires tight control of pressure, flow and product temperature.
Precision for stable pressure
We ensure precise measurement of high pressure at the homogenizer inlet and outlet for effective breakdown of fat globules and a consistent product texture.
Proven durability for demanding environments
Our robust, hygienic sensors operate reliably under the high-pressure, high-vibration conditions of homogenization, ensuring minimum downtime.
Real-time data for continuous process monitoring
Fast, repeatable measurement values allow process parameters to be adjusted instantly, ensuring uninterrupted homogenization and consistent product quality.
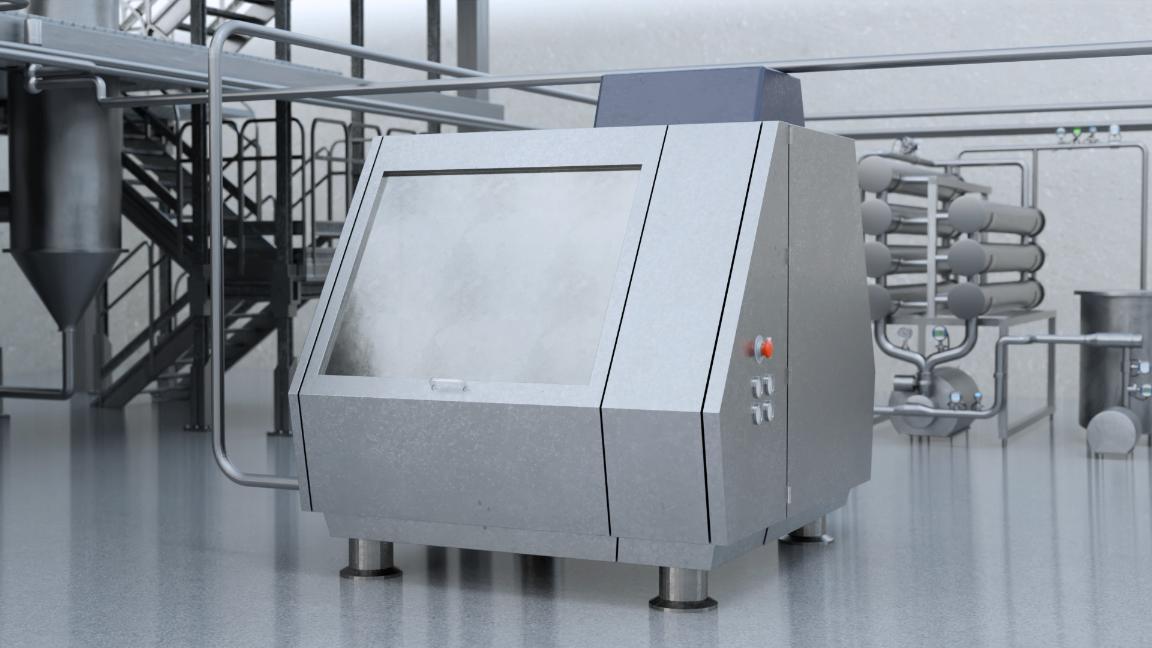
Homogenizer monitoring
Product passed through a high-pressure homogenizer requires precise, repeatable process conditions to break down fat droplets and distribute them evenly throughout the volume. This relies on three critical measurement tasks:
-
compress
Homogenization pressure — Precise monitoring of high pressure at the homogenizer inlet and outlet is required for effective breakdown of fat globules and a consistent product texture.
-
water
Flow rate — Continuous monitoring of flow rate is required to ensure a stable product feed and even distribution at the homogenization head.
-
thermostat
Product temperature — Precise measurement and control of product temperature is required to maintain proper fat fluidity and maximize homogenization efficiency.
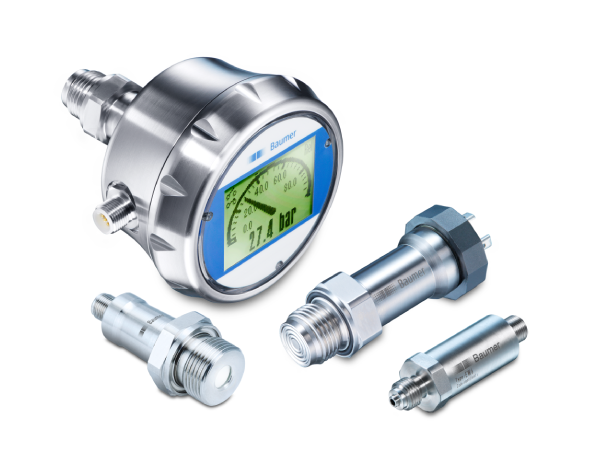
Pressure sensors
Open in product selector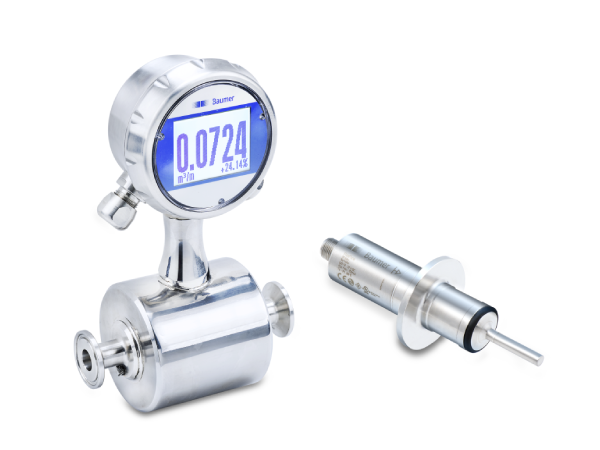
Flow sensors
Open in product selector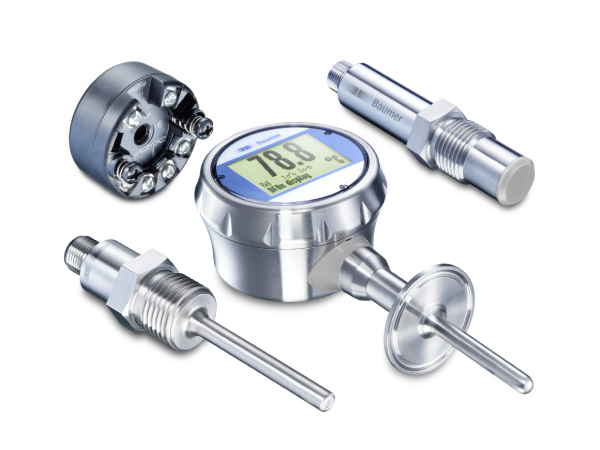
Temperature sensors
Open in product selector
Customized mechanical instrumentation for the process industry
Since 1849, Bourdon has offered dedicated solutions for reliable pressure and temperature measurement. All products are manufactured to meet the highest quality and safety requirements. Bourdon also has a worldwide presence for better service.
Discover Bourdon products
Baumer sensors are certified in compliance with all international design and material standards relevant to the food and beverage industry. Internal processes at Baumer comply with DIN ISO 9000 requirements and are certified accordingly. Hygienic sensors are designed, developed and manufactured in compliance with 3-A and EHEDG guidelines to ensure the highest standards in food production.
An end-to-end development process, from the initial concept phase through to series production, is continuously validated by our customers' actual use. Sensors comply with IP68/IP69K protection class and are additionally tested according to the proTect+ standard to guarantee maximum reliability and durability.
Learn moreDiscover our other sensor solutions for the dairy industry
Discover our sensor solutions for evaporation, heat exchange, centrifugation, filtration and CIP cleaning systems.
Back to Dairy IndustryHave questions?
Our experts are happy to answer all your questions and provide further information. Just send us an email.