Sensors for the Dairy Industry — Precise, Proven, Smart
Smart sensor solutions from raw material intake to final product shipment
Experience and expertise growing over generations in the dairy industry
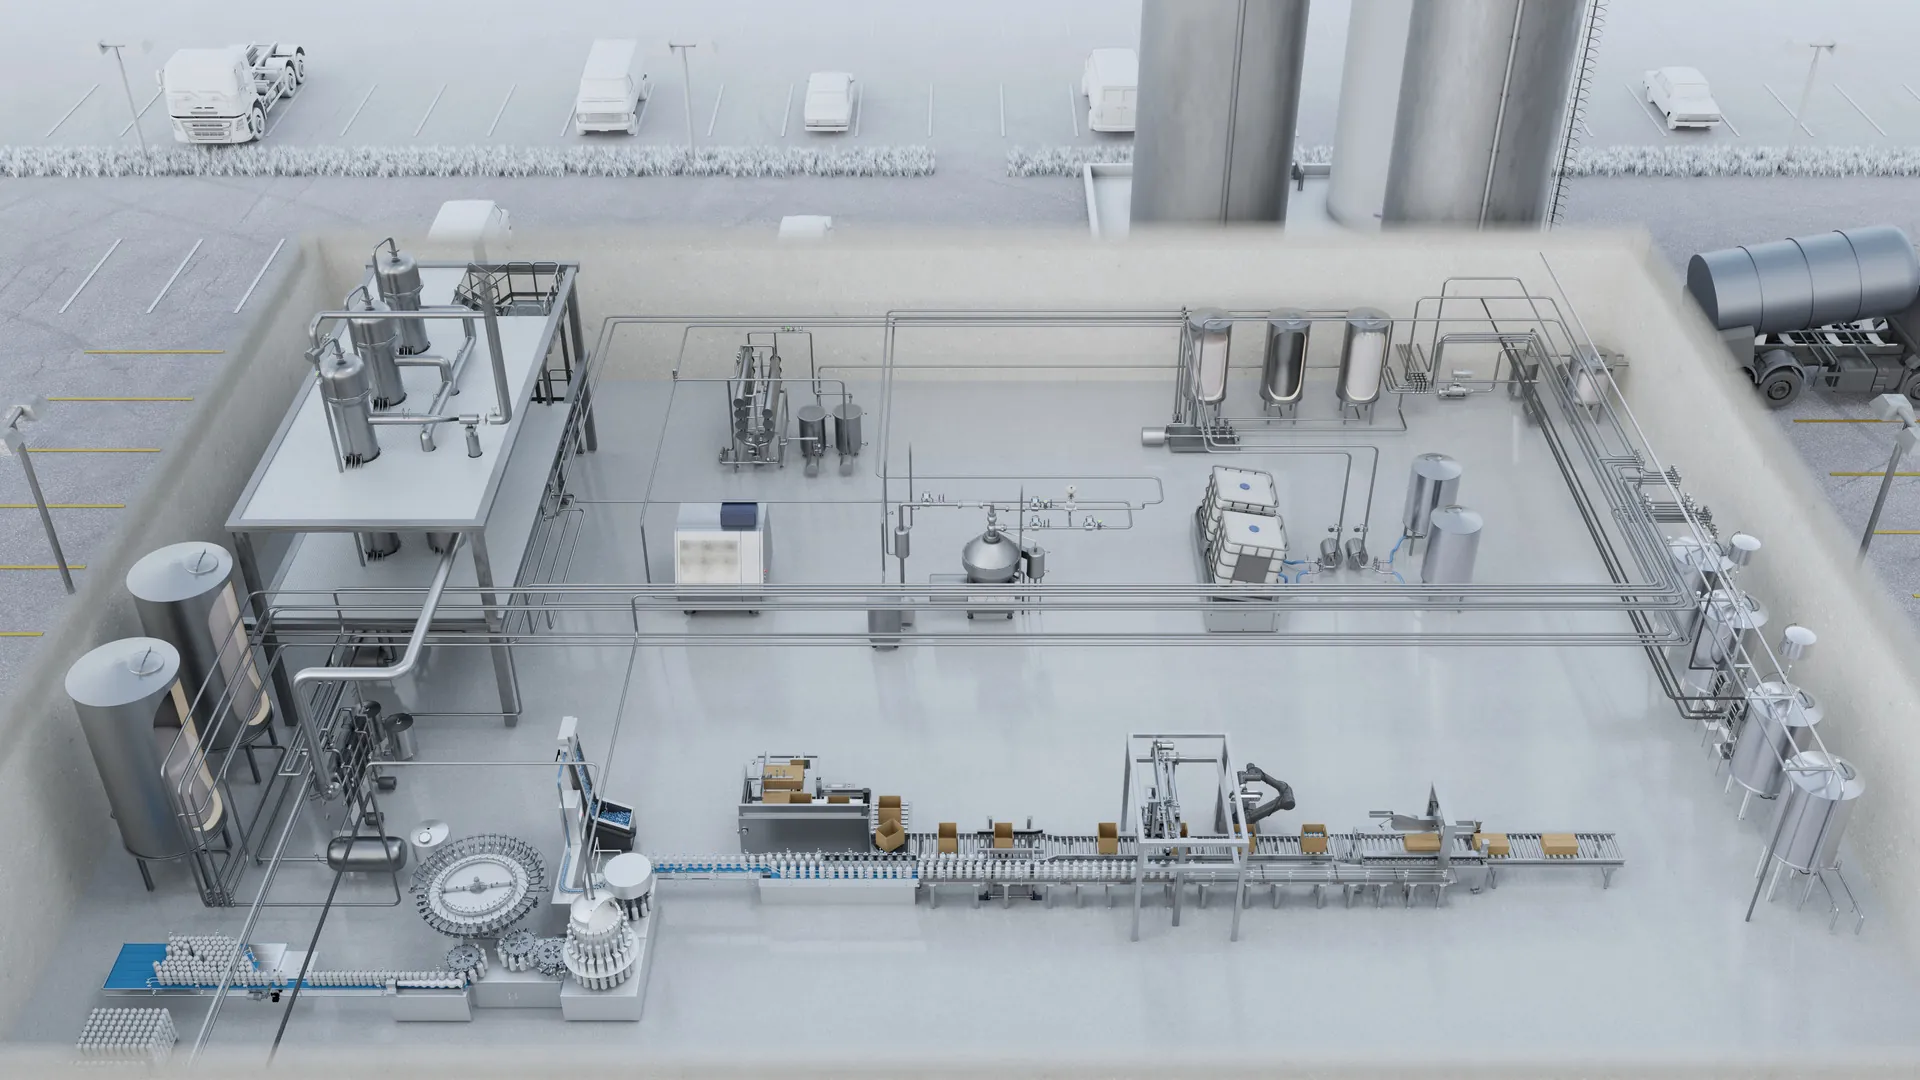
For over 40 years, Baumer has been a sensor partner to local and global dairy companies. Our hygienic sensor solutions, designed for precision and durability, operate reliably in the demanding environment of the dairy industry. Countless practical examples show measurable improvements in efficiency and process reliability, alongside the highest product quality and food safety. By giving you precise insight into the actual condition of your machinery across the value chain, we let you focus entirely on your products.
Evaporation
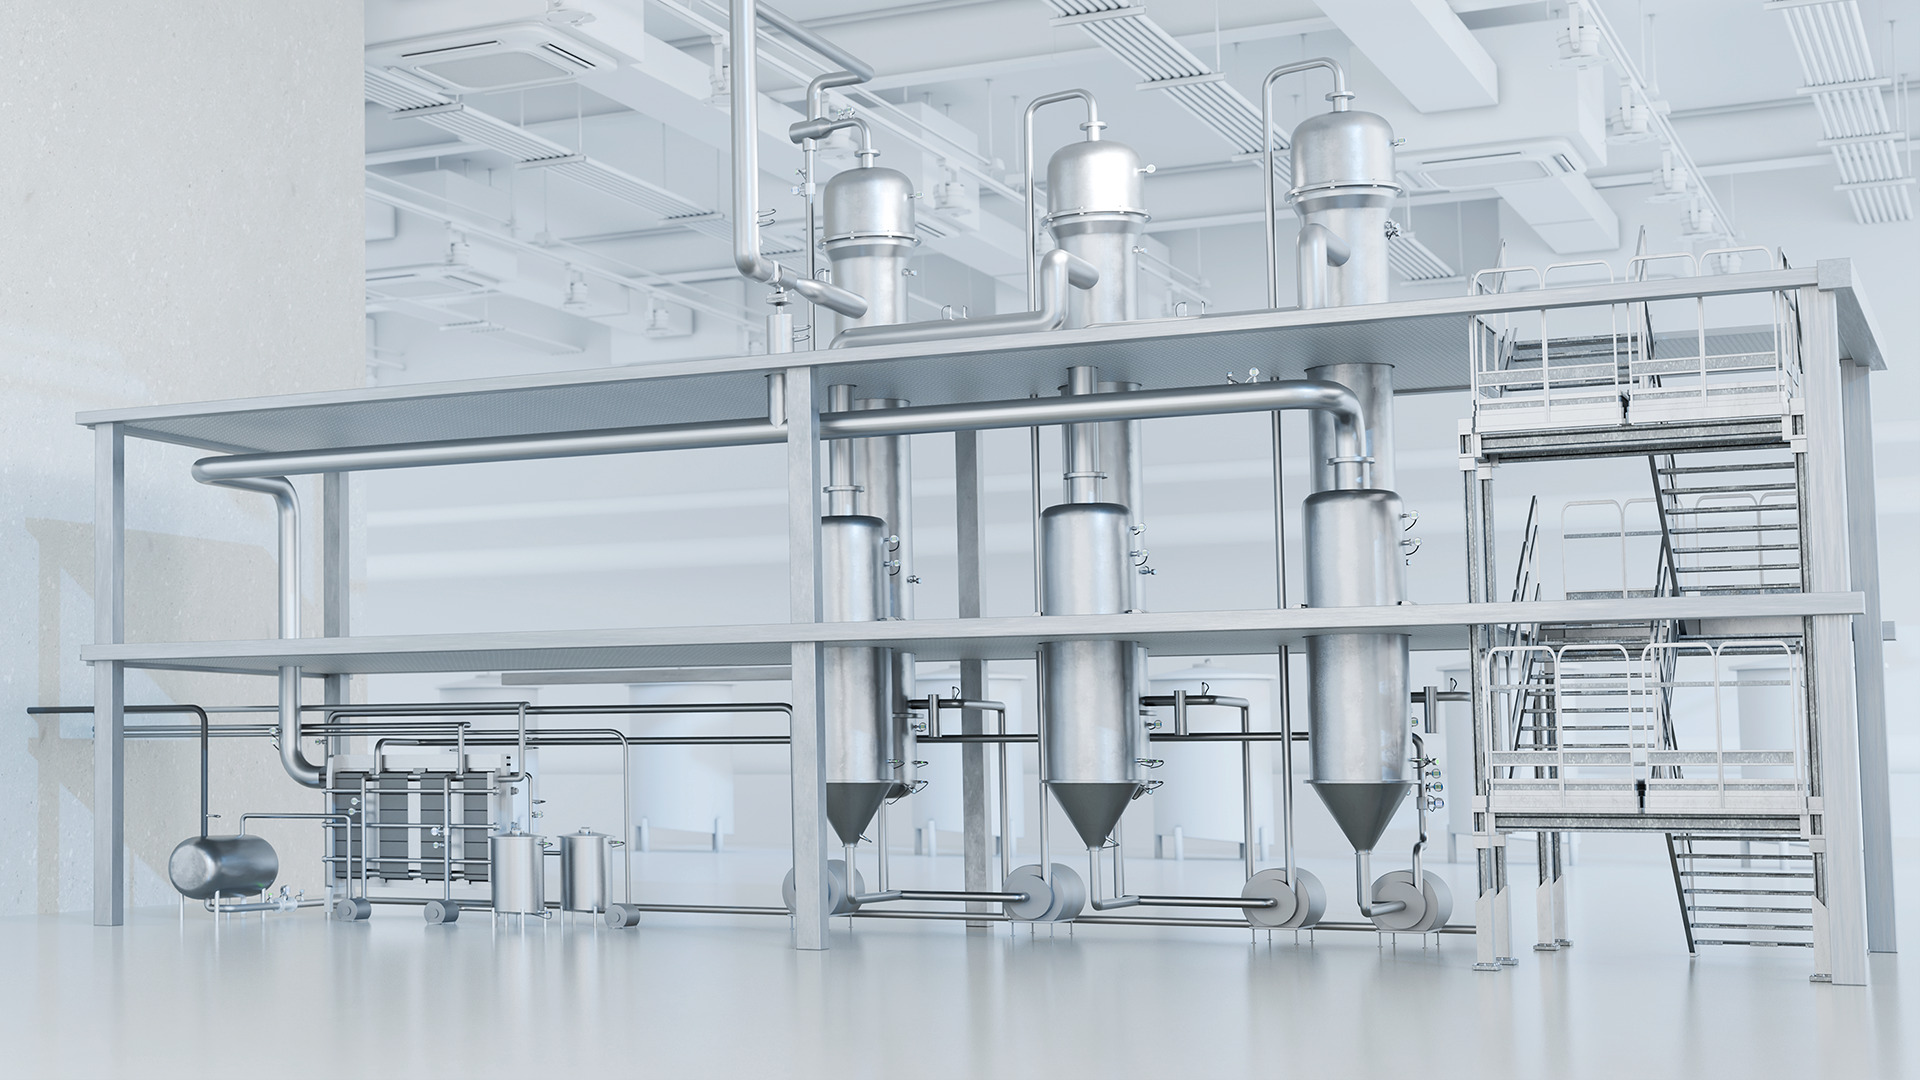
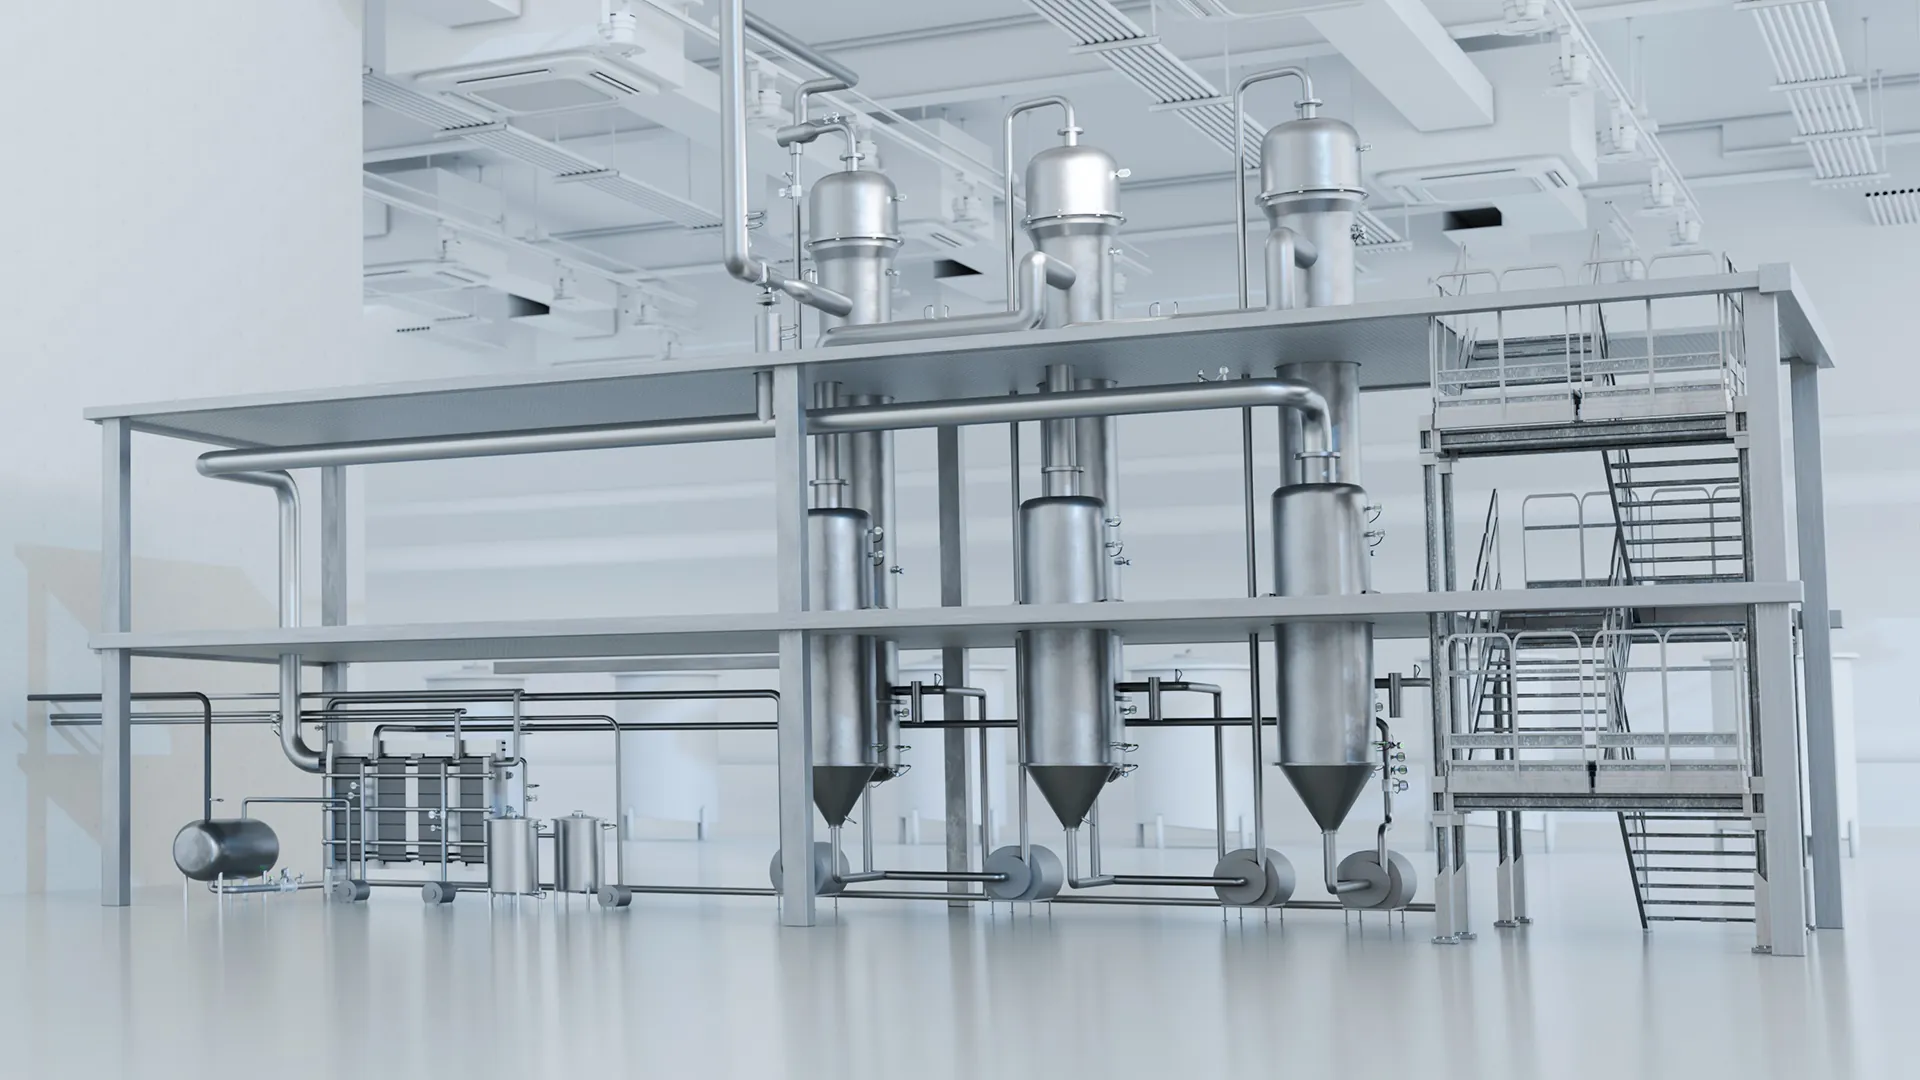
Achieving precise concentration, process stability, maximum steam economy and product quality requires precise monitoring of temperature, vacuum, flow rate and total solids content.
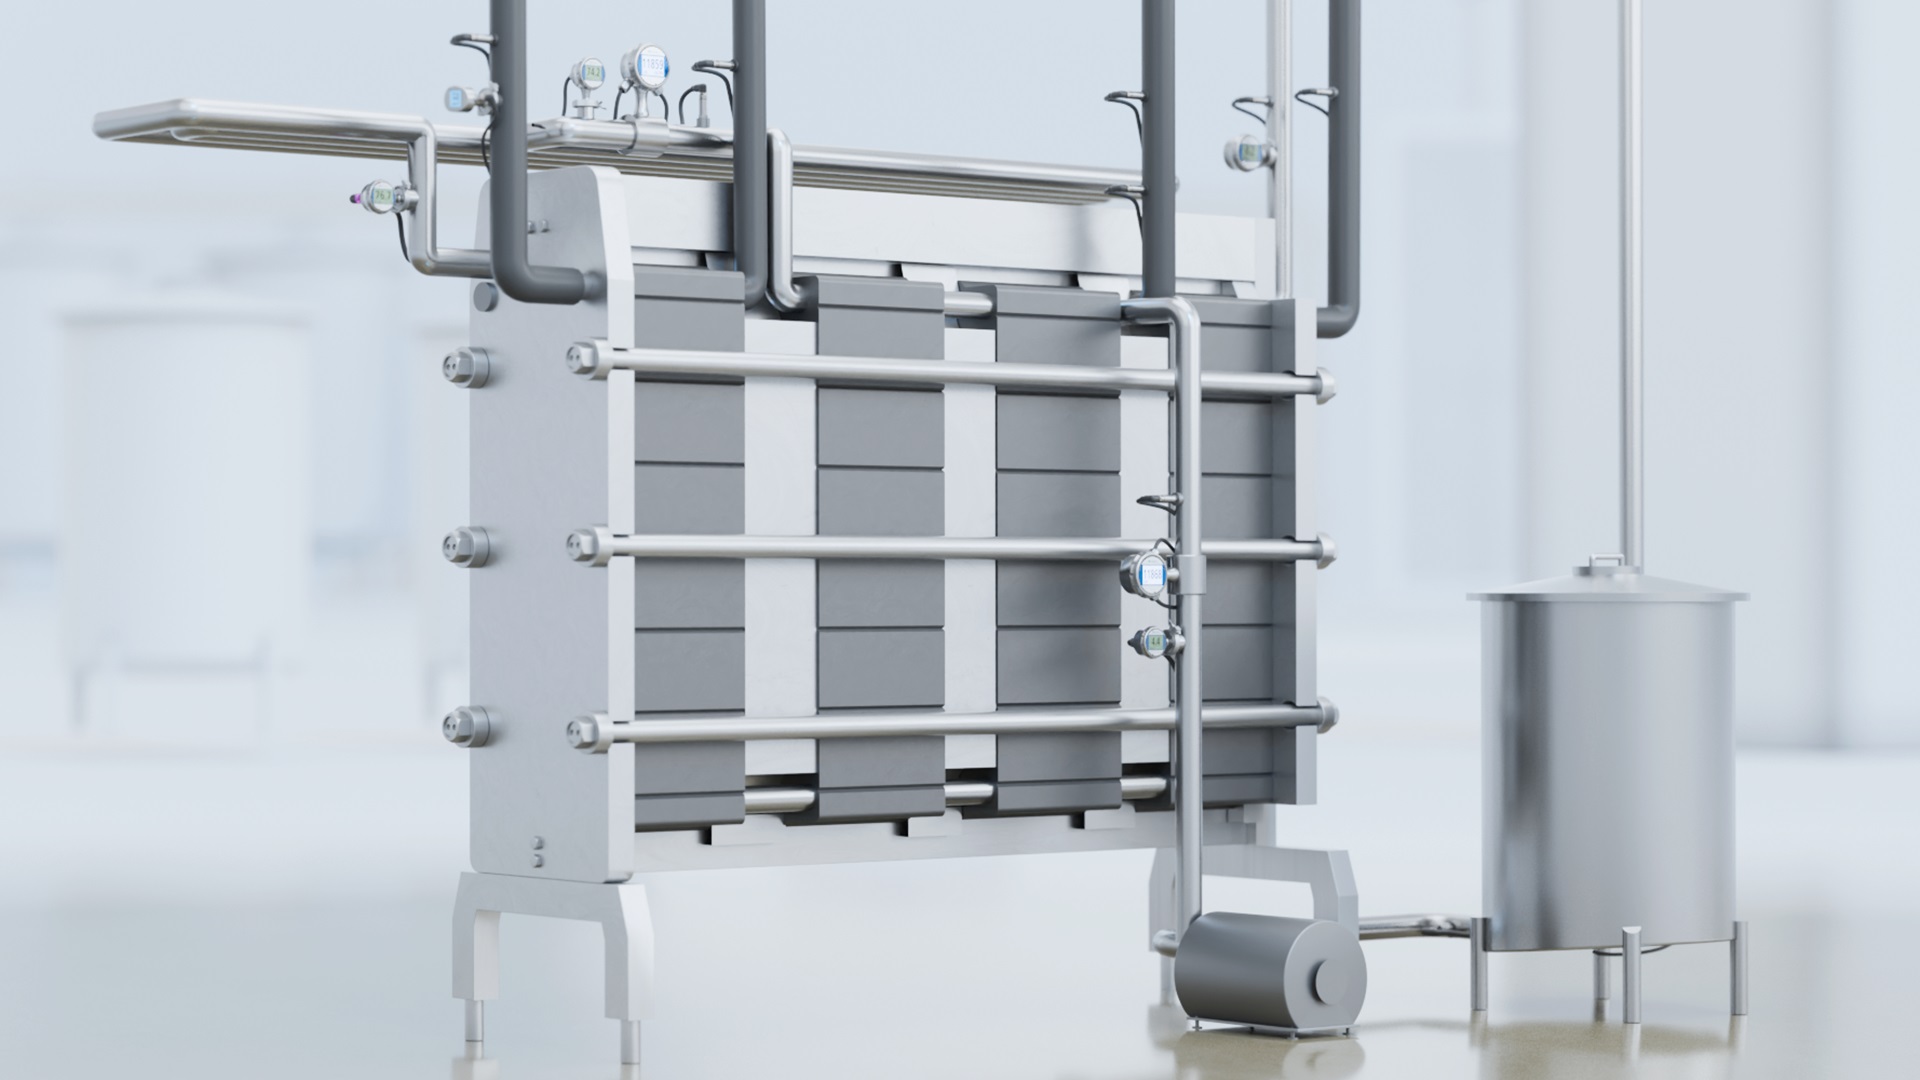
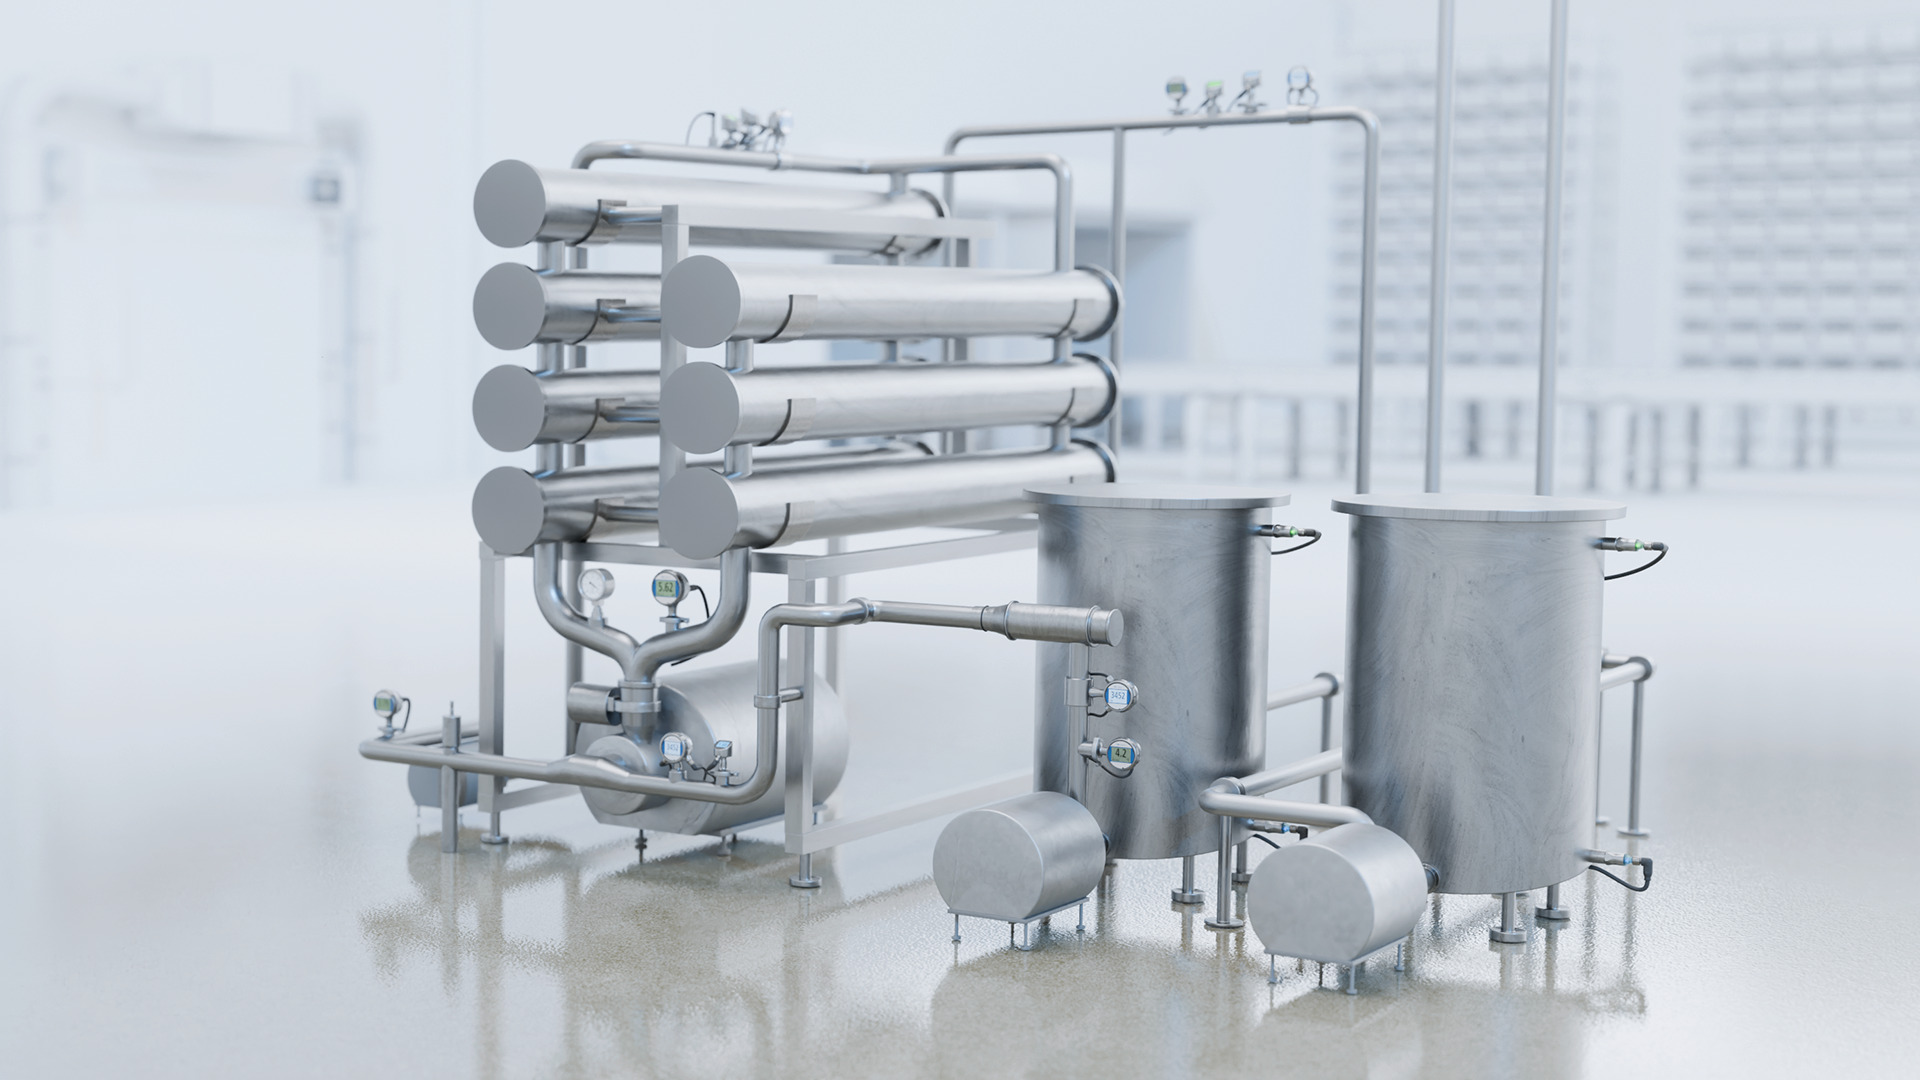
Heat Exchanger
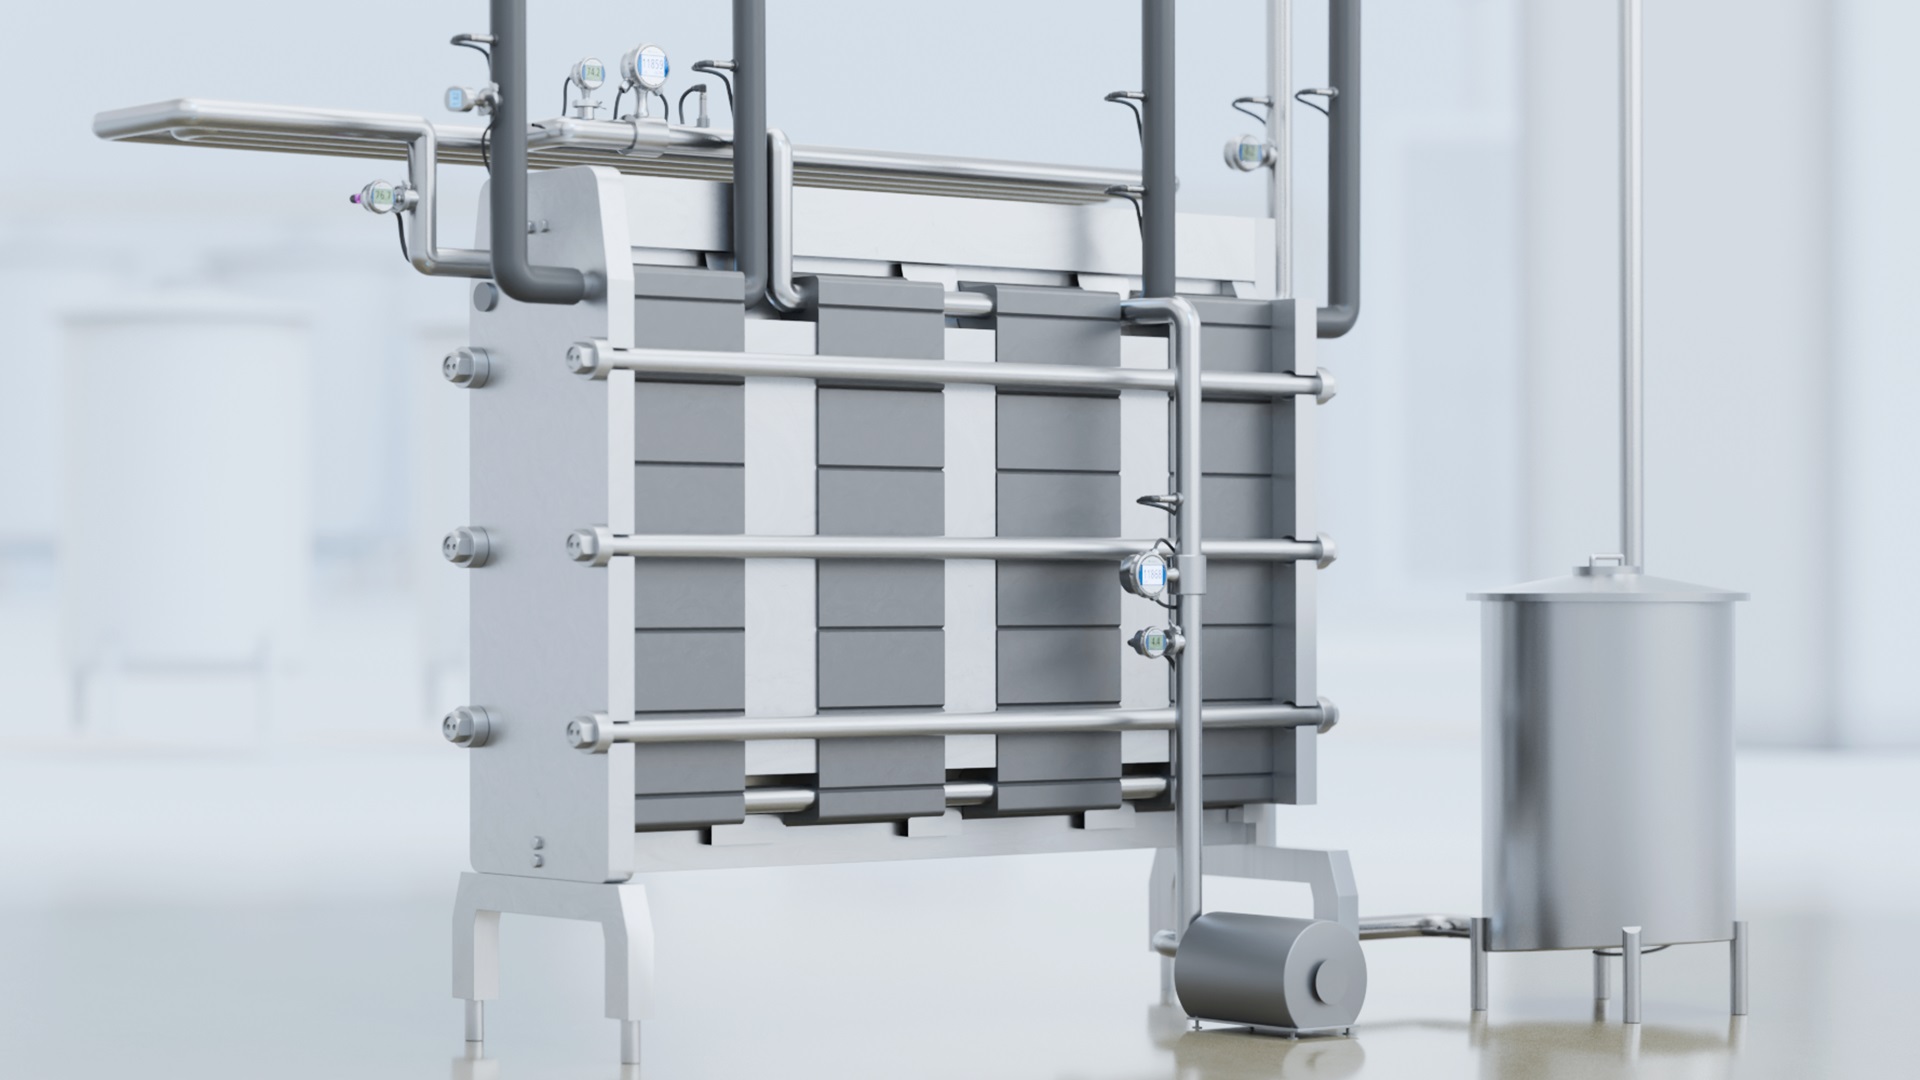
Fast, highly precise measurement of temperature, flow and pressure — unaffected by high process temperatures — enhances the reliability and efficiency of heat exchangers.
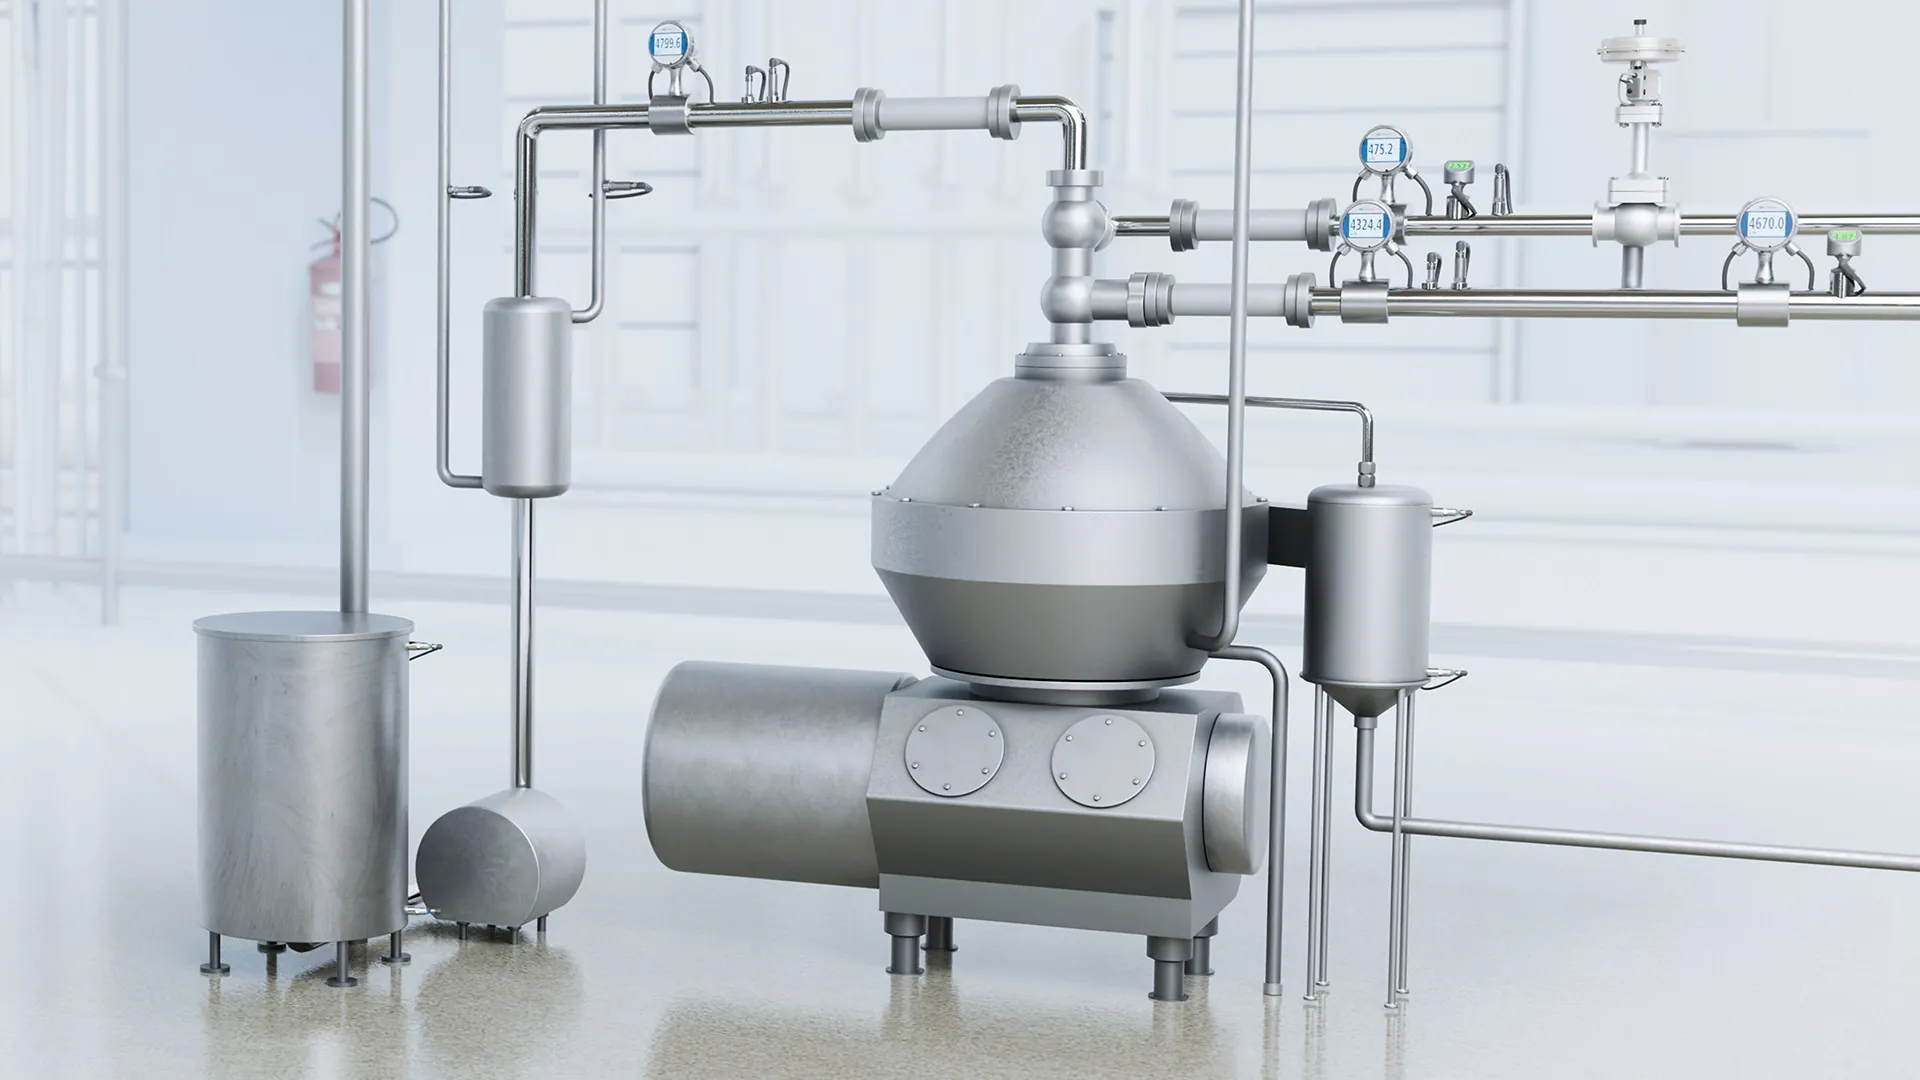
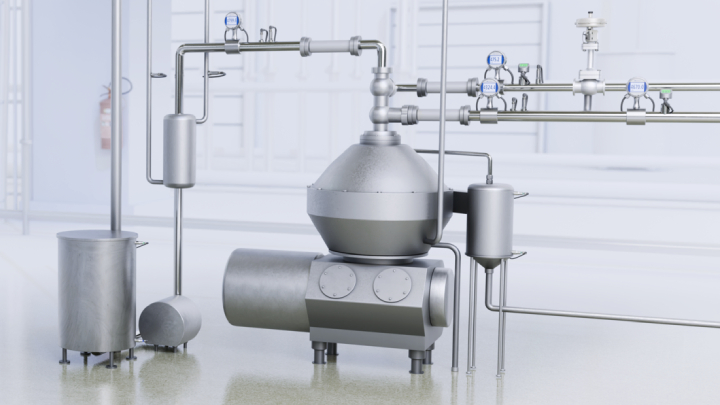
Centrifugation
Precise control of pressure and flow rate, reliable sludge discharge, and speed and vibration monitoring require efficient, consistent and safe operation.

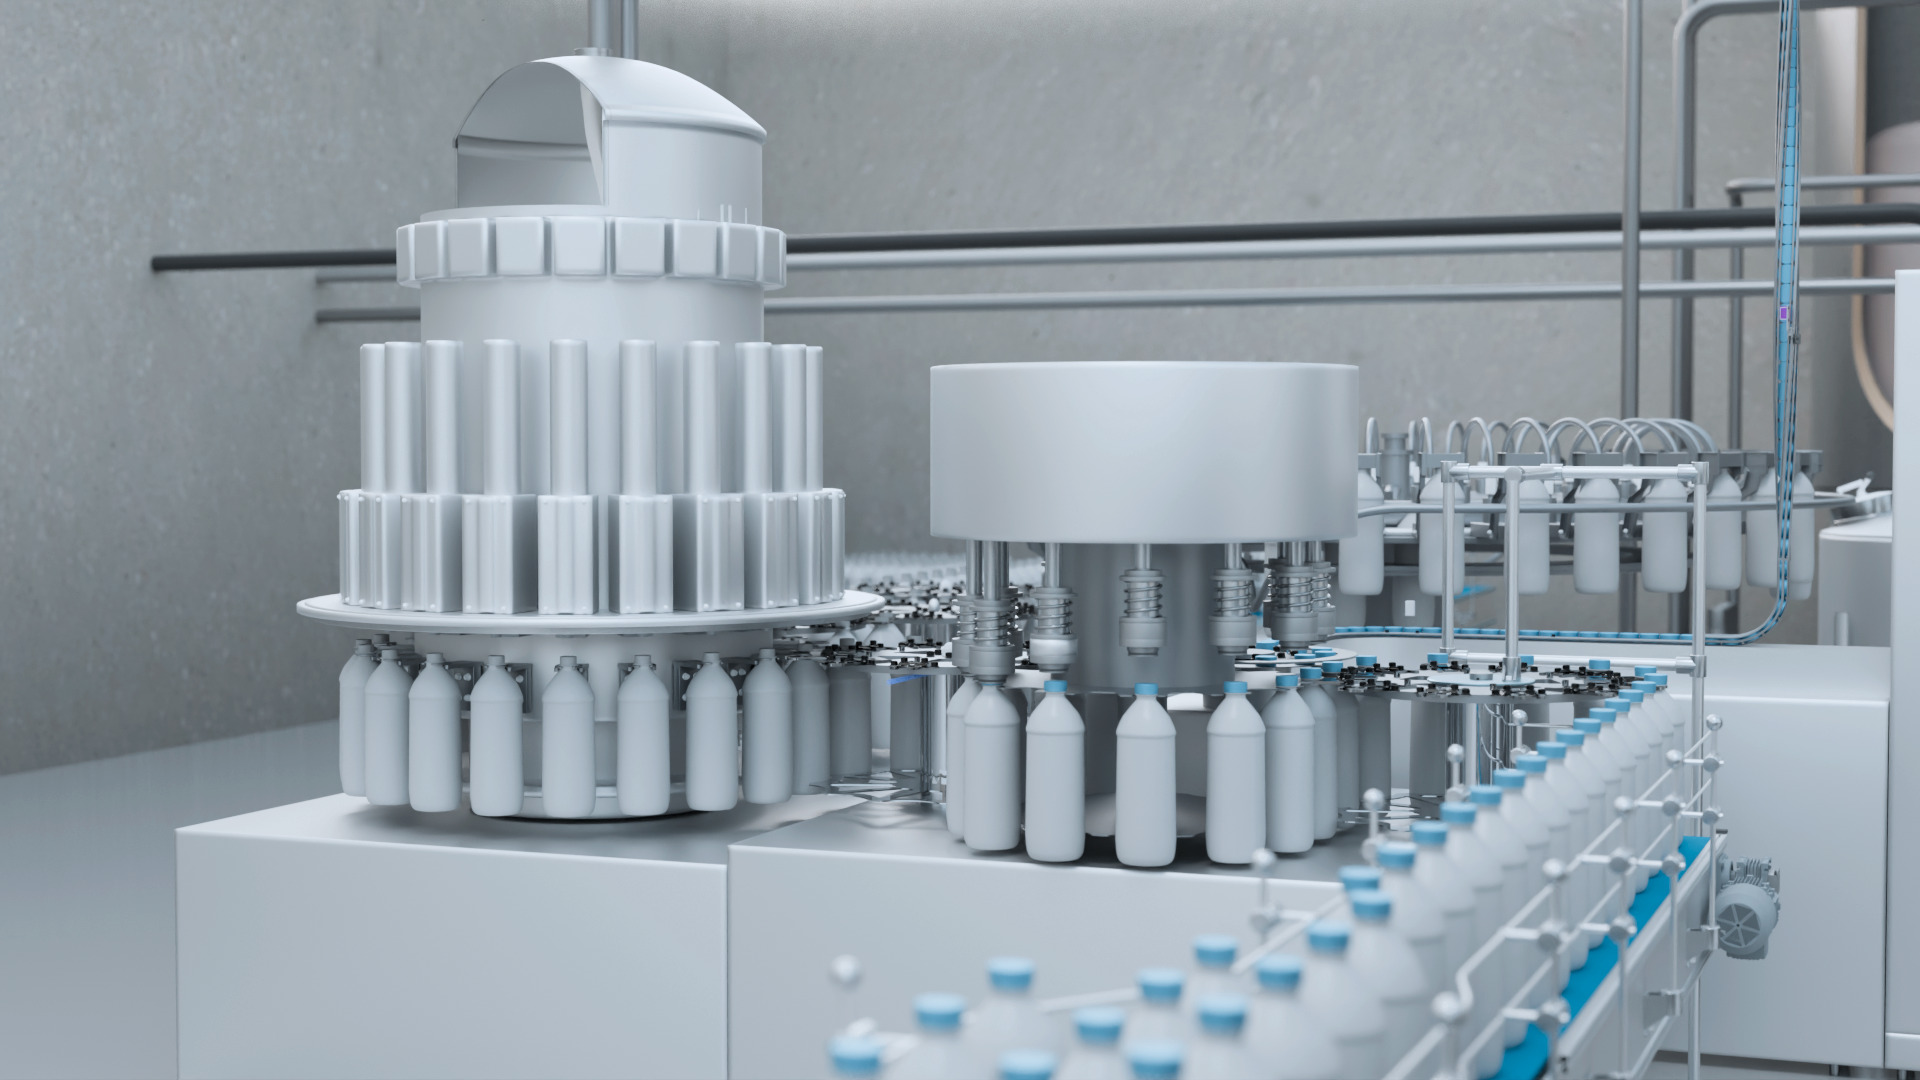
Filling and Packaging
Our wide portfolio of process, optical and smart vision sensors, along with encoder and camera systems, ensures maximum uptime and flexibility in filling and packaging.
Filtration
Efficient, cost-effective separation and maximum availability require tight control of pressure, flow and level.
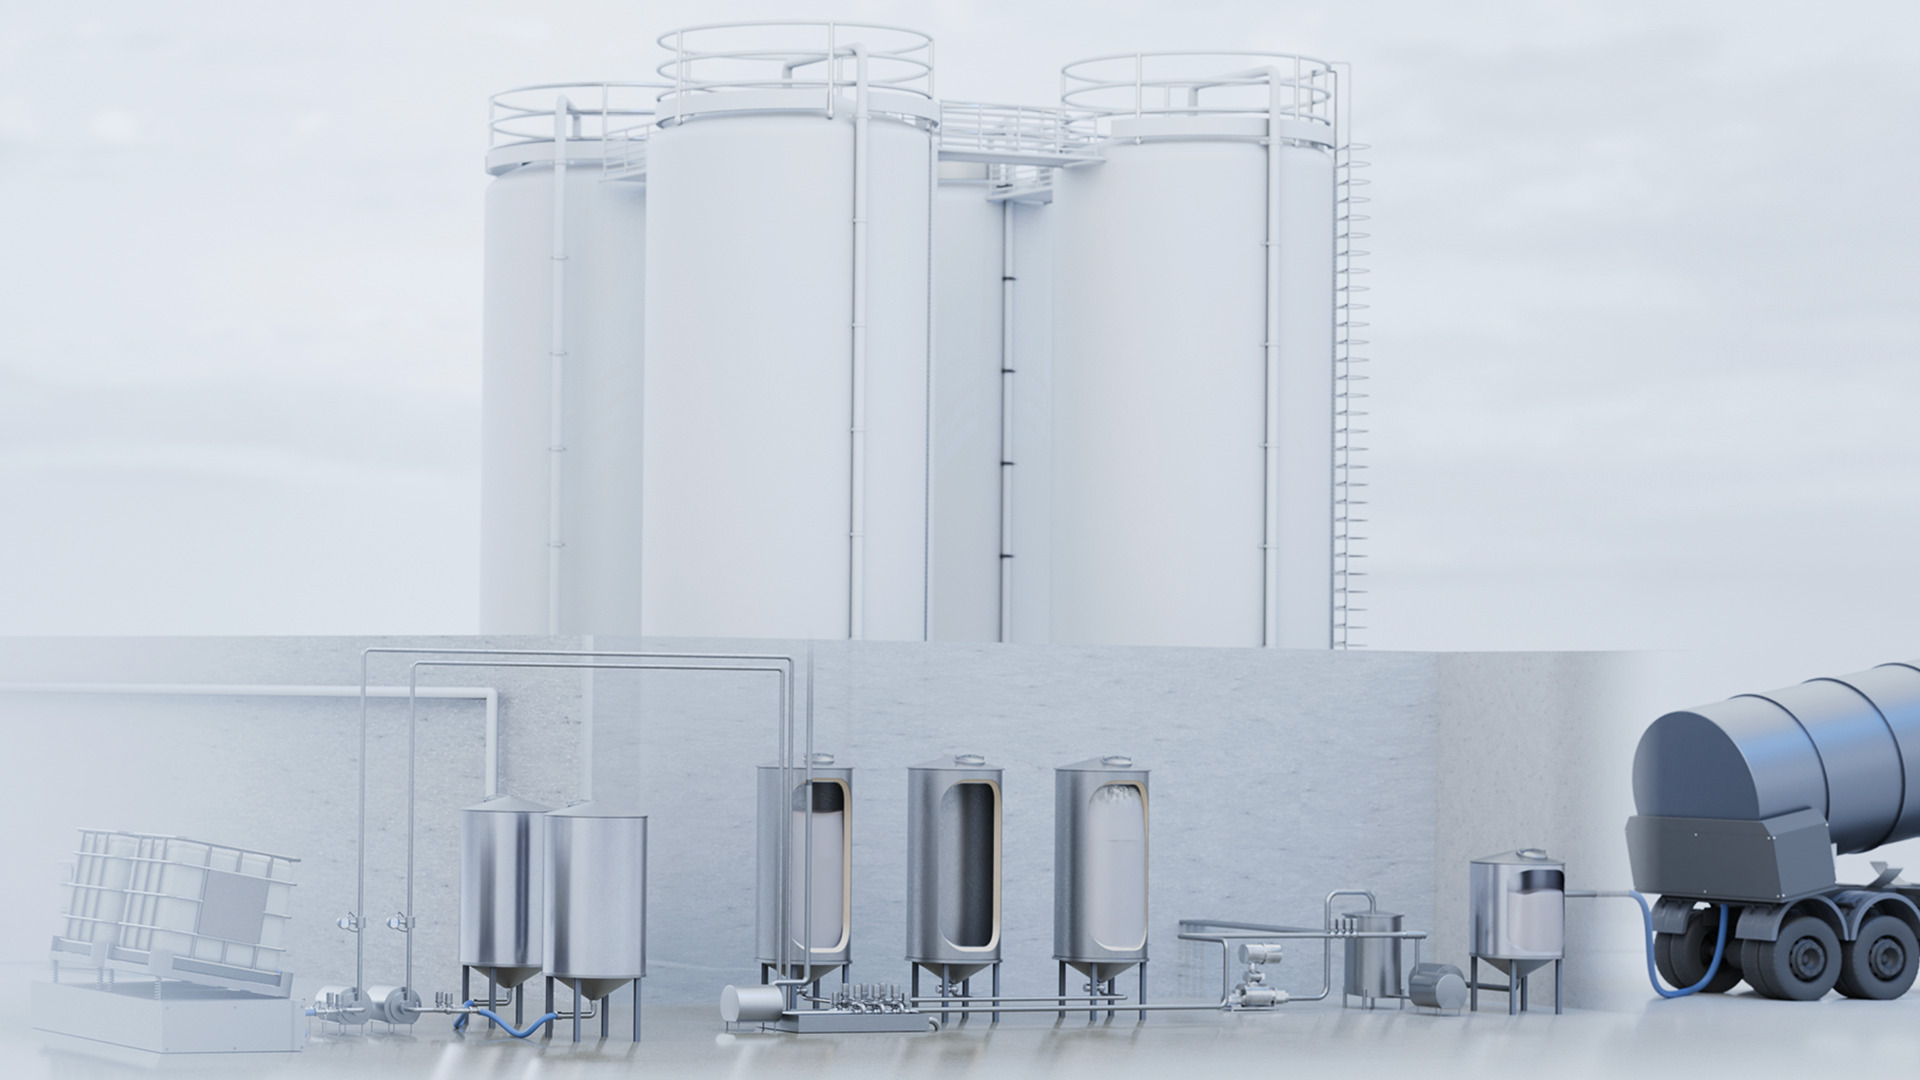
Liquid Inventory Management
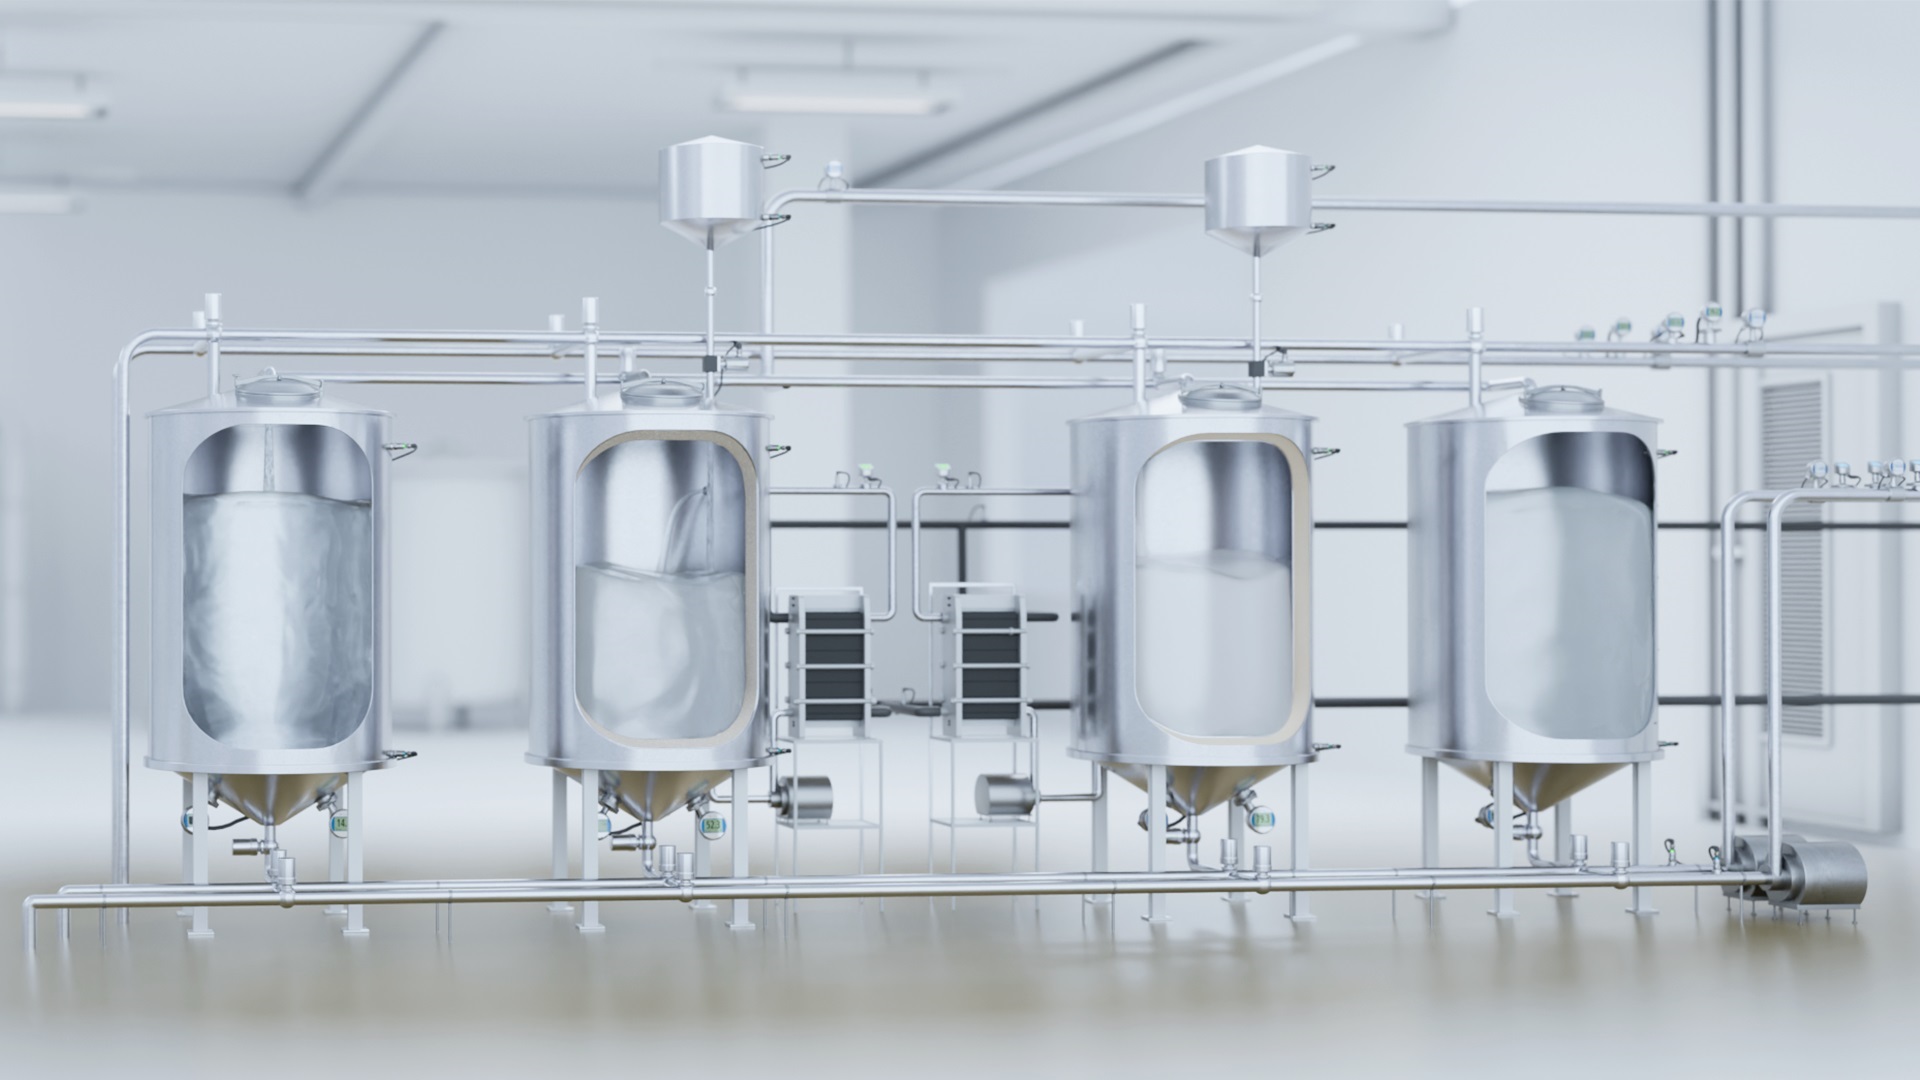
From the intake, processing and storage of milk and other raw materials, precise level, temperature and pressure measurement enables production planning based on actual material availability.
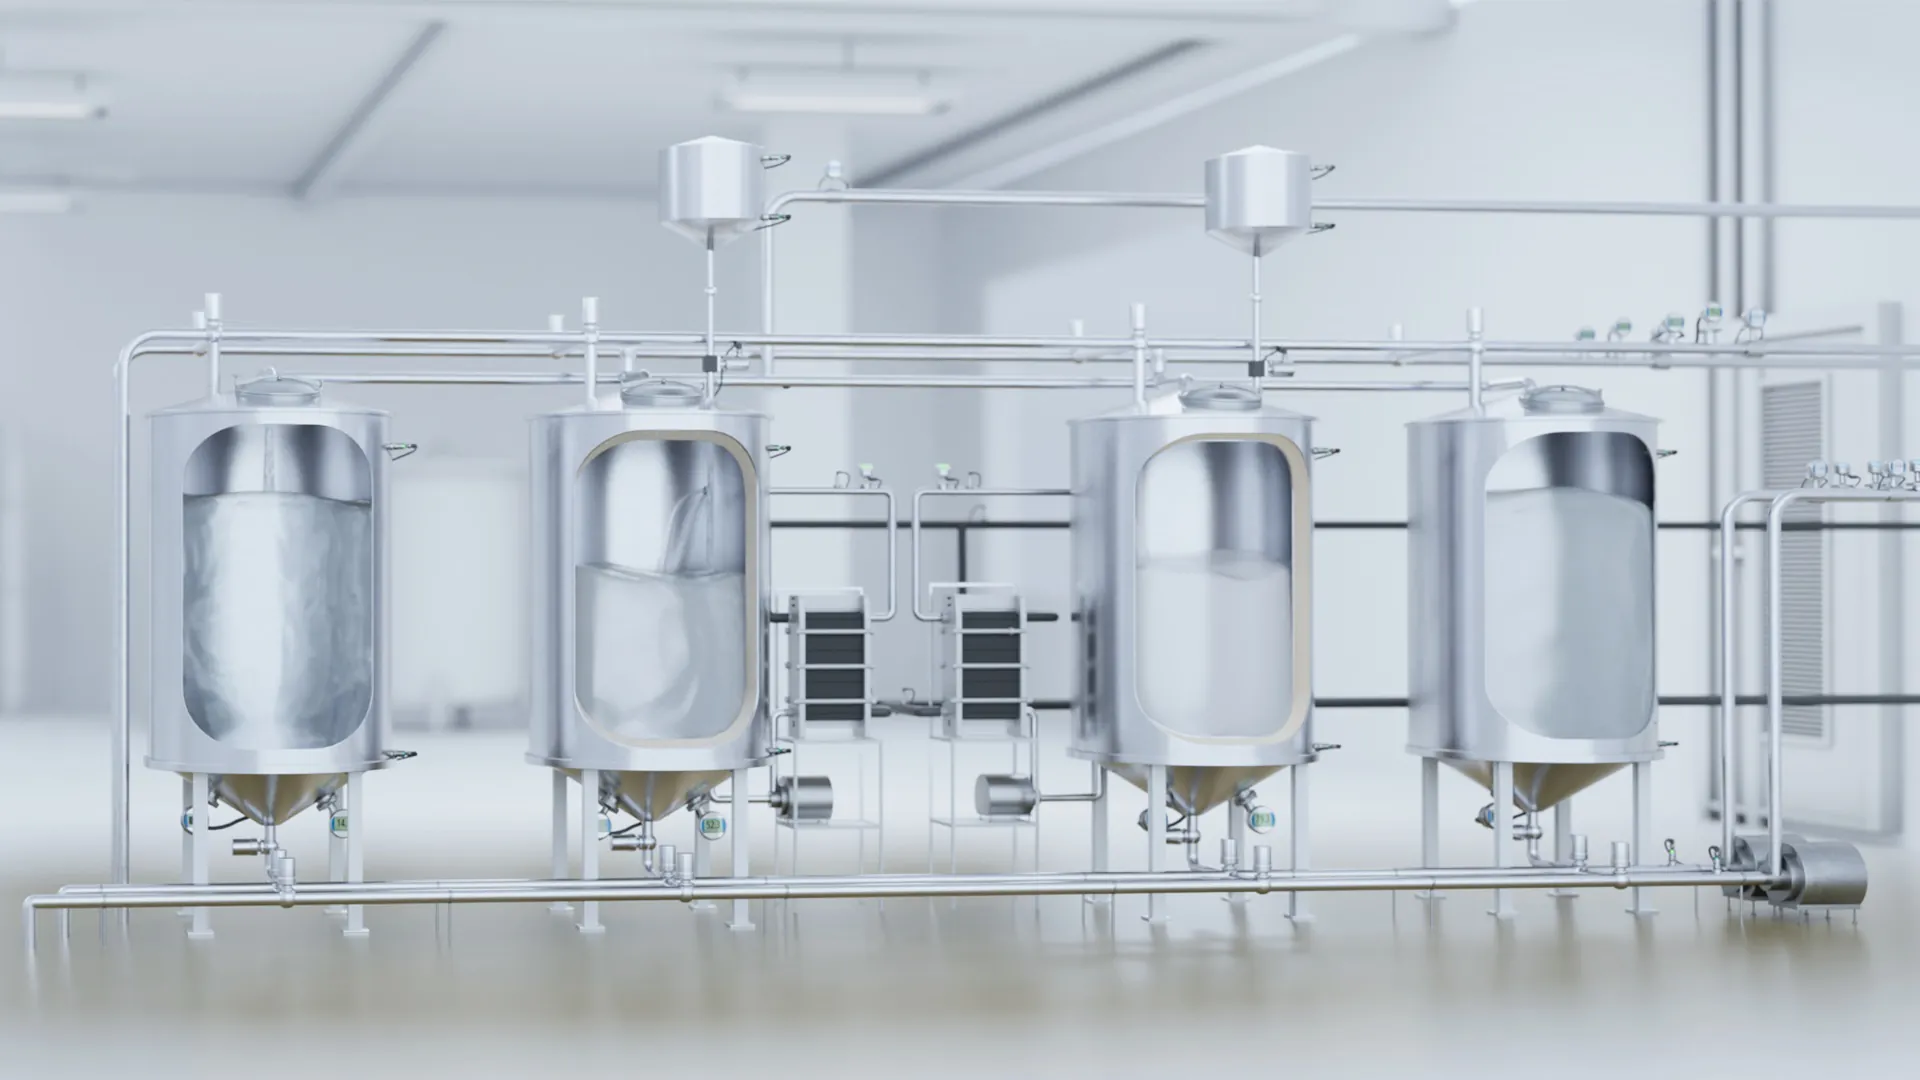
Clean-in-Place (CIP) Systems
Inline sensor solutions designed specifically for CIP monitor key parameters such as conductivity, temperature, flow and pressure, for maximum food safety and efficiency.
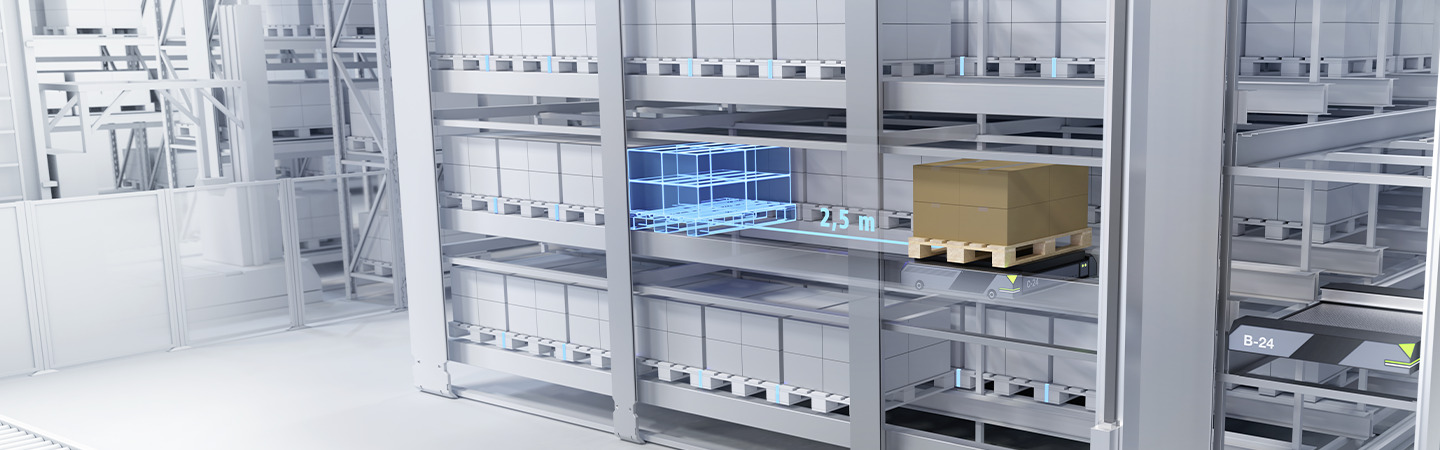
Intralogistics
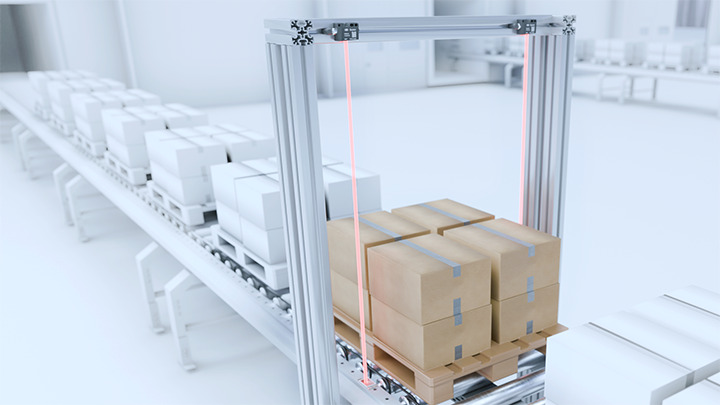
Position, distance and speed measurement combined with object detection and identification sensors ensures maximum efficiency in storage and distribution processes.
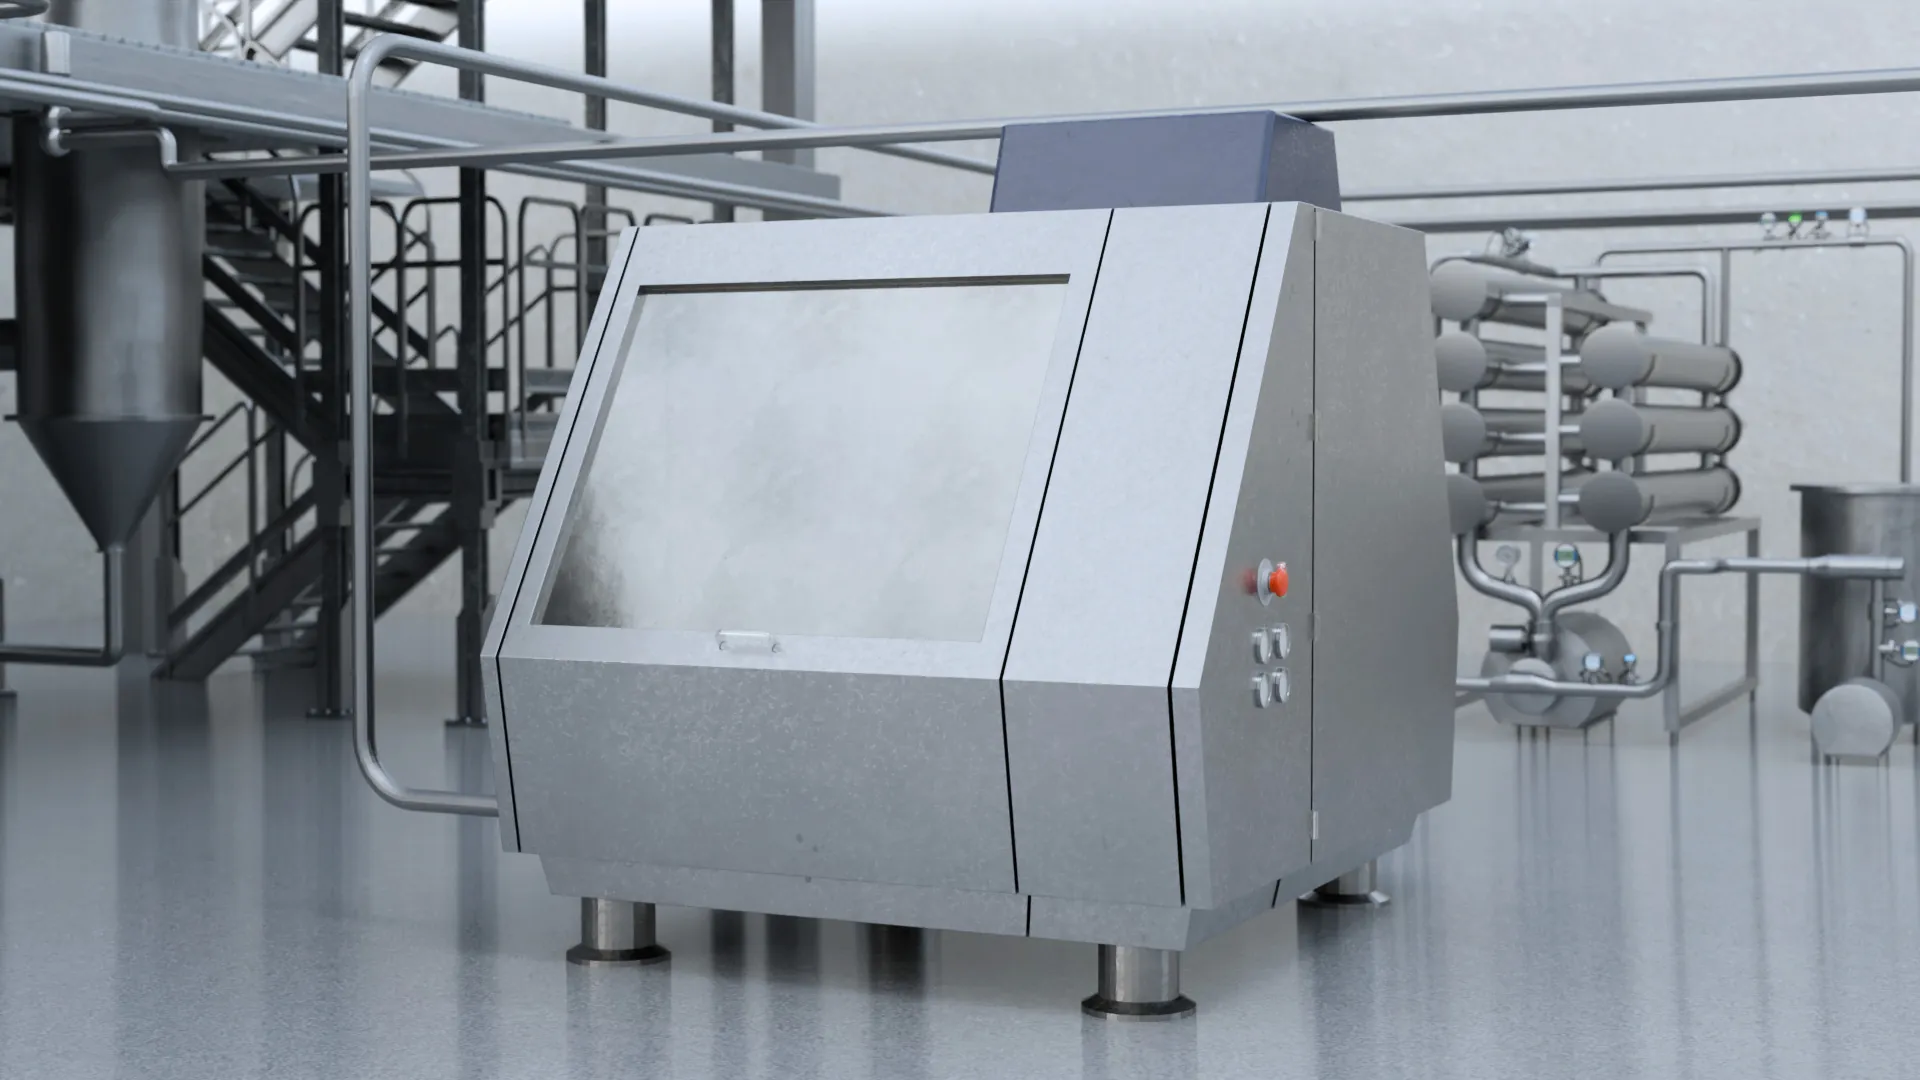
Homogenization
In dairy products, fat is stabilized by breaking down and evenly distributing droplets using a homogenizer. Stable operation requires tight control of pressure, flow and product temperature.
Baumer sensors are certified in compliance with all international design and material standards relevant to the food and beverage industry. Baumer's internal processes are certified in compliance with DIN ISO 9000 requirements. Hygienic sensors are designed, developed and manufactured in compliance with 3-A and EHEDG guidelines to guarantee the highest standards in food production.
End-to-end development, from the initial concept phase through to series production, is continuously validated through our customers' actual use. Sensor protection is a key element here. Our sensors comply with IP69 protection and undergo additional testing under our in-house proTect+ standard for maximum reliability and durability.
Learn more east
Sensor toolbox for the dairy industry
Have questions?
Our experts will be happy to answer any questions and provide further information. Just send us an email.
Get in TouchExplore our other sensor solutions for the food and beverage industry
Explore our sensor solutions for breweries, beverage production, extrusion, evaporation, heat exchangers, centrifugation, filtration and CIP cleaning systems.
Back to Food and Beverage SolutionsHave questions?
Our experts will be happy to answer any questions and provide further information. Just send us an email.